
WEBINAR: Allergen Management: Getting the Clean Right
The Allergen Management Series: Part Two
WEBINAR: Allergen Management: Getting the Clean Right
Tuesday 20th October, 13:00 - 14:00 BST
Join us for Part Two of our Allergen Management Series, hosted in partnership with Campden BRI.
In Part One, Closing the Gap, we looked at why allergen incidents remain a persistent problem despite significant industry investment, and where the gaps in allergen management most often lie. This session picks up where we left off, focusing on one of the most critical of those gaps: cleaning.
Unlike microbial risks, allergens can’t be killed, only removed, and an allergen clean is much more than a longer version of a standard clean. Yet many sites are being asked to manage more allergen changeovers, in shorter hygiene windows, with fewer experienced hygiene people to call on. Procedures that look robust on paper can quickly come under strain.
Our speakers bring together lab, audit and factory-floor perspectives: Wendy Duncan and Marie-Anne Clarke of Campden BRI, John Hessey of Hygiene Improvement Solutions, and Alex Carlyon of Klipspringer. Together, they’ll explore what an effective allergen clean involves, why so many fall short, and how to get it right using the time and resources you actually have.
Whether you work in hygiene, technical or production, you’ll leave with practical points to take back to site. The session closes with a live Q&A, giving you the chance to put the real-world challenges you face to our expert panel.


Webinar Speakers

Alex Carlyon
Key Account Director
Klipspringer

Wendy Duncan
Safety, Quality & Allergens Manager
Campden BRI

Marie-Anne Clarke
Allergens Team Manager
Campden BRI

John Hessey
Managing Director, Hygiene Improvement Solutions Ltd.
Wendy Duncan
With more than 25 years in food manufacturing, Wendy has built her career in the FMCG sector across the UK and Europe. She now leads on allergens within Campden BRI’s Food Safety Management Systems team, where her training and consultancy work helps clients get to grips with allergen risk and ensure compliance.
- Member of the FDF Allergen Steering Group
- Technical Committee of the Federation of Bakers (Safety and Allergen Support)
- Member of RSPH
- Associate IFST member
Marie-Anne Clarke
With over 20 years’ experience in analytical science, Marie leads the Allergen Testing and Biochemistry and Molecular Biology teams at Campden BRI. Through consultancy projects, she helps organisations strengthen quality assurance frameworks, optimise testing programmes and align with UK and international food safety requirements.
- Expertise in analytical testing, allergen risk management, molecular detection methods, species authenticity verification and GMO analysis
- Experienced in allergen cleaning validation and verification (for both allergen management and reusable containers)
- Designs and implements analytical testing strategies, validates laboratory methods and investigates contamination incidents
John Hessey
With over 30 years’ experience in the food industry, John has held operational, technical and hygiene management roles. He is Managing Director of Hygiene Improvement Solutions Limited, a company he founded in 2011, which provides hygiene consultancy, interim hygiene management, skilled hygiene labour and contract cleaning services.
- Qualified BRCGS Auditor
- Experience with companies supplying Marks & Spencer, Tesco, Sainsbury’s, Asda, Waitrose, Co-op, Boots and Morrisons
- Experienced chilled factory and bakery hygiene manager, specialising in lean management techniques, hygiene standards, audit compliance and solving microbiological problems
Key Webinar Areas

1. Making Allergen Cleaning Theory Work (Campden BRI)
This session focuses on the practical application of allergen cleaning: how to plan, carry out and prove a clean that works on your site, and where cleans commonly go wrong.

2. Why Allergen Cleans Fail on Site
(John Hessey)
Drawing on a career spanning hygiene management, contract cleaning and auditing, John looks at why allergen cleans fail on site and what it takes to get them right.

3. Allergen Cleaning in a Shrinking Hygiene Window (Alex Carlyon)
Hygiene windows are getting shorter, and experienced hygiene people are harder to find. Discover how sites can work within those pressures, rather than against them.

4. Live Q&A with the
expert panel
Whether your challenge is planning, carrying out or proving a clean, this is your chance to put it to our expert panel and take practical answers back to site.
Register to Attend
If you joined us for Part 1 of the Webinar Series, you are already signed up for Parts 2 and 3, so there’s nothing more you need to do.

6 Benefits of In-Process Optical Monitoring in Food Manufacturing
Discover 6 Benefits of In-Process Optical Monitoring for Your Food Production Site
From identifying the root cause of problems to supporting cleaning, maintenance and audit preparation, In-Process Optical Monitoring gives food manufacturers a clear view of what is happening inside their equipment during production.
Here are 6 benefits of In-Process Optical Monitoring to consider if you are thinking about introducing this solution to your site.
What Is the In-Process Optical Monitoring System?

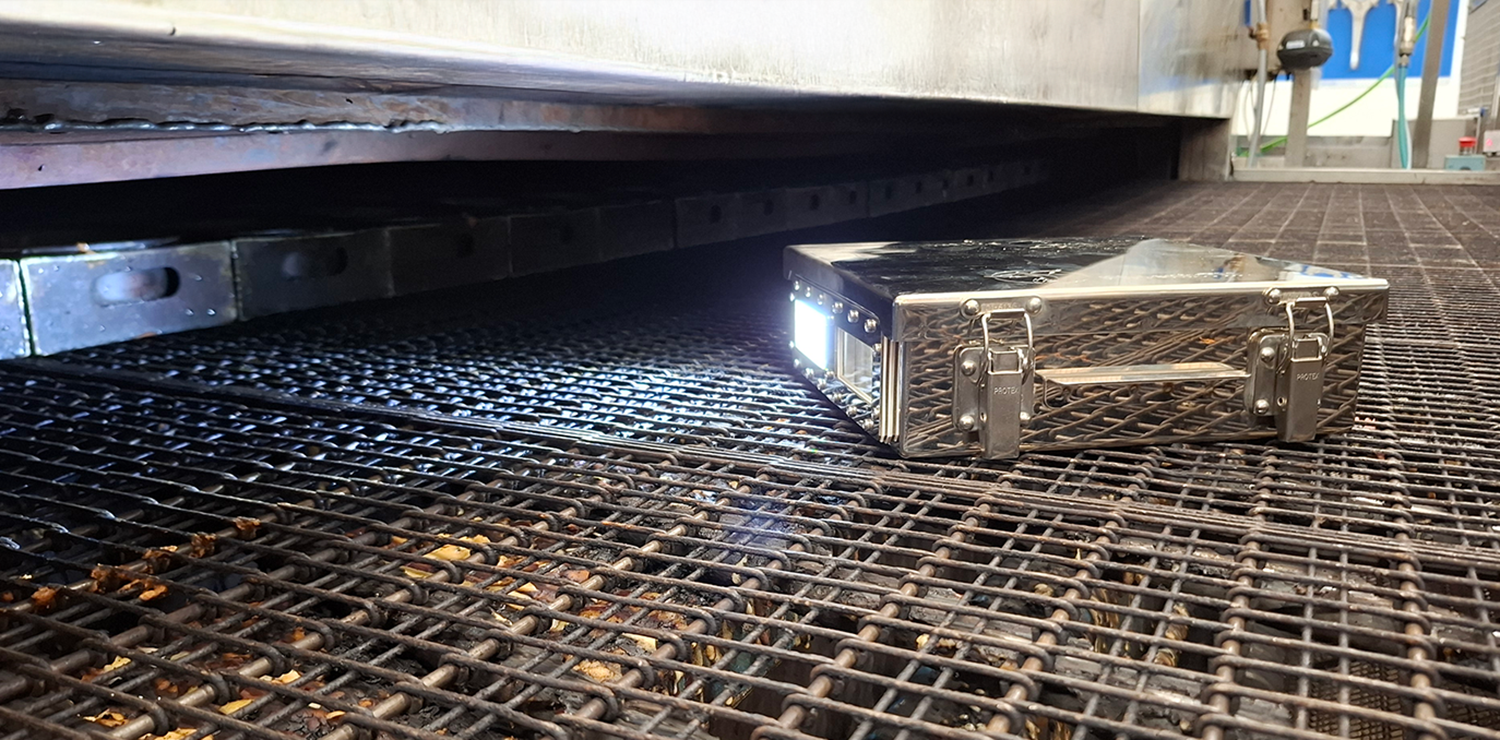
The In-Process Optical Monitoring System travels through your production process under normal operating conditions, capturing high-definition footage of what is happening inside your equipment. It gives your team a clear view of the process without the need for downtime or equipment dismantling, providing valuable visual information alongside your existing data.
Key Features
Travels with the product
Travels through the full process under normal production conditions, capturing what happens as the product moves through each stage.
4K high-definition video
Records continuous footage which can be reviewed after each run to investigate equipment condition and process performance.
Built-in illumination
A high-temperature torch provides up to 1,000 lumens, with adjustable intensity and beam width for clear footage, even inside unlit ovens.
Forward or reverse-facing
The system can be configured to face forwards or backwards, providing visibility of different areas within your equipment.
Withstands temperatures up to 300°C / 572°F
Designed for high-temperature environments, with a max operating temperature of 300°C and a thermal duration of up to one hour at 250°C.
Constructed from 316 stainless steel with an IP65-rated enclosure
A durable solution designed to withstand moisture and demanding food factory environments.
1. Find the Root Cause of Problems
An In-Process Data Logger can be a useful tool for identifying when something isn’t quite right. It might show that a zone is running cold, a result is inconsistent, or a reading has started to drift. However, while this data can tell you what is happening, it doesn’t always tell you why.

This is where optical monitoring can provide valuable additional insight. By capturing what is happening within the process, it allows you to see the physical conditions behind the data and identify potential causes more quickly.
Your team can use the footage to understand what is happening, investigate the root cause, and take appropriate action with greater confidence.
2. Reduce Foreign-Body and Contamination Risk
Over time, equipment can develop issues that aren’t always immediately visible. Damaged insulation, loose debris, and the build-up of condensation can all create potential risks within the production environment.
If material breaks away and enters the product, it can become a foreign-body hazard. The consequences can include contaminated batches, costly recalls, production downtime and, most importantly, a potential risk to consumer safety.

Optical monitoring provides an additional layer of protection by giving your team greater visibility of what is happening within the process. By helping to identify developing issues, it can give you the opportunity to investigate and take action before they become a more serious food safety incident.
3. Create Visual Evidence of Equipment Condition for Audits
During an audit, it’s important to be able to demonstrate that potential risks are being actively monitored and managed across your site, rather than simply relying on written records.
Optical monitoring can provide a dated, reviewable record of what is happening inside your equipment during each run. This gives your team visual evidence that can complement documented inspections and help to demonstrate that any issues identified have been followed up.

It can also be useful when carrying out repairs. By comparing footage from before and after an intervention, you can clearly see what has changed and provide an audit-ready record of the work carried out.
4. Catch Maintenance Issues Early
Unplanned stoppages are expensive, and many can start with small equipment faults that go unnoticed. Optical monitoring provides visibility of the condition of internal components, this includes damage to chambers, insulation, and individual parts.
Regular checks give maintenance teams a clearer picture of equipment condition and make it easier to keep track of developing faults.

Instead of waiting for a component to fail and dealing with an unexpected breakdown, maintenance can be planned around production schedules and existing maintenance activity.
5. Plan Cleaning from Evidence, Not Guesswork
Fixed cleaning schedules don’t always reflect what is actually happening inside your equipment. Some areas may need cleaning sooner than expected, while others may require less frequent attention.
Optical monitoring shows where build-up is occurring, giving your team a clearer basis for deciding when and where cleaning is needed. This can help ensure cleaning activity is focused on the areas that actually require attention, rather than relying solely on a fixed schedule.

The footage can also provide a useful record after cleaning, allowing your team to compare the condition of the equipment and assess the result.
Just as importantly, these inspections can be carried out without stopping production or dismantling equipment. Internal checks can become a routine part of the cleaning process, rather than something reserved for scheduled shutdowns.
6. Understand Product Behaviour
Optical monitoring doesn’t just provide a view of the equipment itself. It can also show how your product behaves as it moves through the process.
This includes changes in colour, shape and size, as well as differences in bake uniformity from one zone to another. Seeing these changes as they happen can give your team a clearer understanding of how process conditions are affecting the finished product.

The footage could also be used to show how a conveyor belt is moving and if product transfer issues occur. This provides a visual reference for investigating problems that may otherwise be difficult to pinpoint from process data alone.
Part of a Complete Process Monitoring Solution
The Multi-Channel In-Process Data Logger gives you detailed temperature data from throughout your production process, helping you understand how your equipment is performing and identify potential hot or cold spots. With up to 20 thermocouples, it can be used for temperature profiling, HACCP cook validation, and investigating process inconsistencies.

When used alongside the In-Process Optical Monitoring System, you can take this a step further. While the data logger shows you what is happening with temperature, the optical system can help show you what is happening inside the equipment at the same time.
Together, they provide a more complete picture of your process, helping your team investigate problems, validate performance, and make informed decisions based on both data and visual evidence.
So there you have it, 6 benefits of using an In-Process Optical Monitoring System at your food production site.
If you have any questions about the system or how it could support you and your team, contact us on 01473 378 517 or email sales@klipspringer.com. Alternatively, fill out the form below.
If you would like to learn more about the In-Process Optical Monitoring System, share your details below and a member of our team will be in touch.

Webinar Round Up: Allergen Management: Closing the Gap
Insights from our Industry Webinar on Strengthening Allergen Management in Food Manufacturing.
In this article, we recap key insights from the first webinar in our three-part series with Campden BRI, exploring why allergen management systems can still fail despite the procedures, training, checks, and controls already in place. The session featured key insights from:
- Alec Kyriakides, Independent Food Safety Consultant.
- Wendy Duncan, Safety, Quality and Allergens Manager, Campden BRI.
- Alex Carlyon, Key Account Director, Klipspringer
If you are short on time, you will find a bulleted list of key takeaways at the end of each section.
Legal Obligations
Alec opened the webinar with a closer look at the legal requirements that apply to UK food and drink manufacturers, which include:
- Assimilated Regulation (EU) No. 1169/2011 (for England and Wales)
- Regulation (EU) No. 1169/2011 (for Northern Ireland)
- Plus, enforcement regulations (Food Information Regulations 2014) and subsequent amendments, e.g. FIR 2019 (Natasha’s Law)
In terms of the specific areas of food production, Alec outlined the following requirements:
- Prepacked food is expected to carry a full ingredient list, with any of the 14 allergens emphasised within it
- Prepacked food for direct sale (PPDS) is also expected to carry a full ingredient list, with any of the 14 allergens emphasised within it. This category also relates to Natasha’s Law
- Non-prepacked food requires a declaration of any allergens used as ingredients, which can be provided in electronic, written or oral form
- Distance selling (e.g. e-commerce) requires allergens to be declared before purchase and again when the food is delivered
Precautionary Allergen Labelling
Precautionary allergen labelling (PAL) is not mandatory. However, failing to provide it where there is a genuine risk may expose consumers to undue risk and the product could be deemed unsafe.
It is essential that PAL does not mislead or confuse the consumer, and a big part of this is keeping it separate from the ingredients list. PAL can be used alongside “vegan” and “gluten-free” claims, but not alongside other “free-from” claims.
What’s Coming Next?
- Benedict’s Law now applies to state schools, which are required to conduct training and hold adrenaline auto-injectors, among other measures
- Owen’s Law is particularly focused on making allergen information mandatory in hospitality environments. It is supported by the FSA and is recommended guidance, but is not yet law
- Codex has recently published allergen thresholds that are being used to support risk-assessed precautionary allergen labelling (PAL)
Key Takeaways
- Prepacked and PPDS foods must carry full ingredient lists with allergens emphasised
- Non-prepacked and online sales have their own allergen declaration rules
- Precautionary allergen labelling isn’t mandatory, but omitting it where a real risk exists could make a product unsafe
- PAL must be kept separate from the ingredients list and used alongside claims with care
- Benedict’s Law, Owen’s Law and new Codex thresholds signal further change ahead
What Do Allergen Recalls Tell Us?
Looking at recall data can provide a useful starting point for understanding where allergen management is going wrong. Alec compared 2025 recall data from Australia, the UK and the USA. Despite the differences between these countries, the patterns were remarkably similar.
Milk was the most common allergen driving recalls, while multi-component products were among the most common food groups involved. There are several reasons why these products can be challenging to manage. Multiple ingredients make labelling more complex, while the same complexity can create additional challenges within the factory.
But recall data only tells us where something has gone wrong. It does not necessarily tell us why. Looking at UK Food Standards Agency allergen recalls from January to August, Alec highlighted several common causes:
- 43% involved an allergen that was not listed in the ingredients list
- Around a third involved mis-packs, where the wrong product or packaging reached the line
- 10% involved cross-contamination
- 10% involved an allergen being listed but not emphasised correctly
The figures provide a useful sense check for manufacturers. If these are the types of issues leading to recalls across the industry, could the same weaknesses exist within your own site?
What About Audit Non-Conformities?
Recall data is only one part of the picture. Audit non-conformities can provide another useful source of information. In hospitality and catering, allergen-related non-conformities commonly involve missing or inaccurate allergen information, or customers not being clearly signposted to where they can find it. Allergen contamination control accounts for much of the remaining issues.
BRCGS data from food manufacturing shows a slightly different picture. Cross-contamination management is a major driver of non-conformities, with weaknesses in procedures and risk assessments accounting for a significant proportion. On-pack labelling makes up much of the remainder. The important point is that these findings should not simply be viewed as audit statistics. They can be used as a prompt to ask: could the same weaknesses exist in our business?
Key Takeaways
- Undeclared allergens and mis-packs are common causes of recalls
- Labelling verification remains a significant area of risk
- Cross-contamination continues to be a major challenge
- Audit findings can highlight areas worth challenging within your own systems
- Recall and audit data show symptoms, but not necessarily the root cause
Finding the Root Cause
An allergen incident rarely starts with the final mistake that is visible to the consumer. Alec highlighted the importance of analysing why these incidents happen, rather than only what went wrong at the point of failure.
Drawing on the FSA’s 2025 incident prevention report, Alec looked at the key drivers behind the majority of recalls, as explored through root cause analysis. The most common specific issues within the main categories were:
- Process: labelling verification checks (30%)
- Material: ingredient cross-contamination (11%)
- Material: ingredient specification (8%)
- Method: labelling declaration (14%)
Key Takeaways
- Allergen incidents rarely start with the final, visible mistake
- Understanding why incidents happen matters more than what went wrong at the point of failure
- Root cause analysis from the FSA’s 2025 incident prevention report reveals the key drivers behind most recalls
The Swiss Cheese Model: Why Controls Fail
Wendy introduced James Reason’s Swiss cheese model as a useful way of thinking about allergen management. The model illustrates how food safety incidents rarely result from an isolated mistake.
Businesses have multiple controls and barriers in place, including supplier approval, segregation, cleaning, label verification and product release. Each of these controls can help to prevent an allergen from reaching the consumer. However, an incident can occur when weaknesses or failures align across several of these barriers, allowing the issue to pass through the system.
This is why focusing solely on the final error can miss the bigger picture. The objective is not simply to identify the last failed check, but to understand why the earlier controls did not work effectively.
Key Takeaways
- James Reason’s Swiss cheese model shows that food safety incidents rarely stem from a single mistake
- Incidents occur when weaknesses across several controls align
- Focusing only on the final error can miss the bigger picture
- The goal is to understand why earlier controls failed, not just identify the last failed check
Prevent, Eliminate or Reduce?
Businesses need to be very clear about the purpose of the allergen controls they have in place and the outcomes they are intended to achieve. Are you trying to prevent the hazard from being introduced, eliminate the hazard, or reduce the risk to an acceptable level? The intended outcome should then determine how the control is designed, validated, monitored and verified.
Examples of allergen controls include:
- Supplier controls
- Segregation
- Formulation controls
- Production controls
- Packaging and labelling controls
- Physical separation
- Controlled handling
- Production sequencing
- Cleaning
Cleaning is an important example. Completing a cleaning procedure does not automatically mean that all allergenic material has been removed. Its effectiveness will depend on a range of factors, including the allergen, the product, the equipment and the cleaning method used. As Wendy highlighted, cleaning will be explored in more detail in Part 2 of the series.
Key Takeaways
- Businesses need to be clear on whether each allergen control aims to prevent, eliminate or reduce the hazard
- The intended outcome should shape how a control is designed, validated, monitored and verified
- Allergen controls span the whole operation, from supplier and formulation controls to segregation, production sequencing and labelling
Where Are Your System Vulnerabilities?
One of the biggest areas of vulnerability in allergen management can be at changeover points. Think about the handovers between:
- Supplier and manufacturer
- Procurement and technical
- Warehouse and production
- Hygiene and production
Each department may understand its own responsibilities, but weaknesses can arise when one team assumes that another has obtained, checked or communicated important information.
A supplier substitution may look like a routine commercial decision, but is the allergen profile the same, and is there a process in place to manage the change? Even a small formulation change may appear insignificant, but what impact does it have on specifications, labelling, scheduling, rework and cleaning?
Another example is when teams assume that completing a cleaning process means that a line is ready to run. But has it been inspected and verified? The challenge is to identify the points where critical information could be lost, delayed or misunderstood.
Key Takeaways
- Changeover points between teams and organisations are among the biggest allergen vulnerabilities
- Weaknesses arise when one team assumes another has obtained, checked or communicated key information
- Businesses should identify where critical information could be lost, delayed or misunderstood
The Procedure Trap
A procedure is evidence that a business has described what should happen; it is not evidence that what is written actually happens. A stronger assessment asks:
- Is the procedure technically appropriate?
- Does it reflect the real process?
- Do people understand it?
- Is it consistently applied?
- Can it withstand operational pressure?
- Does it achieve its intended outcome?
- Is there evidence that it remains effective?
The same applies to training. A training record confirms that someone attended training, but it does not necessarily demonstrate that they can apply the process correctly, recognise a problem or make the right decision when something goes wrong.
Key Takeaways
- A written procedure shows what should happen, not what actually happens
- Procedures should be tested against the real process, operational pressure and their intended outcome
- Ongoing evidence is needed to show a procedure remains effective
5 Warning Signs To Look Out For
Wendy highlighted several warning signs that could indicate weaknesses in an allergen management system.
1. Generic Risk
Assessments
Does your allergen risk assessment reflect your site’s actual allergen hazards and practices?
2. Allergens Are Seen as One Department’s Job
Effective controls depend on business-wide ownership, not just one department.
3. Training Without
Competence
Attending training is not the same as demonstrating competence.
4. Near Misses Are Corrected but Not Investigated
Near misses need to be investigated, not just corrected without further thought.
5. Controls Are Built for the Audit
Allergen controls need to work every day, not just when an auditor is expected.
Key Takeaways
- Allergen risk assessments should reflect your site’s actual hazards and practices, not generic templates
- Effective allergen management needs business-wide ownership, not just one department
- Attending training isn’t the same as demonstrating competence
- Near misses should be investigated, not just corrected
- Controls must work every day, not just when an auditor is due
Food Safety Culture
An effective food safety culture is vital across the business, and a key part of this is building robust controls around hazards.
As mentioned throughout the webinar, an incident rarely occurs due to one isolated failure. Going back to the root cause and understanding the failure pathway can reveal a series of weaknesses across multiple teams that have ultimately allowed the incident to occur. This highlights that allergen control is a company-wide responsibility and should never be left to one department.
Building this culture requires a clear sense of ownership. People need to understand their roles and responsibilities, and these should be clearly assigned rather than assumed. Every department has a role to play, from procurement and product development through to production and warehousing.
Senior leadership also has an important role in ensuring people have sufficient time and resources to maintain robust allergen controls.
Key Takeaways
- A strong food safety culture depends on robust controls around hazards
- Tracing the failure pathway often reveals weaknesses across multiple teams
- Allergen control is a company-wide responsibility, not one department’s job
- Roles and responsibilities should be clearly assigned rather than assumed
- Senior leadership must give people the time and resources to maintain robust controls
Moving From Confidence to Evidence & Procedures to Control
One of the strongest messages from the webinar was simple: Confidence isn’t evidence. A business can be confident that its allergen controls are working, but that confidence needs to be supported by evidence. Wendy outlined five important stages:
- Validate: Can the control achieve its intended outcome?
- Monitor: Is the control continuing to operate within its defined criteria?
- Correct: How do we regain control if it has been lost?
- Verify: Is the wider system working consistently in practice?
- Review: Does the control remain effective after changes or new information?
Testing can support verification, but testing alone is not a control. One result represents one sample, in one location, at one point in time. The question is not simply whether the required activities have been completed. The question is whether the combined evidence shows that the controls consistently achieve their intended outcome.
Key Takeaways
- Confidence isn’t evidence; allergen controls need proof they’re working
- Controls should be validated, monitored, corrected, verified and reviewed
- Validation confirms a control can achieve its intended outcome
- A single test result reflects one sample, in one location, at one point in time. The real question is whether combined evidence shows controls consistently achieve their intended outcome
5 Actions To Take Today
To finish the webinar, Alex brought the discussion back to the factory floor with five practical actions that can be taken immediately at your site.
1. Risk Assessments
Every risk assessment should be specific to the line, product and site. Avoid simply copying an assessment from another area, as this can be a red flag for auditors.
Don’t just write the assessment at your desk. Walk around the factory and observe things like where products are transferred and where rework takes place. Watch a changeover and follow the movement of equipment and people.
Most importantly, involve the people who actually work there. An operative on the line may be able to identify a practical risk in two minutes that would never appear in a desk-based review.
2. Keep It Simple
Allergen management systems can become increasingly complicated over time. Every audit and near miss can add another form or sign-off. Eventually, the system may make perfect sense to the technical team but become difficult for everyone else to follow.
The test is simple: Does it still work at 3am under pressure? Use clear language, visual controls, colour coding and effective signage. If an operative cannot explain the process in their own words, the issue may be with the procedure rather than the person.
3. Bring In External Eyes
Familiarity can create blind spots. When you walk past the same equipment and processes every day, it becomes easy to stop noticing things that someone unfamiliar with the site would immediately question.
An external perspective does not necessarily mean hiring an expensive consultant. It could be another food manufacturer, technical manager, subject matter expert, or supplier. The important thing is to have someone challenge your assumptions.
4. Create Ownership
There is a difference between responsibility and ownership: responsibility can be written into a job description, but ownership is when people genuinely care about whether the control works. Allergen management should not sit solely with the technical team: production controls the schedule, engineering changes equipment, purchasing manages suppliers, NPD changes recipes, and hygiene manages cleaning. Every function has a role to play. Bring those teams together and make sure everyone understands why their actions matter.
5. Treat Allergen Management as a Journey
Allergen management is not something you fix once and move on from. Factories, products, suppliers, and people all change, and every change can introduce new risk. That means risk assessments need to be revisited, controls need to remain visible and teams need to keep looking for opportunities to improve. The aim is to keep allergen management alive rather than allowing it to become another set of documents that only receives attention before an audit.
Key Takeaways
- Review risk assessments on the factory floor, not just at a desk
- Keep processes simple enough to work under pressure
- Use external perspectives to challenge assumptions
- Build allergen ownership across the whole business
- Treat allergen management as continuous improvement, not a one-off project
Webinar Q&A
Do you expect changes to allergen management in BRCGS Issue 10?
Alec explained that he expects developments around Codex allergen thresholds to be considered, although he could not confirm what changes may be made. The existing BRCGS Global Standard for Food Safety already contains requirements around allergen management and precautionary allergen labelling, including the need for a suitable risk assessment.
Why does the UK have more recalls than other countries?
The panel was asked whether higher UK recall numbers indicate weaker controls or a greater willingness to report incidents. Alec said he would not draw a direct conclusion from the numbers alone. Recall data can be influenced by many factors, including how businesses and regulators identify and report issues. The wider point was that businesses should focus on protecting consumers rather than setting a target of having no recalls. A target that discourages reporting could create the wrong behaviours.
Can AI help identify system vulnerabilities?
Wendy explained that AI is already being used in areas including labelling, packaging and raw material checks. The technology is developing quickly and could provide additional tools to support food safety management.
Additional Q&As
We ran out of time to answer all of the questions during the live session, so Alec and Wendy shared their thoughts on the remaining questions below.
Is the allergen control regarding the premix change, managed via the change control process, sufficient?
Having a change control process is an excellent start and ensures that a management system is in place to prompt the review of allergen controls when such changes happen. Of course, it is then a matter of ensuring that the actual review is conducted thoroughly, taking account of any new allergen hazards introduced by the new ingredient or process and ensuring that the correct controls are put in place. This must include processes, procedures and training, to name just a few of the many considerations needed to ensure that change is managed safely. The change should not be approved until the required controls have been implemented and verified across all affected functions.
We use a fish collagen ingredient that is fully hydrolysed (broken down) during processing. The usual fish allergen test we conduct is ELISA for fish protein. The lab says that ELISA only detects parvalbumin, but this protein is destroyed by the hydrolysis process (the raw material we use). So these tests always come back negative, even if we take swabs before cleaning.
Can this happen, and what other ways would you suggest to prove there is no fish allergen risk in an ingredient like this?
One approach that could be considered is to use a generic indicator of the presence of protein, as this will indicate the removal of wider protein residues. In such circumstances, it would be useful to establish that wider protein residues are present prior to cleaning.
For fish testing, we tend to apply DNA-based detection, as it helps with a spread of variety as well as damage due to processing.
Processing of fish products is known to cause issues with detection. Many companies where detection is an issue, due to processing or the presence of low levels, look for another marker to show that the allergen-containing product has been removed, rather than testing for the allergen itself. I would look at the product and see what else could be tested for.
It’s also worth noting that swabbing will always reduce the chance of detection, simply because it requires two transfer steps (onto and from the swab), and transfer efficiency at each step is known to be low. Therefore, it’s important to ensure that final product testing is performed as well.
From a statistical perspective, which parameters should be taken into account when assessing and recording allergen-related incidents? Besides the level of risk and the frequency of occurrence, should the number of people affected also be considered? And how should we account for cases that remain unreported?
If the question is about the considerations to take into account when determining the significance of an allergen contamination event, the key points should include the assessment of the hazard and the likelihood of exposure.
The hazard assessment should include consideration of the quantity present in a portion, given foreseeable consumption circumstances, and the levels likely to elicit a reaction in the susceptible population.
The exposure assessment should include the number of packs in the marketplace and the number of potentially affected packs. This can be informed by reported complaints, but complaint data is an unreliable measure, and the assessment should be driven by the extent of the contamination event in production. Complaint data is useful in triggering an incident investigation, but customers who do not have an allergy may not be motivated to report events that could be dangerous to those who do.
If you are a nut-free site, can you have products with “may contain” labelling?
If you are making a nut-free claim on pack at a nut-free site, then you should not be handling nuts on site, and neither should you use any ingredients that carry a nut precautionary allergen label (PAL) in the nut-free product. This is because, implicitly, if an ingredient has such a warning statement, it should carry through to the finished product, and it is not permissible to have a PAL on a product with a free-from claim, other than gluten-free (as that has a defined level).
There are conceivable circumstances where this might not be the case, based on a risk assessment of carry-over allergens in the ingredient with the PAL statement, and the introduction of allergen thresholds might further change this, but that would need a more detailed risk assessment.
Handling ingredients that have a nut PAL statement at a nut-free site may also be possible where such ingredients are not being used in a product with a nut-free claim. However, this requires a detailed risk assessment to ensure effective separation and management of any potential cross-contamination risks.
So there you have it, the key takeaways from the first webinar in our three-part series with Campden BRI: Allergen Management: Closing the Gap.
- Part 1: Click here to access the webinar recording and presentation slides.
- Part 2: Best Practice Cleaning Regimes takes place on Tuesday 20th October and will explore cleaning validation, shared equipment, cross-contact and what good cleaning looks like.
- Part 3: Food Safety Culture and People takes place on 17th November and will look at the role people and culture play in effective food safety management.
If you have any questions about allergen management or the support we can provide here at Klipspringer, you can contact our team on 01473 461 800 or email sales@klipspringer.com. Alternatively, fill out the form below.
If you have any questions about allergen management and the support we can provide here at Klipspringer, share your contact details below.
6 Benefits of In-Process Optical Monitoring in Food Manufacturing
Discover 6 Benefits of In-Process Optical Monitoring for Your Food Production Site
From identifying the root cause of problems to supporting cleaning, maintenance and audit preparation, In-Process Optical Monitoring gives food manufacturers a clear view of what is happening inside their equipment during production.
Here are 6 benefits of In-Process Optical Monitoring to consider if you are thinking about introducing this solution to your site.
What Is the In-Process Optical Monitoring System?
The In-Process Optical Monitoring System travels through your production process under normal operating conditions, capturing high-definition footage of what is happening inside your equipment. It gives your team a clear view of the process without the need for downtime or equipment dismantling, providing valuable visual information alongside your existing data.
Key Features
Travels with the product
Travels through the full process under normal production conditions, capturing what happens as the product moves through each stage.
4K high-definition video
Records continuous footage which can be reviewed after each run to investigate equipment condition and process performance.
Built-in illumination
A high-temperature torch provides up to 1,000 lumens, with adjustable intensity and beam width for clear footage, even inside unlit ovens.
Forward or reverse-facing
The system can be configured to face forwards or backwards, providing visibility of different areas within your equipment.
Withstands temperatures up to 300°C / 572°F
Designed for high-temperature environments, with a max operating temperature of 300°C and a thermal duration of up to one hour at 250°C.
Constructed from 316 stainless steel with an IP65-rated enclosure
A durable solution designed to withstand moisture and demanding food factory environments.
1. Find the Root Cause of Problems
An In-Process Data Logger can be a useful tool for identifying when something isn’t quite right. It might show that a zone is running cold, a result is inconsistent, or a reading has started to drift. However, while this data can tell you what is happening, it doesn’t always tell you why.
This is where optical monitoring can provide valuable additional insight. By capturing what is happening within the process, it allows you to see the physical conditions behind the data and identify potential causes more quickly.
Your team can use the footage to understand what is happening, investigate the root cause, and take appropriate action with greater confidence.
2. Reduce Foreign-Body and Contamination Risk
Over time, equipment can develop issues that aren’t always immediately visible. Damaged insulation, loose debris, and the build-up of condensation can all create potential risks within the production environment.
If material breaks away and enters the product, it can become a foreign-body hazard. The consequences can include contaminated batches, costly recalls, production downtime and, most importantly, a potential risk to consumer safety.
Optical monitoring provides an additional layer of protection by giving your team greater visibility of what is happening within the process. By helping to identify developing issues, it can give you the opportunity to investigate and take action before they become a more serious food safety incident.
3. Create Visual Evidence of Equipment Condition for Audits
During an audit, it’s important to be able to demonstrate that potential risks are being actively monitored and managed across your site, rather than simply relying on written records.
Optical monitoring can provide a dated, reviewable record of what is happening inside your equipment during each run. This gives your team visual evidence that can complement documented inspections and help to demonstrate that any issues identified have been followed up.
It can also be useful when carrying out repairs. By comparing footage from before and after an intervention, you can clearly see what has changed and provide an audit-ready record of the work carried out.
4. Catch Maintenance Issues Early
Unplanned stoppages are expensive, and many can start with small equipment faults that go unnoticed. Optical monitoring provides visibility of the condition of internal components, this includes damage to chambers, insulation, and individual parts.
Regular checks give maintenance teams a clearer picture of equipment condition and make it easier to keep track of developing faults.
Instead of waiting for a component to fail and dealing with an unexpected breakdown, maintenance can be planned around production schedules and existing maintenance activity.
5. Plan Cleaning from Evidence, Not Guesswork
Fixed cleaning schedules don’t always reflect what is actually happening inside your equipment. Some areas may need cleaning sooner than expected, while others may require less frequent attention.
Optical monitoring shows where build-up is occurring, giving your team a clearer basis for deciding when and where cleaning is needed. This can help ensure cleaning activity is focused on the areas that actually require attention, rather than relying solely on a fixed schedule.
The footage can also provide a useful record after cleaning, allowing your team to compare the condition of the equipment and assess the result.
Just as importantly, these inspections can be carried out without stopping production or dismantling equipment. Internal checks can become a routine part of the cleaning process, rather than something reserved for scheduled shutdowns.
6. Understand Product Behaviour
Optical monitoring doesn’t just provide a view of the equipment itself. It can also show how your product behaves as it moves through the process.
This includes changes in colour, shape and size, as well as differences in bake uniformity from one zone to another. Seeing these changes as they happen can give your team a clearer understanding of how process conditions are affecting the finished product.
The footage could also be used to show how a conveyor belt is moving and if product transfer issues occur. This provides a visual reference for investigating problems that may otherwise be difficult to pinpoint from process data alone.
Part of a Complete Process Monitoring Solution
The Multi-Channel In-Process Data Logger gives you detailed temperature data from throughout your production process, helping you understand how your equipment is performing and identify potential hot or cold spots. With up to 20 thermocouples, it can be used for temperature profiling, HACCP cook validation, and investigating process inconsistencies.
When used alongside the In-Process Optical Monitoring System, you can take this a step further. While the data logger shows you what is happening with temperature, the optical system can help show you what is happening inside the equipment at the same time.
Together, they provide a more complete picture of your process, helping your team investigate problems, validate performance, and make informed decisions based on both data and visual evidence.
So there you have it, 6 benefits of using an In-Process Optical Monitoring System at your food production site.
If you have any questions about the system or how it could support you and your team, contact us on 01473 378 517 or email sales@klipspringer.com. Alternatively, fill out the form below.
If you would like to learn more about the In-Process Optical Monitoring System, share your details below and a member of our team will be in touch.

Webinar Round Up: Peak Production: Springboard or Setback?
Insights from our Industry Webinar on Leveraging Real-Time Monitoring for Meaningful Insights in Food Production.
In this article, we recap key insights from our recent webinar exploring how food manufacturers can manage the added pressure that comes with peak production, while protecting standards, efficiency, and margin. The session featured key insights from:
- Alex Carlyon, Key Account Director, Klipspringer.
- Lars Turner, Director, Foodclean.
If you are short on time, you will find a bulleted list of key takeaways at the end of each section.
Busy vs Profitable: Why Does Peak Production Not Always Mean More Profit?
Key Takeaways
Where Does Profit Leakage Come From?
1. Equipment Strain
2. Labour Costs Climb
3. Seasonal Specials
4. Defects and Errors
5. Over Production
6. Logistics and Supply Chain
7. Consumer Promotions
Retailer-funded deals often come with their own cost structure and can carry a penalty risk if an issue arises on the manufacturer’s side. This risk can be heightened during peak periods compared with standard operating times.
8. Immeasurable Costs
9. Audit Season
Key Takeaways
5 Actions To Take Immediately
1. Plan Ahead
2. Walk the Floor
3. Build Goodwill
4. Prime Your Partners
5. Slow Down to Speed Up
Key Takeaways
Webinar Q&A
Which areas of profit leakage are most likely to catch sites off guard during peak production?
How can we get senior management engaged when there is a disconnect between the boardroom and the shop floor?
When things get tight, what should you flex on and what is non-negotiable?
If you have any questions about peak production and the support we can provide here at Klipspringer, share your contact details below.

5 Ways Hospitality Teams Could Use Real-Time Monitoring and AI
How real-time monitoring and AI could help hospitality teams to identify problems earlier, reduce waste, and cut costs.
Real-time monitoring is more than a compliance tool. Data from temperature, energy, water, door contact, and equipment monitoring can provide valuable insight into how a hospitality site operates, helping teams to identify issues earlier, reduce waste, and control costs.
AI can take this one step further by analysing data, identifying patterns, and highlighting changes that may otherwise be missed. In this article, you will discover five examples of how this combined approach could be applied at your site.
Or, for a broader look at how AI could support your hospitality team, download our daily, weekly and monthly round-up below.
Understanding When Equipment Uses the Most Energy
Hospitality sites rely on a wide range of energy-intensive equipment, from commercial dishwashers and laundry equipment to HVAC systems and refrigeration.
Without detailed monitoring, it can be difficult to understand exactly when energy demand is highest or which equipment is contributing most to consumption.
Real-time energy monitoring provides a clearer picture of how and when electricity is being used. This can help teams identify equipment that is operating unnecessarily or processes that could potentially be moved to different times of the day.

The Role of AI
AI can support this analysis by identifying recurring patterns in energy consumption and helping teams understand when demand is likely to increase. This information can then be used to make operational changes where appropriate, while avoiding disruption to guests or day-to-day service.
Identifying Unusual Water Usage
Water is essential across hospitality sites, from kitchens and bars to guest facilities and cleaning operations. As with energy, understanding how much water is being used and where it is being consumed can help teams identify opportunities to reduce waste.
Real-time water monitoring can track consumption across different areas of a site, providing teams with a clearer view of normal usage patterns.
A sudden increase in consumption may indicate a leak, equipment issue or another problem that needs investigating. Identifying these changes quickly can help to prevent wasted water, higher bills and potentially more significant operational problems.

The Role of AI
AI can add another layer of analysis by identifying unusual patterns in water consumption and highlighting changes that may otherwise be difficult to spot. Across larger businesses, this can also help teams compare sites and identify locations where further investigation may be required.
Identifying Refrigeration Problems Early
Refrigeration equipment can become less efficient long before a fault becomes apparent. A gradual change in temperature or operating performance may go unnoticed during routine checks, while the equipment continues to consume more energy.
Real-time monitoring provides continuous visibility of temperatures across fridges, freezers and cold rooms, making it easier to identify changes from normal operating conditions.

The Role of AI
AI can build on this by analysing data over time and identifying unusual patterns across multiple units. This can give teams an earlier indication that equipment may need attention, allowing them to investigate potential problems before they develop into more costly failures or increased energy consumption.
Reducing Energy Loss from Open Doors
Fridge and freezer doors can be opened frequently during busy kitchen operations. Although each individual incident may seem minor, repeatedly leaving doors open can increase energy use and affect internal temperatures.
Wireless monitoring systems can automatically track door activity, including how often doors are opened and how long they remain open. Alerts can also be configured when a door stays open beyond a set period.

The Role of AI
By reviewing this information, hospitality teams can identify which units or areas are most affected and take targeted action. AI can provide further insight by comparing door activity with temperature data, helping teams understand the impact of repeated door openings and identify patterns across different shifts or sites.
Preventing Equipment Breakdowns
Extraction fans, HVAC equipment, ice machines and other operational equipment often run continuously in the background. When a motor or other component begins to deteriorate, there may be warning signs before a complete failure occurs.
Vibration monitoring can help to detect changes in equipment behaviour, providing an indication that maintenance may be required. This gives teams the opportunity to investigate an issue and plan maintenance before an unexpected breakdown causes disruption.

The Role of AI
AI can also analyse vibration data and compare current readings with previous patterns. Where similar changes have been associated with equipment failures in the past, this can provide an additional early warning and support a more proactive approach to maintenance.
Small improvements can add up over time, particularly across multiple sites. For hospitality businesses already collecting monitoring data, making better use of that information could be an important step towards reducing operating costs while supporting wider sustainability objectives.
To find out how real-time monitoring could work for your site, get in touch on 01473 461800 or sales@klipspringer.com. Alternatively, share your details via the contact form below.
If you would like to learn more about Real-Time Monitoring, share your contact details below.

WEBINAR: Allergen Management: Closing the Gap
The Allergen Management Series
WEBINAR: Allergen Management: Closing the Gap
Allergen recalls remain a persistent problem across the industry. So why, despite significant investment, aren’t the trends moving in the right direction?
Following the success of our webinar on allergen testing best practice, we’ve teamed up with Campden BRI for a three-part webinar series on allergen management in food manufacturing. Part One features Independent Food Safety Consultant Alec Kyriakides and Wendy Duncan, Safety, Quality & Allergens Manager at Campden BRI.
In this session, Alec opened with a top-level overview of the relevant regulations and what the upcoming Codex changes mean for manufacturers. He then looked at what we can learn from recall data and root cause analysis. Wendy then explored why allergen failures happen and where the greatest risks lie, sharing guidance on keeping procedures effective across the entire production journey. Finally, Klipspringer Director Alex Carlyon shared five practical steps you can take immediately, ensuring you leave the webinar with a clear plan of action.
Webinar Speakers
Alex Carlyon
Key Account Director
Klipspringer
Wendy Duncan
Safety, Quality & Allergens Manager
Campden BRI

Alec Kyriakides
Independent Food Safety
Consultant
Keynote Speakers
Wendy Duncan
With more than 25 years in food manufacturing, Wendy has built her career in the FMCG sector across the UK and Europe. She now leads on allergens within Campden BRI’s Food Safety Management Systems team, where her training and consultancy work helps clients get to grips with allergen risk and ensure compliance.
- Member of the FDF Allergen Steering Group
- Technical Committee of the Federation of Bakers (Safety and Allergen Support)
- Member of RSPH
- Associate IFST member

Alec Kyriakides
A highly respected food safety expert, Alec began his career as a microbiologist before spending 28 years at Sainsbury’s, rising to Head of Technical Operations. He is a recognised thought leader, author and speaker across the food industry, bringing decades of scientific and technical expertise to his consultancy work.
- Board Trustee of the Institute of Food Science and Technology
- Chair of the BRCGS International Advisory Board
- Chair of the Safe to Trade Technical Standards Committee
- Member of the LGC Science Advisory Board
- Member of the Advisory Committee on the Microbiological Safety of Food
Key Webinar Areas
1. Your Obligations and What Is Going Wrong?

2. Why is Your Allergen Management Failing You?

3. Making It Real: 5 Ways to Start Today
4. Live Q&A with the expert panel

WEBINAR: Peak Production: Springboard or Setback?
WEBINAR: Peak Production: Springboard or Setback?
Peak season pushes everyone, and everything, harder.
It means increased volume, extra seasonal SKUs, tighter turnarounds and shorter windows. It’s also when equipment gets pushed past its normal limits, new staff are still learning your processes, and auditors tend to show up at the worst possible time. The pressure to keep output moving can quietly wear down the standards you’d normally adhere to.
And when efficiency drops, costs go up. This eventually shows up in decisions we don’t always get a say in, like next year’s budgets for new equipment and day-to-day running costs. So this isn’t just a production problem to manage; it’s one we end up living with long after peak is over.
This webinar is for production, technical, hygiene and engineering teams managing that pressure directly. We look at where the leaks really happen at peak, what’s realistic to control, plus how to protect standards and margin.

Webinar Speakers
Alex Carlyon
Key Account Director
Klipspringer

Lars Turner
Director
Foodclean
Key Webinar Areas

1. Exploring the crucial difference between busy and profitable

2. Where do the profit leaks happen?

3. What can we actually control?

4. Five actions to implement immediately.
5. A live Q&A with our panel of experts.

Shadow Boards for Food Production Sites: Frequently Asked Questions
Your Shadow Board Help Guide, covering mounting, cleaning, audits, colour coding, installation and employee engagement.
Shadow boards are a simple way to keep equipment organised, accessible and audit ready. But when it comes to introducing them to your site, it’s natural to have questions.
From mounting options and cleaning requirements to audit expectations and employee engagement, this guide addresses some of the most common talking points to help you get the most from your shadow boards.
What exactly is a shadow board?
A shadow board is a storage panel with a visible outline, or “shadow”, for each piece of equipment it holds. This makes each tool’s designated space instantly recognisable, so it’s immediately clear whether the tool is present or missing.

In food production, shadow boards are typically used to store tools and cleaning equipment. They serve a dual purpose: keeping equipment organised and accessible while making it immediately obvious if anything is missing, damaged, or has strayed from its designated zone.
Can shadow boards be magnetic?
Yes, magnetic mounting is the most popular option for wall-mounted shadow boards, and for good reason. It allows for quick installation and, crucially, easy removal for cleaning, addressing one of the most common hygiene concerns.

Magnetic boards are usually straightforward to install, particularly if your site already has magnetic walls. However, if this isn’t the case, there are still options to consider. For instance, a steel composite panel can be fitted to the wall first, providing a secure surface for the boards to attach to.
And if you’re concerned about magnets supporting heavier equipment, additional magnets can usually be incorporated at the design stage to accommodate the extra weight.
What is needed to get boards in place before a specific audit deadline?
If you’re working towards a specific audit deadline, the lead time for your shadow board should be one of the first things you consider. The quickest option will depend on whether you need a standard board or a bespoke design.
For a bespoke shadow board, it’s important to allow time for the full process, including design sign-off, manufacture and delivery.
At Klipspringer, our industry-leading turnaround time is 5 to 7 working days.
If time is particularly tight, we also offer “buy it now” boards for popular equipment combinations. These ready-to-order options can help to reduce the time between placing your order and getting a board in place.

It is also worth noting that freestanding and magnetic boards can be among the quickest solutions to get in place because they don’t require your maintenance team to drill fixings into the wall.
They can be positioned and put to use straight away, making them particularly useful when an audit is approaching or a non-conformance around equipment storage has already been flagged.
Can boards sit at the point of use on the line (rather than centrally) to cut retrieval time?
Absolutely. This is one of the simplest ways to improve the return on a shadow board investment. Rather than housing all your equipment on a handful of large, centrally located boards, many sites get better results from smaller boards positioned closer to where the tools are actually used.

Mobile freestanding boards fitted with braked castors are ideal for this. They can be wheeled to the point of use and easily moved if your production lines change.
This approach reduces the time operatives spend walking to retrieve equipment, supports the “point of use” principle within 5S, and can improve accountability, as it becomes immediately obvious if say a tool from Line 2 has ended up on Line 4.
How do you clean shadow boards?
The mounting method makes a big difference here. Magnetic or freestanding boards can simply be lifted off the wall or wheeled away for cleaning, allowing you to clean both the board itself and the wall behind it. This helps to avoid the classic problem of hard-to-reach gaps and fixings becoming potential harbourage points for bacteria.
If you have boards that are permanently fixed to the wall, there is a wide range of detail cleaning equipment that can be used to clean behind them.

Beyond the mounting method, look for boards with a through-board hook system rather than rails, as rails and small fixings can create crevices that are difficult to clean properly. Materials should also be able to withstand your site’s standard cleaning chemicals without degrading.
It’s worth formalising all of this in your site’s Cleaning Instruction Cards (CICs), including how often the boards should be cleaned, which products should be used, and what condition they should be in before production starts. Involving your hygiene team early in the board design process can make this step much easier.
What are the audit requirements around shadow boards?
There isn’t an audit standard that mentions shadow boards by name, but they consistently support many of the areas auditors focus on. Poor housekeeping and the incorrect storage of small utensils are common sources of non-conformances, and shadow boards help to address this by giving every tool a clearly defined and visible home.
More broadly, shadow boards support the type of evidence auditors look for under standards such as BRCGS, including clear equipment storage, colour-coded segregation to help prevent cross-contamination, and a visible commitment to hygiene and organisation across your site.

Another common question is whether empty “shadows” during audits can result in a non-conformance. The simple answer to this is no, but you can click the button below to access a more in-depth article on shadow boards and audit compliance.
What if I’ve run out of colours for my colour-coded equipment, how do I introduce a new shadow board?
This is a common problem on sites with a large number of zones, particularly once you’ve worked through the most popular colour options.
Rather than introducing colours that are difficult to distinguish at a glance, which can undermine the purpose of colour-coding, it’s often better to add additional visual cues. Clear header text on shadow boards can make it easier for teams to identify the relevant zone or production line, while IndeliMarking your equipment provides another layer of distinction.

This is also a good opportunity to review your overall colour-coding policy. Sometimes a scheme has become complicated over time and can be simplified rather than expanded further. Click the button below to access a guide to simplifying your on-site colour-coding policy.
How do I ensure employee engagement with shadow boards?
A shadow board is only as effective as the culture around it, so it’s important that your team is engaged. Below are four factors to consider:
- Ongoing training: Teams should understand not just how to use the boards, but why they matter. Faster retrieval, less equipment damage, and fewer non-conformances are all clear benefits.
- Accountability: Some sites assign responsibility for specific boards to shift managers or nominate “board champions” who are responsible for checking that equipment is accounted for.
- Reinforce instructions: Simple headers such as “Return equipment after use” or “Clean before returning to board” provide a constant, low-effort reminder.
- Make the boards highly visual: Shadow boards that are well branded, clearly laid out and genuinely convenient tend to see much better engagement.

With the right approach, a shadow board can become a simple but valuable part of your site’s everyday organisation and hygiene standards.
If you have any questions we haven’t covered in this guide, contact us on 01473 461 800 or sales@klipspringer.com. Alternatively, fill in the form below and we’ll be in touch.
If you would like to learn more about shadow board storage solutions or have any of your own questions to share, we would be happy to hear from you.

What Are the Different Collection Systems for Industrial Vacuum Cleaners?
Help Guide: The Two Different Collection Systems for Industrial Vacuum Cleaners
The collection system is an important consideration when selecting an industrial vacuum cleaner.
This guide explains the two main collection systems commonly available: Continuous Bag Systems and Barrel Collection Systems. Understanding how each option works will help you identify the most suitable solution for your site.
Barrel Collection System

The Barrel Collection System is the most common collection method used on industrial vacuum cleaners.
Collected material is deposited into a rigid metal container positioned beneath the filtration system. Once the container reaches capacity, it is removed, emptied, and returned to the vacuum for continued use.
Barrel Collection Systems are suitable for a wide range of applications and can be used to collect dry dust, heavier debris, and, on compatible models, liquids.
Benefits | Limitations |
Simple, durable design: The rigid collection container is designed for repeated use without disposable bags. | Greater operator exposure during emptying: Removing and tipping the container may expose operators to collected dust or debris. |
Suitable for a wide range of materials: Ideal for collecting dust, larger debris, swarf and, on suitable models, liquids. | Requires manual handling: Larger containers can become heavy when full and may require additional effort to empty safely. |
No ongoing consumable costs: The same collection container is emptied and reused throughout the life of the vacuum cleaner. | Interrupts cleaning: The collection container must be removed and emptied before operation can continue. |
Available in a range of capacities: Different container sizes allow the vacuum to be matched to the application. | Less suitable for hazardous dusts: Additional precautions may be required when disposing of hazardous materials. |
Easy to inspect: Operators can quickly monitor the fill level and empty the container as required. | Increased risk of spillage: Material can be spilled during transport or emptying if the container is not handled carefully. |
Liquid Containers

Within the range are industrial vacuum cleaners suited to removing liquids and water in food production environments.
These feature solid containers with drains for quick, easy liquid removal: the hose can simply be released from its holder, angled downward, and used to drain the container.
This system helps teams to avoid lengthy downtime and reduces the risk of operator injury, as there’s no need to lift and tip heavy, liquid-filled containers.
Continuous Bag System

A Continuous Bag System is designed to allow collected material to be disposed of with minimal operator input. Instead of collecting dust within a removable container, material is deposited into a continuous tube of durable plastic film. As the bag fills, the operator quickly seals and separates the filled section before continuing to collect material using the remaining length of the bag.
This enclosed disposal method makes Continuous Bag Systems particularly well suited to applications involving fine powders, hazardous dusts, or environments where reducing operator exposure is a priority.
Step 1
Seal the bag cassette at one end with a cable tie. Once the “bag” starts to fill, pull it down so new material is drawn from the cassette to make it longer.
Step 2
To make a new bag, pull the material down from the cassette until it is the length that you require. Seal it at the top with a cable tie.
Step 3
Add another cable tie above the first one and cut the bag material between the two cable ties. The entire process takes less than 30 seconds.

Benefits | Limitations |
Minimises operator exposure: Collected material remains enclosed within a sealed bag during disposal, reducing contact with dust. | Primarily intended for dry materials: Continuous Bag Systems are best suited to dry dusts and powders rather than liquids or larger debris. |
Reduces environmental contamination: Sealing the bag before removal helps to prevent dust from becoming airborne during emptying. | Ongoing consumable costs: Replacement bag rolls are required throughout the life of the vacuum cleaner. |
Supports continuous operation: Filled sections can be sealed and removed quickly, helping to minimise downtime. | Not available on every model: Continuous Bag Systems are typically offered on vacuums designed for dust collection rather than general wet-and-dry applications. |
Suitable for hazardous dust applications: Well suited to environments where safe disposal of fine or potentially hazardous dust is required. | Less suitable for bulky waste: Larger offcuts, swarf and other heavy materials are generally better suited to rigid collection containers. |
Reduces manual handling: Operators handle sealed bags rather than loose collected material, helping to minimise spills during disposal. |
By considering the type of material being collected, the frequency of use, and the method of disposal, you can choose the right Collection System for your site.
For any questions about the Klipspringer range of Industrial Vacuum Cleaners and Accessory Kits, contact us on 01473461800 or sales@klipspringer.com. Alternatively, you can fill out the contact form below and we will be in touch.
If you would like to learn more about the Industrial Vacuum Cleaners mentioned throughout this article, share your contact details below.
Equipment Storage Solutions for Commercial Kitchens
Discover how smart storage solutions can improve organisation and efficiency in your commercial kitchen.
Equipment storage is a small change that makes a big difference to how a kitchen runs day to day. It helps teams to work faster, stay organised, reduce costs, and maintain the standards that hospitality businesses are held to.
In this article, we’ll look at why equipment storage matters, and explore three practical solutions that can help you get the right system in place for your site: shadow boards, header boards, and instrument stations.
Why does equipment storage matter?
The right equipment storage isn’t simply about making a kitchen look tidy. It helps to create a culture where equipment is visible, accessible, protected, and properly cared for. A well-designed storage system can help you to:
- Reduce downtime by making equipment instantly locatable
- Reduce repair and replacement costs through safer storage
- Create a culture of care and ownership across the team
- Improve segregation and awareness around food safety and allergens
- Support 6S Lean Management and visual workplace standards
- Make training easier for new and temporary team members
- Create consistent standards across multiple areas and sites
1. Shadow Boards: Make Every Piece of Equipment Visible

Shadow boards are a popular way to give equipment a clearly defined home.
Each item has its own outlined position, making it immediately obvious what should be there and what is missing. This creates a simple visual management system that teams can understand at a glance.
Shadow boards can be particularly useful for:
- Kitchen utensils
- Knife stations
- Spill kits
- PPE stations
- Cleaning equipment
- Other frequently used handheld equipment
Shadow boards can be customised to suit your site, including colour coding, labels, branding and instructional messaging.
This should make equipment a lot easier to find, easier to return and less likely to be left on work surfaces or in unsuitable locations.

Request an Audit
If you’re not sure which solution is right for your site, we can help you to identify where better storage could save time, protect equipment and improve your kitchen’s visual standards.
Request a FREE shadow board audit and discover what could work for your team.
2. Header Boards: Smart Storage If Space Is Limited
Not every kitchen has the wall space for a
full-length shadow board. That’s where header boards can provide a practical alternative. Header boards use available wall space efficiently while keeping equipment organised, visible, and easy to locate.
Just like larger shadow boards, header boards can be customised with colour coding and company branding.

3. Instrument Stations: Protect Valuable Kitchen Equipment
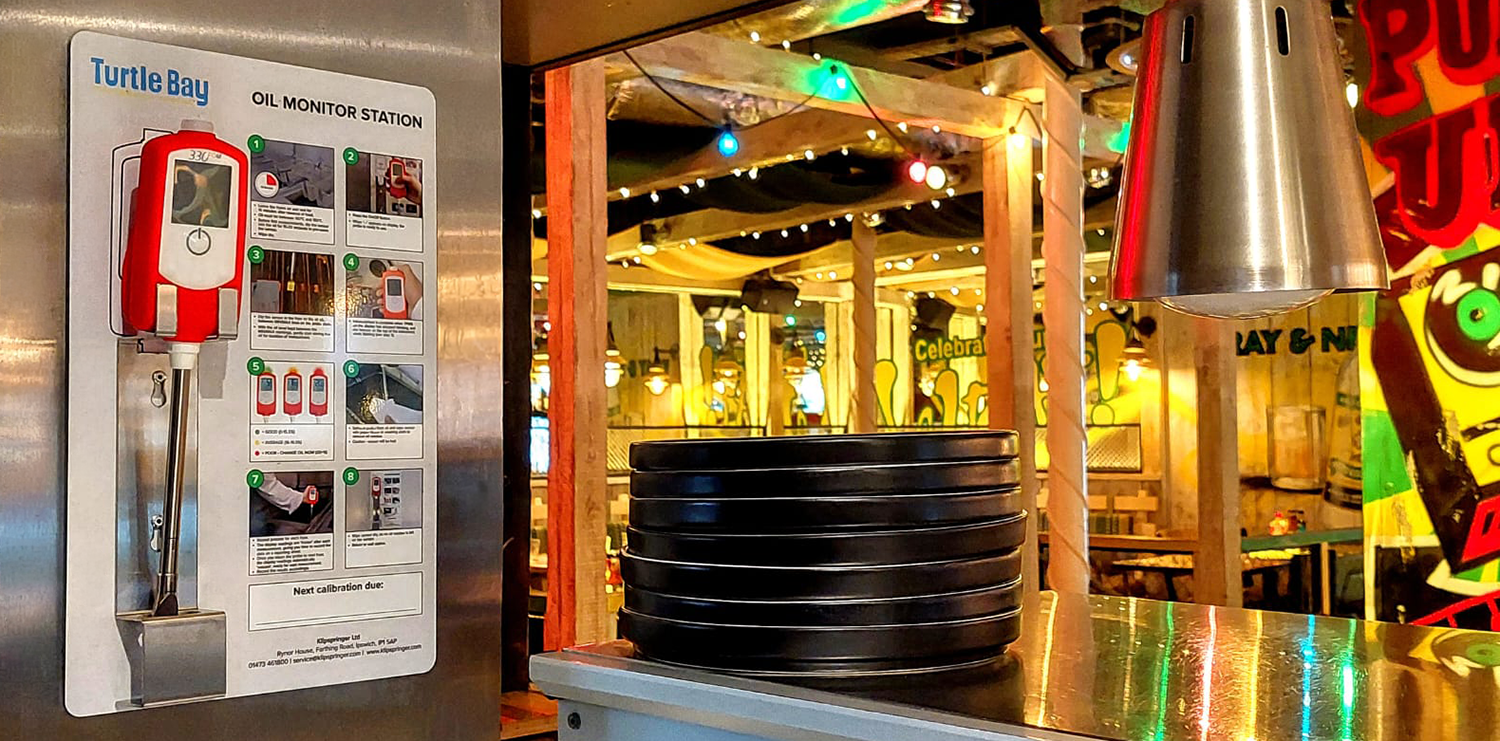
Thermometers, food oil monitors and other handheld instruments play an important role in maintaining food safety and quality. But they can also be vulnerable to damage when they aren’t stored correctly. Correct handling and storage can help to prevent this damage, reducing downtime and the cost of repairs or replacements.
Instrument stations provide a dedicated home for valuable equipment, keeping it protected, accessible and ready for use. They can be supplied as standard designs or customised around the needs of your site. For example, your station could include:
- Step-by-step instructions for use
- Cleaning instructions
- Photos showing correct procedures
- Dedicated holders for accessories
- Storage for wipes
- Space for digital tablets or other equipment


Whether you have plenty of wall space or need to make every inch work harder, the right storage solution can make a surprisingly big difference to the way your kitchen operates.
If you have any questions about equipment storage, you are welcome to contact our team on 01473461800 or sales@klipspringer.com. Alternatively, you can share your details via the form below and we will be in touch.
If you have any questions about shadow boards, header boards, or instrument stations, share your contact details below and we will be in touch.

About the Author
Libby Loughnan is Content Manager at Klipspringer, specialising in food safety and compliance. She writes extensively on helping commercial kitchens improve food safety, cut costs, and work more efficiently, covering everything from equipment storage to food oil management.

WHITE PAPER: Getting Allergen Testing Right: The Foundation
WHITEPAPER
Getting Allergen Testing Right:
The Foundation
Food manufacturers continue to invest heavily in allergen control, yet allergen-related recalls remain a persistent challenge across the industry.
This white paper outlines the key principles required to build a robust allergen testing programme and establish confidence in allergen control.


WHITE PAPER: Rapid Allergen Testing: A Practical Guide for Food Manufacturers
WHITEPAPER
Rapid Allergen Testing:
A Practical Guide for Food Manufacturers
Rapid allergen tests are widely used across the food manufacturing industry, yet many sites continue to struggle with uncertainty around best practice.
This white paper provides a practical guide to rapid allergen testing. It explains how different testing methods work, when they are most effective, and the key considerations for generating reliable and meaningful results.


What Are the Different Motor Options for Industrial Vacuum Cleaners?
Help Guide: Exploring the Different Motor Options for Industrial Vacuum Cleaners
The motor is one of the most important components of an industrial vacuum cleaner, determining key factors like suction performance, operating life, maintenance requirements and the type of application the vacuum is best suited to.
This guide explains the different motor options available across the Klipspringer range, helping you to make the right choice for your site.

Turbine Motor
Turbine Motors (also known as side-channel or regenerative blowers) deliver reliable suction during extended or continuous operation. A rotating impeller sits inside a specially shaped channel, and as it spins, each parcel of air is picked up and re-accelerated by the blades multiple times as it travels around the channel, rather than passing the blades just once, as in a standard motor. This repeated acceleration is what lets a simple, single-moving-part design build strong, steady suction.
Higher-performance vacuum models are fitted with multiple turbines rather than one, to boost vacuum level, depending on what the model is built for.
The turbine configuration is matched to the vacuum at the design stage, so each model is supplied ready-built for its intended application. Some models also pair the turbine with an inverter, giving adjustable motor speed for variable performance.
Benefits | Limitations |
Continuous operation: Designed to run reliably during extended or 24/7 use | Fine dust collection: Best suited to general and coarse dust. Centrifugal fan systems are typically preferred for very fine dust applications |
Simple design: Mechanically straightforward, with reliable performance | Multi-turbine setup: Achieving higher suction performance involves combining multiple turbines, which adds to overall complexity |
Wide applicability: Suitable for a wide range of general food factory applications | |
Scalable performance: Available in multi-turbine configurations to increase suction | |
Adjustable speed: Can be combined with inverter control for variable motor speed |
Centrifugal Fan

A Centrifugal Fan is designed to move large volumes of air rather than generate maximum pressure. Instead of focusing on lifting heavier materials, it provides the airflow required to capture airborne/suspended dust efficiently.
This is why Centrifugal Fan Systems are used with Dust Extraction Units, suited to applications where maintaining high airflow is more important than producing high vacuum pressure. They are often combined with large filtration systems and automatic filter cleaning to support continuous operation.
Benefits | Limitations |
Fine dust extraction: Excellent for extracting fine airborne dust | Vacuum pressure: Generates lower vacuum pressure compared to turbine motors |
High airflow: Well suited to large or open working areas | Heavier debris and liquids: Better suited to airborne dust than heavier debris or liquids |
High-capacity filtration: Well suited to systems handling large filtration volumes | Larger installations: Continuous, high-volume applications generally call for larger system installations |
Automatic filter cleaning: Compatible with automatic filter cleaning systems |
Brushless Motor
A Brushless Motor eliminates the carbon brushes found in conventional electric motors, reducing wear while improving reliability and service life. The by-pass cooling design keeps the motor cooling air separate from the suction airflow, helping to protect the motor from dust contamination.
Brushless Motors provide strong suction performance in a compact design and are commonly used in portable industrial vacuum cleaners, including ATEX-certified models where reliability is particularly important.
Benefits | Limitations |
Longer service life: Lasts longer than conventional brushed motors | Electronic controls: More complex electronic controls can contribute to a higher purchase cost |
Reduced maintenance: Requires less upkeep due to the absence of brush wear | Duty range: Typically used on compact vacuums rather than the largest continuous systems |
Strong suction performance: Delivers strong suction in a compact design | |
Lightweight and portable: Suitable for lightweight and portable industrial vacuum cleaners | |
Safety-rated applications: Commonly used in ATEX and ACD environments |
Brush Motors
Single Brush Motor
A Single Brush Motor is the simplest motor configuration used in industrial vacuum cleaners. It consists of one brush-type electric motor with a cooling system that keeps the motor cooling air separate from the suction airflow.
This design provides a compact and economical solution for lighter-duty cleaning tasks where continuous operation is not required.
Benefits | Limitations |
Cost-effective solution: Well suited to general cleaning applications | Airflow and vacuum performance: Lower than other motor options |
Compact and lightweight: Offers a compact, lightweight design | Duty cycle: Not intended for heavy-duty or continuous industrial operation |
Lower power consumption: Uses less power than larger motor configurations | Material volume: Less suited to applications involving large volumes of material |
Intermittent use: Suitable for lighter-duty cleaning and intermittent operation |
Dual Brush Motor

A Dual Brush Motor uses two brush-type motors operating together to provide greater airflow and suction performance than a single-motor design. Similar systems are also available with three motors where additional performance is required.
This configuration provides a balance between performance and cost, making it suitable for a wide range of industrial cleaning applications involving dry dust, liquids and slurry.
Benefits | Limitations |
Higher suction performance: Delivers greater suction than a Single By-Pass Brush Motor | Duty cycle: Lower continuous-duty capability than Turbine Motors or Centrifugal Fan systems |
Cost-performance balance: Offers a good balance between cost and performance | Maintenance requirements: Additional motors increase maintenance requirements compared with a single-motor design |
Versatile collection: Suitable for collecting dust, liquids and slurry | Service life: Brush wear results in a shorter service life than Brushless By-Pass Motors |
Multi-motor configurations: Available in configurations with additional motors to increase performance |
Triple Brush Motor

A Triple Brush Motor combines three brush-type motors to push total airflow and vacuum performance beyond what a dual-motor setup can achieve, while still using single-phase by-pass motors rather than moving to a turbine or centrifugal fan system.
Benefits | Limitations |
Highest airflow/suction tier: Leads the by-pass motor configurations for airflow and suction | Component count: More motors mean more components that could wear or need maintenance compared to single or dual configurations |
Fine dust collection: Particularly associated with the collection of very fine dust, often paired with HEPA filtration and multi-filter setups | Service life: By-pass brush motors, even in a triple configuration, still generally have a shorter service life than brushless equivalents |
Automatic filter compatibility: Compatible with automatic, self-cleaning filter systems for continuous operation without suction interruption or operator intervention | Power draw: Higher power draw than single or dual setups, which may be a consideration for single-phase electrical supply limits |
Compact and manoeuvrable: Still benefits from the compactness and manoeuvrability typical of single-phase by-pass machines, despite the added power |
Venturi (Compressed Air Powered)
Venturi motorisation eliminates the motor altogether. It doesn’t have an impeller, bearings, or electrics. Instead, compressed air passes through a shaped nozzle inside a venturi tube, accelerating as the nozzle narrows. This high-velocity jet entrains the surrounding air, creating the depression that draws debris into the container.

Because Venturi motorisation doesn’t have any moving or heat-generating parts, the unit can run continuously with no duty cycle limit, typically delivering a service life of around 20,000 hours.
Also, the system doesn’t require an electrical ignition source, so it’s a natural fit for ATEX zoned areas, with certified models available for Zone 21 and Zone 22.

Selecting the most appropriate motor depends on how the vacuum cleaner will be used. Factors such as operating time, the type of material being collected, the required airflow and suction performance, and the level of maintenance should all be considered.
For any questions about the Klipspringer range of Industrial Vacuum Cleaners and Accessory Kits, contact us on 01473 461800 or sales@klipspringer.com. Alternatively, you can fill out the contact form below and we will be in touch.
If you would like to learn more about the Industrial Vacuum Cleaners mentioned throughout this article, share your contact details below.

What Are the Different Filter Options for Industrial Vacuum Cleaners?
Help Guide: Understanding the Different Filter Options for Industrial Vacuum Cleaners
The performance of an industrial vacuum cleaner depends on more than just the vacuum itself. The filter cleaning system and filter type both play a vital role in supporting efficient day-to-day cleaning.
This guide explains the different options available across the Klipspringer range, helping you to identify the most suitable solution for your application.
Why Filter Choice Matters
Choosing the right filter cleaning system and filter type for your application isn’t just a specification detail, it directly affects how well the vacuum performs and how long it lasts. There are two main reasons filter options to consider:
- Vacuum performance: the wrong filter type, or one that becomes blocked, reduces performance, limiting the depression (vacuum strength) and airflow the machine can generate.
- Motor protection: a blocked or poorly matched filter forces the motor to work harder to maintain suction. Over time this increases running costs, puts additional strain on the motor, and can ultimately result in costly motor repairs.
Matching the filter cleaning system and filter type to your dust type, volume, and how often the vacuum is used helps avoid these issues, keeping the vacuum running efficiently and protecting your investment.
Manual Shaking
Manual Shaking is the simplest filter cleaning system available. As dust collects on the surface of the filter, airflow and suction gradually reduce. To restore performance, the operator stops or pauses the vacuum and uses an external handle or lever to shake the filter, allowing the dust to fall into the collection container below.
This straightforward design makes Manual Shaking well suited to lighter-duty applications where the vacuum is used intermittently and dust volumes are relatively low.

Manual Shaking Lever
Benefits | Limitations |
Simple, cost-effective design: With no automated cleaning components, Manual Shaking systems are typically the most economical option. | Requires operator intervention: The filter must be cleaned manually to maintain suction performance. |
Easy to maintain: Fewer moving parts reduce maintenance requirements and simplify servicing. | Temporary interruption to cleaning: The vacuum must be stopped or paused while the filter is cleaned. |
Compact and lightweight: The uncomplicated design often results in a smaller, easier-to-handle vacuum cleaner. | Reduced suction between cleaning cycles: Airflow gradually decreases as dust accumulates on the filter. |
Well suited to intermittent use: An effective choice for routine cleaning where filters do not require frequent cleaning. | Less suitable for continuous operation: Frequent manual cleaning can reduce productivity in high-use environments. |
Not intended for heavy dust loads: Applications generating large volumes of fine dust are generally better suited to automated cleaning systems. |
Semi-Automatic Filter Cleaning
Semi-Automatic Filter Cleaning systems provide a more advanced method of filter cleaning than Manual Shaking, cleaning the filters without the operator having to manually shake it. There are two types used across the Klipspringer range, depending on the motor type:

Standard (Electric)
Used with brushed motors. The filter is mounted to electric solenoids which shake the filter to dislodge accumulated dust.
Pneumatic Piston
Used with turbine motors. The vacuum uses a reverse air valve which pushes air through a pneumatic piston, and this in turn shakes the filter to dislodge accumulated dust.
In both cases, this restores airflow quickly, helping to maintain consistent suction while reducing filter clogging and maintenance requirements. Vacuum cleaners with Semi-Automatic Filter Cleaning are suited to applications involving regular use, fine dust, or extended operating periods.
Benefits | Limitations |
Fast, effective filter cleaning: Mechanised cleaning removes accumulated dust more efficiently than manual shaking. | Operator activation required: The cleaning cycle must still be started manually. |
Maintains consistent suction: Regular filter cleaning helps preserve airflow throughout operation. | More complex design: Additional mechanical components increase system complexity. |
Reduces filter clogging: Dust is removed more effectively, extending the time between maintenance. | Higher purchase cost: Typically more expensive than Manual Shaking systems. |
Lower maintenance requirements: Operators spend less time cleaning filters and more time carrying out productive cleaning tasks. | Not fully automatic: Although cleaning is mechanised, it does not take place continuously during operation. |
Suitable for demanding applications: Well suited to frequent use and environments where fine dust is generated. |
Automatic Filter Cleaning
Automatic Filter Cleaning is designed for applications where uninterrupted performance is essential. Unlike Manual or Semi-Automatic systems, the filter is cleaned continuously while the vacuum remains in operation, maintaining airflow without stopping suction.
Every model in our Automatic range uses a combination of Micro Vibration Technology and Compressed Air Pulses to clean the filters without the requirements for an onboard compressor, a patented approach that is unique in the market and the flagship filter cleaning system in the Klipspringer collection.
These systems continuously remove dust from the filter surface, making them particularly suitable for demanding production environments and applications involving large volumes of fine dust.
How the System Works
- The turbine switches on, the vacuuming starts, and the automatic cleaning timer begins. The turbine stays on throughout the entire process.
- The timer runs on an adjustable 2-10 minute cycle. When it fires, the filters are cleaned one at a time while the other two continue vacuuming:
- Filter A: a solenoid seals it off from suction; it is cleaned for 4 seconds while Filters B and C keep vacuuming.
- Filter B: the same process runs 6 seconds later, while Filters A and C keep vacuuming.
- Filter C: the same process runs a further 6 seconds after that, while Filters A and B keep vacuuming.
- The filter is sealed into its own manifold by a solenoid, and the combination of micro-vibration and a compressed air pulse spreads evenly in all directions, cleaning the full length of the filter.
- All three filters are cleaned in rotation, and the vacuum can run continuously for as long as it is set by the timer regulator, with zero interruption to suction.
Benefits | Limitations |
Continuous suction performance: Filter cleaning takes place while the vacuum remains in operation. | More sophisticated system: Automatic cleaning mechanisms include additional components that require periodic maintenance. |
Maximum cleaning efficiency: Automatic cleaning helps to maintain consistent airflow and filtration performance. | Higher purchase cost: Typically the most expensive filter cleaning option. |
Ideal for continuous operation: Well suited to production environments where vacuums operate for extended periods. | May exceed application requirements: Simpler cleaning systems are often sufficient for occasional or lower-volume cleaning tasks. |
Handles high dust volumes: Designed for demanding applications involving large quantities of material. | |
No routine operator intervention: Reduces downtime and minimises operator involvement during normal operation. | |
Supports multi-cartridge filtration systems: Helps to maintain performance across larger filter surface areas. |
Filter Types
In addition to finding a filter cleaning system that is suited to your site and application, it is also important to consider the type of filter being used by your Industrial Vacuum Cleaner. Below are some of the key options included in the Klipspringer range.
Star Polyester Filter
Star Polyester Filters use a pleated, star-shaped design that maximises filtration surface area within a compact housing. They are commonly used for general industrial cleaning and are well suited to applications involving conventional dust and routine housekeeping.

Cartridge Filters
Cartridge Filters provide a larger filtration surface area than Star Polyester Filters, making them effective for collecting fine dust while maintaining airflow over longer operating periods. Multiple cartridges can be installed within the same vacuum to increase overall filtration capacity, making these systems well suited to higher-volume or continuous-duty applications.

Cartridge Filters (Class M)
Class M Cartridge Filters are designed for applications involving hazardous industrial dusts that require a higher level of filtration than standard filters. They are commonly supplied with conductive coatings to help dissipate static electricity and can be combined with HEPA filtration where even greater filtration efficiency is required.
HEPA Filters
HEPA Filters are installed as a secondary filtration stage rather than being used as the primary filter. They capture extremely fine dust particles that pass through the primary filter, significantly improving overall filtration efficiency. Depending on the model, HEPA filtration can achieve efficiencies of up to 99.995% for particles as small as 0.3 microns, making it suitable for applications involving fine powders or hazardous dusts.

Anti-Static and Conductive Filters
Antistatic and Conductive Filters are not a separate filter type, but a feature incorporated into primary filtration systems such as Star Polyester or Cartridge Filters. They are designed to safely dissipate static electricity, helping to reduce the risk of sparks in environments where combustible dust is present.

By considering how often your vacuum cleaner will be used, the type and volume of dust being collected, and the level of operator involvement required, you can select a filter cleaning system that delivers reliable performance while minimising maintenance and downtime. Choosing the appropriate filter type will also help to ensure effective dust capture.
For any questions about the Klipspringer range of Industrial Vacuum Cleaners and Accessory Kits, contact us on 01473461800 or sales@klipspringer.com. Alternatively, you can fill out the contact form below and we will be in touch.
If you would like to learn more about the Industrial Vacuum Cleaners mentioned throughout this article, share your contact details below.

WHITE PAPER: Hygiene Verification: Analysing an Alternative Approach to ATP
WHITEPAPER
Hygiene Verification: Analysing an Alternative Approach to ATP
Effective hygiene verification is vital for food safety, compliance, and brand protection. ATP testing is common but doesn’t always tell the full story.
This white paper explores the A3 system, which detects more organic residues than ATP alone, backed by research and case studies, offering practical insights for cleaning validation.


Why Clean-in-Place (CIP) Isn't the Whole Hygiene Picture for Food Production Sites
Learn how Clean-in-Place (CIP) systems work and why manual cleaning remains essential.
Clean-in-Place (CIP) is an essential part of food manufacturing, providing a reliable and efficient way to clean processing equipment without the need for dismantling.
However, an effective CIP system involves more than simply running a cleaning cycle. To achieve consistent hygiene standards, manufacturers must understand how CIP works, how cleaning effectiveness is verified, and where the limits of the process sit.
In this guide, we’ll explore the key principles behind Clean-in-Place systems, including the importance of validation, hygienic design, and manual cleaning controls.
What is Clean-in-Place (CIP)?
Clean-in-Place (CIP) is the standard method for cleaning the inside of tanks, pipework, valves, and other processing equipment without the need for dismantling. Instead of taking equipment apart, cleaning and sanitising solutions are circulated through the system in a controlled sequence, helping to remove product residues and maintain hygienic production conditions.
A typical CIP cycle includes several stages:
- A pre-rinse to remove loose product residues.
- A hot alkaline (caustic) wash to break down fats and proteins.
- An intermediate rinse to flush away the cleaning solution.
- An acid wash, where required, to remove mineral deposits and scale.
- A final rinse.
- A sanitising step before production resumes.

Time
How long the cleaning solution remains in contact with the equipment.

Action
The mechanical cleaning effect created by the flow of the solution.

Chemistry
The type and concentration of the cleaning chemicals.

Temperature
The heat of the cleaning solution.
What is TACT?
The effectiveness of a Clean-in-Place (CIP) system is determined by four key factors, commonly known as TACT:
- Time: how long the cleaning solution remains in contact with the equipment.
- Action: the mechanical cleaning effect created by the flow of the solution.
- Chemistry: the type and concentration of the cleaning chemicals.
- Temperature: the heat of the cleaning solution.
These factors work together. If one is reduced, such as cleaning time, another may need to be increased to achieve the same cleaning performance.
A validated CIP programme is designed to establish the right balance for each process, taking into account both the equipment being cleaned and the type of residue being removed.
How do you know your Clean-in-Place (CIP) Process has worked?
Most food manufacturers monitor CIP performance by reviewing cycle data such as time, temperature, conductivity, and flow. Many also use ATP testing or visual inspections before production resumes.
While these methods are valuable, they answer different questions. A validated CIP cycle confirms the cleaning process ran as intended, while ATP testing indicates the presence of general organic residue. Neither is designed to detect specific allergen proteins or individual pathogens.

ATP testing also has recognised limitations. During processes such as cooking, heating and fermentation, ATP naturally breaks down into molecules (ADP + AMP) that standard ATP tests cannot detect. As a result, a surface may pass an ATP test while still carrying residual organic material.
Similarly, a satisfactory ATP result does not necessarily mean allergen proteins have been removed. Trace allergen residues may remain below the test’s detection threshold while still posing a risk to the next production run.
The Importance of Hygienic Design
Even the best cleaning programme cannot overcome poor equipment design. Areas such as dead legs, hard-to-reach surfaces, poor drainage points, and hidden crevices can allow product residues and microorganisms to remain after cleaning.
This means CIP performance is not only determined by cleaning parameters such as time, temperature, chemistry, and flow. The design of the equipment itself plays a critical role.

By selecting equipment with hygienic design principles in mind manufacturers can improve cleaning reliability and reduce the risk of contamination. This includes:
- Smooth surfaces
- Effective drainage
- Avoiding equipment with areas/components that are difficult to clean
Where Clean-in-Place (CIP) ends and Manual Cleaning begins
A validated Clean-in-Place (CIP) process is a critical element of food safety, but it is only effective within its defined scope. Understanding the boundaries of CIP is essential to ensure that all areas requiring cleaning are identified and appropriately controlled.
CIP is designed to clean internal product-contact surfaces within equipment, including tanks, pipework, valves, and pumps. However, it does not replace the need for manual cleaning of areas that fall outside the automated process.


Equipment exteriors, floors, drains, changeover tools, and other manually cleaned components require separate cleaning procedures. If these areas are assumed to be covered by CIP, gaps in hygiene controls can occur, increasing the risk of contamination.
Manual cleaning should therefore be treated as an integral part of the overall hygiene programme. By clearly defining responsibilities, cleaning methods, and verification requirements, manufacturers can ensure that both CIP and manual cleaning activities work together to maintain effective hygiene standards across the site.
Managing Manual Cleaning Controls
If manual cleaning is required, segregation and traceability become critical. Equipment used in an allergen-controlled area, for example, may create a food safety risk if it is moved into another production zone without appropriate controls in place.
Visual controls play an important role in ensuring manual cleaning tasks are clearly understood and consistently completed. Colour-coded cleaning tools and shadow board storage systems make it immediately clear where equipment belongs and its intended application. This helps to prevent incorrect use, supports segregation, and reduces the risk of cross-contamination.

Cleaning Instruction Cards should also be used to provide clear guidance on cleaning requirements. These should include photographs and step-by-step instructions that define what needs to be cleaned, the correct cleaning method, and which areas fall within or outside the CIP process.
It is also important to identify areas that are frequently missed or present particular cleaning challenges. To drive continuous improvement, Visual Management Signs can be introduced to highlight best-practice examples, cleaning steps, and key responsibilities.
When CIP and manual cleaning controls work together, food manufacturers can create a more reliable cleaning process that supports food safety, operational efficiency, and audit compliance.
If you have any questions about the guidance or solutions mentioned throughout this article, you are welcome to contact our team on 01473461800 or sales@klipspringer.com. Alternatively, you can share your details via the form below and we will be in touch.
If you have any questions about the guidance or solutions mentioned throughout this article, please share your contact details below.

Sustainability Regulations Reshaping Cleaning and Hygiene Products: What Food Production Sites Need to Know
A guide to the sustainability rules reshaping cleaning and hygiene products, and what they mean for your food production site.
The sanitisers, disinfectants and cleaning chemicals used at your food production site are made from ingredients that are coming under stricter regulation across the UK and EU.
If these ingredients become restricted, reformulated or discontinued, the effects will reach your site. You could face new ingredient lists, price increases or reduced availability of the cleaning and hygiene products you rely on.
This guide explains the key changes ahead, from chemical restrictions and packaging reform to carbon reporting and greenwashing.
Chemical Review: PFAS and Microplastics
Regulators across the UK and EU are reviewing a wide range of chemicals used in cleaning and hygiene products, with particular focus on PFAS, a group of persistent chemicals used in some surfactants and performance ingredients, and microplastics, which can be found in ingredients such as encapsulated fragrances.

What this means for your site:
Some cleaning and disinfecting products may be reformulated, discontinued or replaced over the next few years. Speak to your suppliers now to understand their plans and identify suitable alternatives, rather than waiting until a product is no longer available.
Biocidal Product Approvals Are Slowing
During the pandemic, approvals for biocidal products were fast tracked to help keep disinfectants available. That flexibility is now being scaled back under both the EU Biocidal Products Regulation (BPR) and GB BPR, with active substances undergoing re-evaluation, stricter environmental risk assessments and longer authorisation timelines.

What this means for your site:
Disinfectants used as part of your food safety programme may face longer approval times or require reformulation. Build this into your supplier review process now, rather than waiting until product availability becomes an issue.
Packaging Rules Are Getting a Lot Stricter
Requirements for the UK
The new Extended Producer Responsibility (EPR) rules mean businesses will now pay fees based on how recyclable their packaging is, with much more detailed reporting required.
The existing Plastic Packaging Tax will also continue to apply to plastic packaging containing less than 30% recycled content.
Requirements for the EU
The Packaging and Waste Regulation (PPWR) takes things a step further. It will introduce mandatory recycled content targets for plastic packaging components, encourage the use of single-material packaging designs and set targets such as 100% reusable packaging for business-to-business transport by 2030.

What this means for your site:
Review your current packaging materials and speak with suppliers about upcoming changes. Understanding where your packaging may need to be redesigned, replaced or reported differently will help you to avoid unexpected costs and compliance issues.
Carbon Reporting Is Reaching Further Down the Supply Chain
Large EU companies are now required to report their Scope 3 emissions under the Corporate Sustainability Reporting Directive (CSRD). This includes emissions generated throughout their supply chain, not just from their own operations.
As a result, smaller UK food producers, including those that do not sell directly into the EU, may increasingly be asked by customers and supply chain partners to provide carbon emissions data.

What this means for your site:
Start collecting basic carbon and sustainability data now, even if no one has asked for it yet. Taking a proactive approach will make it easier to respond if customers begin requesting this information.
Wastewater Standards Are Tightening
If your site uses clean in place (CIP) systems or discharges wastewater, the standards governing what can be released into the drain are becoming stricter. For manufacturers supplying industrial and institutional cleaning products, there is increasing focus on how quickly cleaning chemicals biodegrade and their impact on aquatic life.

What this means for your site:
Ask your cleaning chemical suppliers whether their products meet the latest biodegradability and aquatic toxicity requirements. It’s also worth reviewing any clean in place or wastewater discharge processes that could be affected as standards continue to evolve.
Green Claims Are Under Increased Scrutiny
Both the UK and EU are cracking down on greenwashing, where products or operations are presented as more environmentally friendly than they really are.
Requirements for the UK
The Green Claims Code, introduced by the Competition and Markets Authority, has applied since April 2025, with fines of up to 10% of global turnover for misleading environmental claims.
Requirements for the EU
The Empowering Consumers for the Green Transition Directive must be implemented by member states by March 2026, followed by a six-month period before the new rules apply.
The Directive bans vague claims such as “environmentally friendly”, carbon neutrality claims based solely on offsetting, and sustainability labels that are not supported by approved certification.

What this means for your site:
Review the sustainability claims on your packaging, website and marketing materials to make sure they are accurate, specific and supported by evidence.
Practical Steps for Food Producers
- Ask your cleaning and hygiene suppliers whether their products contain PFAS or other substances under regulatory review.
- Confirm supplier timelines for the reformulation and reapproval of key disinfectants.
- Review your packaging against upcoming UK and EU recycled content requirements.
- Start collecting carbon and emissions data, even if customers have not requested it yet.
- Check that the sustainability claims on your packaging and marketing materials are accurate and supported by evidence.
- Discuss these changes with your procurement and compliance teams now, rather than reacting when a product is discontinued or a new fee is introduced.
How Klipspringer Can Help
We work closely with our customers to understand their sustainability commitments and support their Scope 3 ambitions. There are several areas of our range to consider, including:

- A trade-in scheme that lets you upgrade ageing instruments without adding to landfill, all while making a saving on new equipment.
- SegriCovers: a heavy-duty, reusable alternative to single-use plastic film for equipment protection during washdowns and deep cleans.
- Cloud-based quality management systems: helping sites move away from paper-based checks and cut unnecessary waste.
- Recycled and sustainably sourced equipment across parts of our product range, developed to reduce environmental impact without compromising on food safety standards.
We’re also a member of Sedex, the ethical trading platform, and hold ourselves to the same standards we help our customers meet. If you’re reviewing your suppliers as part of your sustainability planning, get in touch with our team to find out more.
Regulatory changes are moving fast, but if you start talking to your suppliers now and keep track of the right information, you won’t be caught out.
For any questions about the updates mentioned throughout this article or the sustainability solutions provided by Klipspringer, contact us on 01473461800 or sales@klipspringer.com. Alternatively, you can fill out the contact form below and we will be in touch.
If you would like to learn more about the products and solutions mentioned throughout this article, share your contact details below.

BRCGS Storage and Distribution Issue 4: Review of 2026 Position Statements
Your Guide to the BRCGS 2026 Position Statements for Storage and Distribution
BRCGS regularly publishes position statements to clarify how clauses within its Global Standards should be interpreted and applied.
Since the beginning of 2026, several new position statements have been released for sites certificated to the BRCGS Global Standard for Storage and Distribution Issue 4.
In this guide, we take a closer look at three key changes, before providing a summary of the remaining 2026 position statements.
Position Statement 17: Equipment Storage
Clause 6.1 has been amended to state that equipment must be used “and stored to” minimise the risk of damage or contamination. While this may appear to be a small amendment, it places greater emphasis on how equipment is treated between use, not simply how it is designed or maintained.
According to the update, equipment should be stored in a way that prevents it from becoming a source of contamination or harbouring pests. The position statement also highlights the importance of keeping movable equipment within designated areas.


Securing Compliance with Shadow Boards
For sites reviewing how their equipment is stored, shadow boards offer a practical way to meet this requirement. By giving each tool a dedicated home, shadow boards keep items off the floor, separated from one another, and stored in a clean, hygienic manner.
Shadow boards can also be colour-coded or customised with bespoke headings to support existing segregation systems.
Finally, bringing equipment storage into highly visible locations makes it easier to identify missing or damaged utensils during routine inspections, before they create a larger issue.
Position Statement 18: Cleaning Equipment
Clause 6.4.5 has been updated to clarify the requirements for cleaning equipment, it must now be:
- hygienically designed and fit for purpose
- suitably identified for its intended use, for example through colour-coding or labelling
- cleaned and stored in a hygienic manner to prevent contamination
As discussed in the previous section, dedicated shadow boards support the safe and hygienic storage of cleaning equipment.
The revised clause also places greater emphasis on equipment design and clear identification.

Securing Compliance with Colour-Coded Equipment
Colour-coding is a simple yet effective way to ensure equipment is clearly identifiable and segregated by area or task, helping to minimise the risk of cross-contamination. A wide range of hygienically designed cleaning and production equipment is available in different colours, making it easy to implement a colour-coding system tailored to the specific requirements of your site.
Another option to consider is Indelimarking, a laser-engraving technique that permanently marks equipment without creating crevices or harbourage points where contaminants can build. Unlike printed or adhesive labels, Indelimarking will not fade or lift over time, providing a durable and hygienic method of equipment identification.
Position Statement 20: Process Monitoring
Clause 17.3 has been amended to clarify that processes must be monitored using appropriate process parameters. These parameters should be recorded using suitable monitoring equipment linked to an automatic alarm system or, if automatic monitoring is not available, through documented manual checks.
The update makes it clear that alarm settings must be appropriate for the process being monitored and that monitoring records must be retained for a minimum of the product shelf life plus one year, as they may be required to support a due diligence defence.
Where manual monitoring is used, checks must continue during non-working periods, including weekends and public holidays. The frequency of these checks should be determined by the product’s sensitivity to temperature variation and the associated risks.

Securing Compliance with a Real-Time Monitoring System
Real-time monitoring systems are well suited to meeting this requirement, particularly for sites managing multiple areas that are temperature-controlled.
The WatchmanOne Real-Time Monitoring System tracks key parameters, including temperature, humidity, and door contact, and sends automatic alerts by SMS or email to pre-selected contacts if a reading falls outside the expected range.
This kind of continuous monitoring reduces reliance on manual checks and helps to ensure records are complete and easy to access should they be needed for an audit. It also resolves the issue of monitoring processes during non-working periods.
Overview of the remaining 2026 Position Statements
Position Statement 12 – Clause 1.3.2: Personnel responsibilities
Personnel must understand their responsibilities, be able to demonstrate that their work follows documented site procedures, and must have access to the relevant documentation.
Position Statement 13 – Clause 2.1: Prerequisite programmes
Prerequisite programmes must be established, documented and verified where appropriate before HARA or HACCP risk analysis is carried out, and included in the development and review of the plan.
Position Statement 14 – Clauses 3.5.1.2 and 3.5.2.1: Suppliers and subcontractors
Specifications or contracts must clearly define the service being provided, along with relevant product-safety, quality, legality, handling and technical requirements.
Position Statement 15 – Clause 3.5.3.1: Product-fraud vulnerability assessments
Personnel carrying out vulnerability assessments must have suitable knowledge of product-fraud risks and vulnerability-assessment principles.
Position Statement 16 – Clause 4.2.1: Product security and defence
Personnel undertaking threat assessments and developing product-defence plans must be appropriately competent.
Position Statement 19 – Section 17: Contract processing
Irradiation has been added to the list of contract-processing activities covered by Section 17, alongside chilling, freezing, tempering, defrosting and high-pressure processing.
The position statements referenced throughout this article will take effect for audits commencing 10th August 2026. So, now is the perfect time to review your current practices against the updated clauses, particularly around equipment design and identification, the storage of your utensils, and process monitoring.
If you have any questions about the position statements above or would like to discuss the solutions referenced throughout this article, you can contact us on 01473 461 800 or email sales@klipspringer.com. Alternatively, complete the contact form below.
If you would like to learn more about the products and solutions mentioned throughout this article, share your contact details below.

The Benefits of Visual Management for Multi-Site Food Production Groups
Five benefits of a standardised approach to visual management across multi-site groups
Visual management uses boards, signage, and colour-coding to communicate key information across your food production site, helping teams understand what is required at a glance.
In multi-site food production groups, it plays an important role in maintaining consistency. Without a standardised approach, sites can develop their own ways of displaying information, making it harder to compare performance, maintain standards and roll out changes across the business.
The following guide explores five key benefits of implementing a standardised visual management system across your food production group.
1. Standardise Food Safety Across Every Site

If each production site within your group uses different boards, signage and visual systems, it will be much harder to maintain consistent standards across the business.
For example, one factory may display Critical Control Point (CCP) information on production boards, while another may store the same information in folders or communicate it in a completely different way. Likewise, colours, symbols and layouts can vary between sites, making it harder for employees and managers to understand information when moving between locations.
Introducing a standardised visual management system helps to ensure important information is displayed consistently throughout your organisation. Although each factory may require its own site-specific content, using the same layouts, formats and visual principles makes it easier for every team to work towards the same food safety and quality standards.
2. Strengthen Performance Monitoring Across Your Group
Monitoring performance across multiple production sites can quickly become a time-consuming task if every location records and displays information differently.
Without a consistent approach, group-level managers often need to interpret data from a variety of formats before meaningful comparisons can be made. This slows decision-making and makes it more difficult to identify trends or share successful ways of working.

Using standardised KPI, SQCDP, and SIC boards across every site makes performance much easier to review. When the same information is presented in the same format, managers can compare sites more effectively, identify opportunities for improvement and share best practice across the wider business.
3. Improve Audit Readiness
Preparing multiple production sites for customer, third-party and regulatory audits can be challenging when each location follows different visual standards.
Auditors expect to see clear evidence that food safety procedures are being followed consistently. If information is presented differently from site to site, demonstrating compliance across your organisation becomes more difficult and can create unnecessary questions during the audit.

Standardised visual management helps to establish a consistent approach throughout your business. From production boards and hygiene signage to CCP displays and quality information, auditors can quickly understand how each site operates and see that the same standards are being applied across your entire production group.
4. Simplify Staff Training and Site Transfers
Many food production groups regularly move employees between sites to cover holidays, support periods of increased demand or provide development opportunities.
However, if every site communicates information differently, experienced employees can still require additional training before they are able to work confidently in their new location.

A consistent visual management system helps to reduce this learning curve. When production boards, colour-coding, signage and workplace information follow the same structure across every site, employees can quickly familiarise themselves with their surroundings and begin working safely and effectively with minimal additional support.
5. Save Time When Rolling Out Changes

Introducing changes across multiple production sites can be a complex and time-consuming process, particularly if every factory uses different visual management systems.
Whether you’re launching a new product, introducing a customer-specific requirement, responding to an audit non-conformance or updating an internal procedure, each site may require different boards, signage and documentation to be redesigned before the change can be implemented.
A standardised visual management system removes much of this unnecessary work. By using the same layouts, formats and design principles across every site, changes can be introduced quickly and consistently throughout your organisation.
This not only reduces the time and resources needed to update your visual management system, but also helps ensure every site receives the same information at the same time. As a result, your business can respond more quickly to customer requirements, audit findings and operational improvements without creating different solutions for every factory.

Visual Management Inspiration Guide
From KPI Boards to Shift Management Planners, there are over 70 designs to explore in our Inspiration Guide.
Group-Wide Visual Management Solutions
Klipspringer works with multi-site food groups to implement visual management systems that support consistency, compliance and operational efficiency.
Whether you’re introducing visual management for the first time or looking to standardise existing systems, our visual management solutions can be customised to reflect the specific requirements of your organisation. The range includes:
- SQCDP, KPI and production performance boards.
- CCP, hygiene and food safety signage.
- Training, communication and shift management boards.
- Equipment shadow boards and storage solutions.
- Washroom and hygiene station signage, including customised mirrors.
By adopting a unified approach to visual management, you can reduce the time and resources spent maintaining different systems, improve communication across your production group and speed up response times to new customer requirements, audit findings and operational improvements.
If you have any questions about Visual Management Solutions or would like to discuss your requirements, you can contact us on 01473 461 800 or email sales@klipspringer.com. Alternatively, you can complete the form below and a member of our team will be in touch.
If you would like to learn more about Visual Management Solutions, share your details below.

Washroom Best Practice for Food Manufacturers: Improving Hygiene, Organisation and Efficiency
The Ultimate Guide to Washroom Best Practice in the Food Industry
The washroom is one of the busiest and most demanding areas of any food production site. Hygiene Teams are responsible for cleaning equipment quickly and effectively while maintaining the highest standards of food safety. With tight production schedules and large volumes of equipment to manage, keeping the washroom organised isn’t always easy.
With this in mind, we’ve created a guide to washroom best practice. It explores some of the common challenges faced during washdowns and highlights practical ways to improve segregation, protect equipment, and increase operational efficiency.
Equipment Segregation in Food Factory Washrooms
Most food production sites work hard to maintain equipment segregation on the factory floor. Colour-coding, designated storage locations and documented procedures all help to reduce the risk of cross-contamination. However, one stage that can often be overlooked is the washroom.
When multiple sets of equipment are cleaned at the same time, it is easy for tools from different production areas to mix together. Equipment may be placed on the nearest hook, shared rail or even temporarily on the floor while operators focus on completing the clean as quickly as possible.
Maintaining segregation throughout every stage of the cleaning process helps to reduce the risk of cross-contamination. It also makes it much easier to identify missing equipment and ensures that tools are returned to the correct production area once cleaning has been completed.
How to Improve Equipment Segregation
Providing dedicated storage within the washroom is a simple way to reinforce existing segregation procedures.
Washroom Equipment Storage Boards give Hygiene Teams a clearly defined place to hang equipment while it is being cleaned and dried. Boards can be dedicated to specific production areas, equipment types or colour-coded systems, helping to maintain segregation throughout the washdown process.
Keeping equipment organised also improves visibility. When every item has its own position, missing equipment is easier to identify and less likely to be misplaced or accidentally transferred between production areas.

Equipment Damage in Food Factory Washrooms
During washdowns, tools are exposed to cleaning chemicals, high-pressure water and constant handling. In busy periods, equipment can easily become piled together, knocked against hard surfaces or dropped while being moved around the washroom. Over time, this can lead to unnecessary wear, damage, and avoidable replacement costs.
Regular inspections before and after cleaning remain an essential part of any food safety system. However, preventing avoidable damage in the first place provides another layer of protection.
How to Reduce Equipment Damage
Storing equipment correctly throughout the washdown process helps to minimise unnecessary wear and tear.
Rather than leaving tools resting against walls, stacked together or placed on the floor, Washroom Equipment Storage Boards provide individual hanging positions that keep equipment secure while cleaning and drying takes place.
This not only helps to protect equipment from accidental damage, but also makes visual inspections quicker and easier before items are returned to production.

Operational Efficiency in Food Factory Washrooms
Washdowns are often carried out against tight schedules, with Hygiene Teams under pressure to return equipment to production as quickly as possible. Every minute spent searching for utensils, untangling tools or deciding where items should be stored adds to production downtime.
A well-organised washroom supports a smoother workflow. Equipment can be cleaned, inspected and dried in a logical sequence, reducing unnecessary handling and helping teams to prepare everything for production more efficiently.
Improving organisation in the washroom helps Hygiene Teams to work efficiently without compromising food safety or hygiene standards.
How to Reduce Equipment Damage
Providing designated storage for equipment helps to streamline the entire washdown process. Washroom Equipment Storage Boards create a clear, visual storage system where every item has a dedicated location. This makes equipment easier to find before, during and after cleaning, while helping teams quickly identify when something is missing or stored incorrectly.
By reducing unnecessary movement and improving organisation, Washroom Equipment Storage Boards help Hygiene Teams to minimise production downtime, ensuring equipment is ready for use when it is needed.
Washroom Equipment Storage Boards
Designed specifically for harsh washdown environments, Washroom Equipment Storage Boards help food manufacturers improve organisation throughout the cleaning process.
Suitable for production equipment and hygiene tools alike, they support colour-coded segregation, protect equipment from unnecessary damage and provide clear visual management within the washroom. Key benefits include:

- Purpose-built for harsh washdown environments.
- Supports colour-coded equipment segregation.
- Keeps equipment organised and off the factory floor.
- Helps reduce equipment loss and replacement costs.
- Protects equipment during cleaning and drying.
- Improves operational efficiency to help reduce downtime.
- Customise with bespoke layouts, messaging and company branding.
That brings us to the end of our guide to washroom best practice. We hope it has provided some practical ideas for improving organisation, maintaining segregation and protecting equipment during washdowns.
If you have any questions about Washroom Equipment Storage Boards or would like to discuss how they could be customised for your site, our team would be happy to help. Contact us on 01473 461 800 or email sales@klipspringer.com. Alternatively, complete the form below.
If you would like to learn more about Washroom Equipment Storage Boards in general, share your contact details below.

WatchmanOne and SenseAnywhere Calibrations: Understanding Your Options
Which Calibration Option Is Right for Your WatchmanOne or SenseAnywhere System?
The WatchmanOne System and SenseAnywhere System are widely used real-time monitoring solutions that help food production sites to maintain product quality, meet regulatory requirements, and reduce operational risks.
Through continuous monitoring, automated alerts, and secure data capture, these systems provide the visibility and traceability needed to support effective quality management.
For sites using either system, there are several calibration options available. This article provides guidance to help you select the most appropriate approach for your site.
How Often Should WatchmanOne and SenseAnywhere Systems Be Calibrated?
The most appropriate approach will depend on your site’s audit requirements, the level of risk associated with the process being monitored, and the value of the stock being protected.
For some sites, the system may be used simply for temperature and humidity monitoring to support quality records or data collection. If there is no direct food safety risk, calibration may be required less frequently, or sites may choose to carry out internal verification checks every few years.
However, for high-care factories or storage facilities with high-value stock at risk, annual calibration is strongly recommended, even if it is not a specific audit requirement.
Option 1: On-Site Calibration (Engineer Visit)
With on-site calibration, a qualified Klipspringer engineer visits your facility and calibrates your sensors in their installed location. This approach provides a convenient solution that ensures audit-readiness without disrupting your operations.
Best for: High risk environments, minimal disruptions, audit-critical operations.
| Key Benefits | Considerations | Typical Use Cases | Costs |
|---|---|---|---|
|
|
|
£120-£170 per sensor. |
Option 2: Calibrated Reference Checks
This approach involves using a calibrated reference sensor to verify the accuracy of your monitoring probes. Instead of removing equipment or arranging a site visit, your team can complete checks internally by comparing readings from the reference device against those from the sensors. This is a cost-effective calibration option that reduces disruption to your operations.
Best for: Sites with robust internal processes that require flexibility and a cost-effective approach.
| Key Benefits | Considerations | Typical Use Cases | Costs |
|---|---|---|---|
|
|
|
|
Option 3: Return to Klipspringer Laboratory for Calibration
This method involves returning sensors to Klipspringer for calibration, typically in batches. Sensors are calibrated in a UKAS-controlled laboratory environment, allowing testing at multiple temperature points. This approach ensures you have easy access to certification records and is a cost-effective option, particularly for larger operations.
Best for: Planned equipment rotation and sites requiring high-accuracy UKAS calibration, with multi-point testing completed in a controlled laboratory environment rather than ambient on-site conditions.
| Key Benefits | Considerations | Typical Use Cases | Costs |
|---|---|---|---|
|
|
|
|
Option 4: Hybrid Approach
- On-Site Calibration (Engineer Visit): used for critical sensors.
- Calibrated Reference Checks: completed throughout the year.
- Return to Klipspringer Laboratory for Calibration: used for non-critical, spare equipment or reference SenseAnywhere / WatchmanOne sensors.
Ultimately, the best calibration strategy is the one that reflects the needs of your site, helping you to maintain accurate monitoring, meet audit expectations, and keep operations running smoothly.
If you would like to learn more about SenseAnywhere, WatchmanOne, or Klipspringer’s Calibration Services, contact our team on 01473 461 800 or email sales@klipspringer.com. Alternatively, complete the form below.
If you would like to learn more about SenseAnywhere, WatchmanOne, or Klipspringer’s Calibration Services, share your contact details below.

Trial to Standardisation: How to Adopt New Hygiene Solutions
A Practical Guide to Hygiene Equipment Trials and Standardisation in Food Factories
Whether you are introducing a new cleaning tool, hygiene monitoring system or colour-coding policy, a successful outcome depends on more than the equipment itself.
Effective trials help sites to evaluate performance and make informed decisions before standardising new ways of working.
If you are considering an equipment trial and want to maximise its chances of success, this article will guide you through the process.
Setting Up Your Equipment Trial
Most equipment trials begin with a specific challenge. Whether the objective is to improve cleaning validation, increase efficiency, strengthen safety controls, or reduce the risk of cross-contamination, understanding the problem you are trying to solve is an important first step.

The examples below highlight some of the common reasons sites choose to trial different types of equipment and the outcomes they are looking to achieve.
Example 1: Trialling the A3 Hygiene Monitoring System
A3 trials are often driven by a lack of confidence in a site’s cleaning validation methods. While ATP testing is widely used to verify cleanliness, it can have limitations in food manufacturing environments. This is because ATP degrades to ADP and AMP during common processes like heating, cooking, fermentation, and even cleaning.
By measuring ATP, ADP and AMP, the A3 System provides a more complete picture of surface cleanliness. Trials are typically carried out to compare A3 against existing validation methods and assess whether the additional data can improve cleaning verification, strengthen hygiene controls, and provide greater confidence in cleaning effectiveness.
Example 2: Trialling Industrial Vacuums
Industrial vacuum trials are commonly introduced to improve cleaning efficiency or address safety concerns associated with existing cleaning methods.
In some cases, teams may be spending excessive time removing dust, debris, or product residue. In others, sites handling powdered ingredients such as flour may be looking to reduce the risks associated with airborne combustible dust and improve compliance with ATEX requirements. Trials help to determine whether a vacuum system can improve cleaning performance, reduce labour requirements, and provide a safer, more controlled approach to dust management.
Example 3: Trialling Double Blade Squeegees
Double blade squeegee trials are usually focused on improving cleaning performance and reducing the time it takes to remove water and debris from production areas.
If standing water remains after cleaning or multiple passes are required to achieve the desired result, cleaning can become both time-consuming and inefficient. Trials allow teams to evaluate whether double blade designs can improve liquid removal and reduce cleaning times by removing water and debris in a single pass.
Trials also provide an opportunity to assess how easy it is to clean the new equipment. This is often a key consideration when evaluating squeegee performance. Hygienically designed double blade squeegees can help to address these concerns through smooth, moulded construction and minimal crevices.
Example 4: Trialling Colour-Coded Equipment
Colour-coded equipment trials are typically undertaken to improve segregation and strengthen controls around cross-contamination risks.
Trials are often centred around introducing a more structured colour-coding system, making it easier for teams to identify the correct equipment, follow established procedures, and maintain consistency across departments and shifts.
By evaluating the system in a controlled way, sites can assess how effectively colour coding supports operational standards before implementing it more widely.
Running Your Equipment Trial
Once a trial has been set up, the next step is ensuring it is carried out in a way that produces clear, meaningful results. After all, a trial that is not properly managed can lead to mixed feedback, inconsistent use, and ultimately no clear conclusion.

The examples below highlight how different types of trials are typically run on site, and the factors that influence whether they deliver successful outcomes.
Example 1: Trialling the A3 Hygiene Monitoring System
A3 trials are most effective when run alongside existing validation methods rather than in isolation. This allows teams to compare results directly and understand how the system performs under real production conditions.
In practice, this often involves testing the same surfaces with both ATP and A3 swabs over a defined period. The side-by-side comparison helps to identify where results differ and assess whether ATP, ADP and AMP detection provides a more complete indication of cleanliness.
Consistency is important throughout the trial. Using the same test points, timings, and procedures helps to ensure results can be compared accurately. It is also important to establish clear benchmarks from the outset.
Example 2: Trialling Industrial Vacuums
Industrial vacuum trials are typically carried out as part of normal cleaning routines, focusing on areas where existing methods are least effective.
This may include zones where dust or debris are difficult to remove, or where traditional cleaning methods require significant time and effort. In environments handling powders, trials may also focus on ensuring dust can be removed in line with ATEX requirements.
During the trial, attention is usually placed on real-world performance. This includes assessing how quickly material can be removed, how easy the equipment is to handle, and whether the available attachments allow teams to clean hard-to-reach or high-level areas effectively.
Example 3: Trialling Double Blade Squeegees
In most cases, the double blade squeegee is compared directly against existing floor cleaning equipment, with attention focused on how effectively water and debris are removed. Particular emphasis is often placed on whether floors can be cleared in a single pass.
This can have a significant impact on cleaning efficiency, particularly in larger production areas where reducing cleaning time can help to shorten hygiene windows and improve operational efficiency.
Ease of cleaning is also an important consideration during the trial. Hygienically designed double blade squeegees with smooth surfaces and minimal crevices can be easier to clean and inspect, helping to support consistent hygiene standards.
Example 4: Trialling Colour-Coded Equipment
Colour-coded equipment trials typically involve assigning specific colours to designated areas, processes, or allergens and monitoring how consistently the system is followed over a defined period. The aim is to assess whether colour coding improves segregation, increases clarity, and reduces the risk of equipment being used incorrectly.
During the trial, teams can evaluate how intuitive the system is in practice and identify opportunities to strengthen compliance. This may include introducing colour-coded shadow boards with bespoke messaging and visual instructions.
Consistency across shifts is also an important consideration. For a colour-coding system to be effective, it must be understood and applied consistently by all teams, helping to maintain standards and reduce the risk of cross-contamination.
Rolling Out to Standardisation
Once a trial has been completed and the results are understood, the next step is deciding how to implement the solution. Successful roll out should focus on introducing a clear approach as early as possible, as using different methods for too long can create confusion.

The examples below highlight how different types of equipment are typically rolled out following a successful trial, plus the factors that influence whether they become part of standard site practice.
Example 1: Rolling Out the A3 Hygiene Monitoring System
Following a successful A3 trial, the focus shifts to integrating the system into existing hygiene verification programmes. This typically involves reviewing Cleaning Instruction Cards (CICs), cleaning validation procedures, environmental monitoring programmes, and allergen control plans to determine where A3 testing should be incorporated.
It is also important to establish clear action limits and response procedures so the additional information provided by ATP, ADP and AMP testing can be used consistently. Teams should understand not only how to carry out testing, but also how to interpret results and respond when limits are exceeded.
Training forms an important part of the rollout process. Operators, hygiene teams, and supervisors should be confident in using the system and recording results correctly. Ongoing support from Klipspringer’s Technical Team can help sites justify benchmark levels, update documentation, and demonstrate the effectiveness of the new approach during audits.
Example 2: Rolling Out Industrial Vacuums
Once proven effective, industrial vacuums should be incorporated into routine cleaning procedures and reflected within relevant CICs.
Training should focus on safe operation and correct use. It is also important to highlight the reasons for the change, whether that’s to improve cleaning efficiency, enhance dust control, or support ATEX compliance.
Dedicated storage solutions, such as shadow boards with clear instructions, will help to ensure equipment remains accessible, organised, and is consistently returned after use.
Example 3: Rolling Out Double Blade Squeegees
Following a successful trial, double blade squeegees should be introduced into areas where they provide the greatest operational benefit.
Cleaning procedures and CICs should be updated to define where and how the equipment is used, while training should reinforce correct technique and the advantages of the double blade design over existing methods.
Dedicated shadow board storage can further support standardisation by making equipment easy to locate and return.
Example 4: Rolling Out Colour-Coded Equipment
The success of a colour-coding system depends on site-wide consistency. Following a trial, existing equipment should be reviewed and any items that do not align with the agreed structure should be removed, replaced, or reassigned.
Procedures and CICs should clearly define colour allocations for specific areas, processes, or allergen zones. Visual management tools, including colour-coded shadow boards and signage, can reinforce segregation and support correct equipment selection.
Training for both operatives and supervisors should ensure consistent application across all departments and shifts, while routine monitoring will help with maintaining standards and identifying opportunities for improvement.
A well-structured trial ensures decisions are based on clear evidence rather than assumption, helping to deliver consistent, long-term improvements when new equipment is introduced.
If you would like to learn more about Klipspringer trials or any of the solutions mentioned in this article, contact our team on 01473 461 800 or email sales@klipspringer.com. Alternatively, complete the form below.
If you would like to learn more about the solutions mentioned in this article, share your details below and we will be in touch.

FSSC 22000 Version 7: What's Changing and What You Need to Know
Understanding the changes in FSSC 22000 Version 7 and what they mean for your site.
FSSC 22000 is one of the most widely recognised food safety certification schemes in the world, with over 40,000 certified organisations across the global supply chain.
With FSSC 22000 Version 7 now published (May 2026), many sites will be starting to think about what’s changing and what they need to do next.
This guide provides a helpful overview. However, for a full clause-by-clause breakdown, we recommend reviewing the official FSSC 22000 change document.
Why was there a need for FSSC 22000 Version 7?
While FSSC 22000 Version 7 is not a complete overhaul of the standard, it introduces a number of changes designed to improve clarity, consistency, and alignment across the food industry. These updates have been driven by several key factors:
- Alignment with the latest GFSI Benchmarking Requirements (2024).
- Incorporation of the revised ISO 22002:2025 prerequisite programme (PRP) series.
- Stronger support for organisations contributing to the Sustainable Development Goals (SDGs).
- A clearer structure for food chain categories.
- Ongoing improvements to make requirements more consistent and easier to apply.
Key Dates You Need to Know
If your site is certified to FSSC 22000, these are the key dates to be aware of:
- May 2026: Version 7 is published and the 12-month transition period begins.
- May 2027: Audits against Version 7 commence.
- June 2028: All Version 6 certificates will be withdrawn.
The 12-month transition period provides certified sites with sufficient time to review the changes, assess their impact, and prepare for certification audits against Version 7.
The Big Change: A New ISO 2202 Structure
One of the most important updates in FSSC 22000 Version 7 relates to prerequisite programmes (PRPs). PRPs are the basic hygiene and environmental controls that support your food safety system. They cover routine activities such as cleaning, maintenance, and facility conditions.
Previously PRP requirements were contained within different standards depending on your sector. However, Version 7 introduces a new structure:
- ISO 22002-100:2025 now acts as the core PRP standard applicable across all sectors.
- Sector-specific PRP standards (e.g. manufacturing, packaging, retail, and catering) still apply.
This means sites will now need to meet the core PRP requirements (ISO 22002-100), along with the sector-specific PRP requirements relevant to their operations.
While this change does not necessarily mean more work, it does mean that some requirements have been reorganised. Sites should therefore review their existing procedures, update their documentation, and confirm all requirements are still fully covered.
Additional Updates and Changes

Greater Focus on Competence and Ownership
FSSC 22000 Version 7 places stronger emphasis on ensuring key risks are managed by appropriately trained personnel. For example:
- Food defence plans must be developed by competent individuals.
- Food fraud vulnerability assessments must be handled by personnel with the right knowledge.
This reinforces accountability and raises expectations around expertise.

Food Safety Culture is a Clear Priority
Food safety culture is now more clearly defined and subject to greater scrutiny under FSSC 2200 Version 7. Auditors will be looking for evidence that sites have:
- Established measurable food safety culture objectives.
- Provided the resources needed to support and strengthen food safety culture.
- Demonstrated active engagement across all levels of the business.

Artwork and Labelling Controls
Artwork and labelling controls were previously limited to packaging manufacturers.
However, under FSSC 2200 Version 7, these requirements have been extended to include any organisation involved in the production of labels or printed materials.
As a result, food manufacturers that manage labelling activities in-house may now find these requirements within the scope of their certification.

Pet Food and Allergen Management
Another notable update in FSSC 22000 Version 7 is the clarification of allergen management requirements under 2.5.6 (h). The scheme now confirms that these requirements may not applicable to pet food manufacturers unless:
- There is allergen-related legislation applicable in the country where the product is going to be sold.
- An allergen-related claim has been made about the product.

Verification of Prerequisite Programmes (PRPs)
PRP verification refers to checking that your basic site controls are working effectively in day-to-day operations. In Version 7, this requirement has been expanded to include:
- Catering / food service (Category E)
- Retail / wholesale (Category FI)
Sites that fall into one of these categories may need to introduce or strengthen their routine site inspections, documented checks, and other risk-based verification activities.

NEW: Packaging Design Principles
A brand-new requirement focuses on how packaging is designed. Sites developing packaging must consider:
- Protecting the product throughout the supply chain.
- Extending the shelf life of the product.
- Reducing food loss and waste.
- Providing clear instructions for consumers.
Importantly, these principles must never compromise food safety.
Changes to Audits Under FSSC 22000 Version 7
While the certification process remains broadly the same, there are some important updates to consider during the Version 7 transition period.
Audit Duration
- Audit duration is now more flexible, taking into account both the number of full-time equivalent employees (FTEs) and the number of HACCP studies in place.
- The typical minimum audit duration ranges from 1.5 to 2.5 days, depending on the size and complexity of the organisation.
- For sites in Categories C (Food Manufacturing), D (Animal Feed Production), and K (Bio/Chemicals Production), the minimum audit duration is now two days, bringing FSSC 22000 into line with GFSI expectations.
- Reduced audit durations may be applied to sites with fewer than 20 FTEs and a maximum of two HACCP studies. Under Version 7, the threshold has been increased from one HACCP study to two.
NOTE: If the small organisation exemption is applied, the Certification Body will ensure that the audit duration is sufficient to conduct an effective audit based on the specific audit requirements, while still fully covering all FSSC 22000 requirements.
Unannounced Audits
FSSSC 2200 Version 7 introduces a clearer structure for the management of unannounced audits. It clarifies that blackout periods (periods during which the unannounced audit cannot take place) must be agreed in advance between the site and the Certification Body. It also provides guidance on how to manage situations where a site is not operational at the time of the audit.
Remote Audits
A clear limit has been introduced for remote audits. A maximum of two consecutive fully remote audits is permitted.
Multi-Site Certification
There are updated reporting requirements for multi-site certification. These provide clearer guidance for Certification Bodies on how to document and report multi-site audits, including how to calculate the audit duration for the central function (e.g. head office or central management team). It is also worth noting that Sub-Category BIII (Pre-process handling of plant products) is now included within the scope of multi-site certification.
Offsite Activities
A single method for calculating audit duration is now specified, except in campus-style operations where parameters may be combined.
If manufacturing, processing, or services activities take place offsite, the audit duration for the satellite site must be calculated separately from the main site. In these cases, a 50% reduction in the calculated base audit duration may be applied when determining the audit time for the satellite site. TFSSC still applies in addition to the calculated audit duration.
Audit Duration Calculations – Version 7
- Audit duration calculations will be reviewed in line with the requirements of Version 7.
- Certification Bodies may either issue a new Version 7 contract or apply a Version 7 addendum to the existing Version 6 contract to incorporate the new requirements.
- Audit durations will then be recalculated or reconfirmed as required.
- No additional audit time is required for the Version 7 upgrade audit.
Most of the changes in FSSC 22000 Version 7 focus on strengthening existing requirements rather than introducing completely new ones. Early review and small adjustments should help to ensure a smooth transition.
If you would like support during this process, please contact our team on 01473 461 800 or email sales@klipspringer.com. Alternatively, you can complete the form below.
If you would like to learn more about the products and solutions we provide, share your details below and we will be in touch.

How to Prevent Hygiene Risks in Food Production Environments
Discover how hygiene risks commonly develop in food factories and the practical steps that help to prevent them.
In food production environments, hygiene failures often develop gradually through small decisions, overlooked details, and routines that slowly drift away from best practice.
From poorly stored cleaning tools to equipment modifications that create inaccessible areas, these issues can go unnoticed until standards begin to slip more significantly.
This article explores where hygiene risks commonly develop within food factories and outlines practical steps for prevention.
How Do Hygiene Risks Commonly Develop?
1. Inconsistent Cleaning Procedures
Even well-established cleaning procedures can become less effective over time if routines begin to drift or shortcuts become normal practice.
Keeping Cleaning Instruction Cards (CICs) up to date is an important first step. Instructions should reflect current equipment, cleaning methods, and production layouts so teams can follow processes consistently and confidently.

It is also important to review whether procedures are practical and easy to follow. In some cases, hygiene teams may avoid using the correct tools simply because equipment storage is inconvenient or too far away from the task area.
To resolve this, mobile shadow boards can be used to reduce unnecessary movement around the factory floor while making it immediately obvious which tools should be used for specific tasks. Removing friction from the cleaning process often improves consistency far more effectively than simply introducing additional steps.
Finally, visual management can help to reinforce correct procedures. Signage and visual prompts provide clear reminders, particularly in busy production environments.
2. Static Equipment and Factory Layout
Issue 9 of the BRCGS Global Food Safety Standard highlights the importance of hygienically designed equipment, particularly in areas where contamination risks must be tightly controlled.
When installing new equipment or making modifications, easy access for cleaning and inspection should form part of the decision-making process. Poorly accessible framework, pipework, and enclosed areas will quickly become harbourage points if they cannot be cleaned effectively.

If equipment design cannot be changed easily, providing your hygiene team with the right cleaning tools becomes even more important. There are a range of solutions available to help improve access and cleaning performance. For example:
- Extendable handles combined with flexible brushes can help operatives clean around pipework and difficult access points more effectively.
- Detail cleaning brushes designed for tough or baked-on residues can improve cleaning performance in hard-to-reach areas.
- Machine-safe brush designs with built-in guards help to prevent utensils from falling behind or underneath equipment.
3. Walls, Floors, Doors and Ceilings
Walls, floors, doors, and ceilings need to withstand the demanding conditions of a food production environment. After all, they are regularly exposed to moisture, cleaning chemicals, temperature fluctuations, and repeated washdowns. If unsuitable materials are used during the initial build or later repairs, deterioration can happen much faster.
Alongside material selection, smaller design decisions can also help to reduce future hygiene risks. For example, magnetic shadow boards and signage remove the need for drilled fixings, eliminating unnecessary holes that may otherwise require ongoing sealing and maintenance.

Pooling water is another common issue that should never be accepted as “normal.” Standing water can contribute to water ingress, environmental contamination, and the deterioration of surrounding surfaces over time.
Preventative measures such as intelligent factory design, effective segregation during washdowns, and the use of moisture management tools like condensation squeegees can all help to improve control while reducing long-term hygiene risks.
4. Cleaning and Production Equipment
Cleaning and production tools can become a source of contamination if they are not properly maintained, inspected, and stored.
When selecting equipment, hygienic design and durability should be top priorities. Equipment designed specifically for food production environments is typically manufactured using food-contact approved materials, with minimal crevices and durable construction that can withstand repeated use.

Regular inspections also play an important role in ensuring worn utensils are identified early. Visual management systems can support this by clearly showing operatives what “acceptable” and “unacceptable” equipment looks like, helping teams recognise when tools need to be replaced.
Using equipment correctly is another important step. Tools used outside of their intended purpose are more likely to become damaged prematurely, reducing both their lifespan and hygiene performance.


Equipment storage is vital to effective hygiene control. Shadow board storage solutions help bring equipment into a highly visible, controlled space. They also make it easier to identify missing, damaged, or insufficiently cleaned tools before small problems develop into larger hygiene issues or are highlighted during an audit.
5. Culture and Engagement
Even the best hygiene procedures rely on the people responsible for carrying them out, so it is essential that culture and engagement are not overlooked.
Ongoing training remains important, but the focus should extend beyond simply explaining what teams need to do. Understanding the “why” behind each step helps to improve long-term engagement, particularly in areas where standards are more likely to be missed during busy production periods or under time pressure.
Internal audits can also help reinforce accountability by identifying where behaviours have started to drift from expected standards.

Improving hygiene culture is not solely about increasing oversight. In many cases, the most meaningful improvements come from removing barriers that make the wrong approach easier than the right one.
As discussed throughout this article, solutions such as visual management, accessible storage, and up-to-date Cleaning Instruction Cards (CICs) can reduce uncertainty by making expectations visible, ensuring equipment is easy to locate, and aligning procedures with real site conditions. Measures like these help teams to understand what is required and reduce variation between shifts.
Hygiene risks rarely appear overnight. By improving equipment design, cleaning processes, visual management, and team engagement, food manufacturers can prevent small issues from developing into larger food safety problems.
If you would like to learn more about any of the solutions mentioned throughout this article, contact our team on 01473 461 800 or email sales@klipspringer.com. Alternatively, fill out the form below.
If you would like to learn more about the solutions mentioned in this article, share your details below and we will be in touch.

Mastering Allergen Testing: Webinar Q&A with Barbara Hirst
Webinar Q&A: Keynote Speaker Barbara Hirst Answers Questions on Allergen Testing
Following our industry webinar, Mastering Allergen Testing: Best Practice and the Role of Rapid Testing, keynote speaker Barbara Hirst joined Klipspringer’s Engagement Manager, Guy Bush, to answer the audience questions we didn’t have time to cover during the live session.
The following article also includes Barbara’s responses from the webinar Q&A, bringing together all of her expert insights for easy reference.
If you have any further questions about allergen testing, Klipspringer’s in-house Technical Team is here to help. Simply click here to submit your query, and we’ll be in touch.

Barbara Hirst | RSSL
Barbara is a Senior Consultant in the Food Safety and Quality team at RSSL, specialising in allergen management. She works closely with food production sites to identify allergen control challenges and implement practical and effective solutions.
Do denatured proteins still present an allergen risk?
Barbara addressed this question during both the live webinar and the following Q&A.
Barbara explained that although denatured proteins can be more difficult to detect, this does not mean they are no longer allergenic. Put simply, they can still pose a risk to allergic consumers.
Barbara added that the Morinaga test kits discussed during the webinar are particularly well regarded for their ability to detect denatured proteins and are becoming more widely used across the industry. At RSSL, Morinaga tests are used for a range of allergens, including milk and egg, where they perform especially well.
Barbara also highlighted the importance of positive control testing. This involves submitting a product known to contain the target allergen for ELISA testing. The results can help to determine whether the selected on-site test method is suitable for the specific product and processing conditions being evaluated.
Why are qualitative results recommended for verification purposes rather than quantitative testing?
Barbara highlighted that validation and verification serve different purposes and therefore require different testing approaches.
Validation
Validation is not only about determining whether an allergen is present, but also about understanding how much is present. For this reason, it requires a quantitative test (e.g ELISA) which provides a numerical result rather than a simple detected/not detected answer.
Verification
Verification follows validation and is focused on confirming that existing controls and processes are still working effectively. For this purpose, a qualitative test that provides a detected/not detected result is sufficient, provided the limit of detection is understood.
Regarding the limit of detection (LOD), Barbara explained that this is the lowest concentration at which an allergen can be reliably detected.
Quantitative tests, such as ELISA methods, also have a limit of quantification (LOQ), which is the lowest concentration at which the allergen can be accurately quantified.
How can sites balance practical on-site requirements such as speed and ease of use with the need for accuracy?
Barbara acknowledged the pressures sites face around cost and speed but warned that there are no shortcuts when it comes to allergen validation. She explained that if factories attempt to take the “cheap and cheerful” route, their results may not be reliable and could create a false economy.
Barbara stressed the importance of careful planning, taking samples from the correct locations, using appropriate test methods, and working with competent laboratories to ensure confidence in the results being generated.
How often should allergen testing programmes be reviewed or revalidated?
Barbara advised that allergen validation should always be reviewed whenever anything significant changes. Examples discussed included changing cleaning chemical suppliers, modifying equipment, altering production layouts or changing the cleaning process itself.
Alongside change-driven reviews, Barbara recommended carrying out at least an annual formal review to confirm whether anything has changed that could impact the effectiveness of allergen controls. She also noted that some retail customers may require annual validation activities as part of their own supplier policies.
Why do rapid swabs still require site-level validation if the manufacturer has already validated them?
Barbara explained that while the manufacturers of rapid tests carry out extensive validation work before launching their products, they cannot possibly validate every individual food matrix or production scenario.
Using the example discussed during the webinar, she explained that a milk test may have been extensively validated on liquid milk, cream or even cheese, but not on a specific product such as a Parmesan-topped ready meal.
Without site-specific validation, sites cannot assume the test will perform with the same sensitivity in every application. In some cases, Barbara noted that sensitivity can be reduced by 100- or even 1,000-fold depending on the ingredient or product matrix involved.
Why is rapid testing described as a qualitative method?
Barbara clarified that rapid tests remain qualitative because they provide a yes-or-no answer regarding allergen presence. Although rapid tests may have a defined limit of detection, they do not measure how much allergen is present.
Quantitative ELISA testing, by contrast, is used when sites need to understand allergen concentration levels, such as during cleaning validation studies or finished product analysis.
How can sites reduce false positives in rapid testing programmes?
Barbara returned to the importance of validating rapid tests before use. Validating them against site-specific products and processes helps to reduce the risk of both false positives and false negatives.
She explained that false positives can lead sites to believe equipment is not clean when it actually is, potentially resulting in unnecessary recleaning or production delays.
However, false negatives present a greater risk, as sites may believe allergens are absent when residues are still present. This could result in subsequent products being manufactured under the assumption that equipment is clean, when allergen residues remain on the line.
Is a laboratory ELISA method always more sensitive than a rapid test, and is it possible to get different results for the same sample?
Barbara stressed that it is not possible to make a generalised comparison, as there is a wide range of tests on the market that detect slightly different things and operate with varying levels of sensitivity.
She also confirmed that different ELISA and rapid testing methods can absolutely produce different results for the same sample.
However, variations in results do not automatically mean that one method is correct and another is incorrect. Instead, they may arise because different kits target different proteins, use different analytical approaches, or operate at different sensitivity thresholds.
The key, once again, is understanding how each method performs through proper validation work.
Is there a recognised reference list of cross-contaminants that sites can use?
Barbara explained that all biological assays, including both ELISA and rapid tests, are likely to demonstrate some degree of cross-reactivity, which can lead to false positive results.
Manufacturers of allergen testing kits will usually provide cross-reactivity reports and validation data outlining known interactions. Barbara stressed that food factories are responsible for reviewing and understanding this information before implementing a testing method.
However, she also noted that test kit manufacturers cannot possibly assess every ingredient or finished product combination. For this reason, sites still need to confirm whether their own ingredients, products, or manufacturing conditions could create unexpected cross-reactivity issues during testing.
Is it good practice to continue annual swabbing/testing even if it is only to justify the ongoing use of Precautionary Allergen Labelling (PAL)?
Barbara explained that cleaning validation is about demonstrating whether a site’s cleaning process is effective. If residues are found on surfaces, and more importantly if they are carried over into the next product, this is a clear indication that the cleaning process is not effective.
In such cases, the first step is to understand why the cleaning is not effective and identify what can be improved. Businesses have an obligation to achieve the cleanest possible outcome while remaining reasonably practical and cost-effective.
If, despite best efforts, residues cannot be reduced to non-detectable levels when tested using a ELISA method, then precautionary allergen labelling (PAL) may be appropriate. However, there is an expectation that everything reasonable is done to minimise or avoid the need for this.
What is your recommendation for the surface area for swabbing? What about conveyors that are several metres in length?
Barbara confirmed that, ideally, a 10 cm × 10 cm area is what you should aim for when it comes to surface swabbing.
She explained that, prior to sampling, it is best practice to examine the line when it is dirty and identify where product tends to get stuck. These are the areas that should be targeted after cleaning. For long conveyors, this may include worn edges or the space around the rollers.
The key is to maximise the probability of detecting any residual contamination by targeting the “worst-case” scenario. If these areas are clean, it can reasonably be assumed that the rest of the surface is also clean.
Barbara also cautioned against swabbing areas significantly larger than the 10 cm × 10 cm guideline, as this may produce results that are not representative of cleaning effectiveness. While it may increase the likelihood of detecting residue, it does not reflect a defined sampling area.
She added that the swabbing process can be more complex for irregular surfaces such as pipes, which is why results should be reported as amount per swab rather than parts per million, since the sampled area is not always precisely defined.
How are spike recovery tests done and who should do them?
Test manufacturers such as Morinaga will have completed extensive spike and recovery testing, with details typically provided in the validation report. However, it is not reasonable to expect manufacturers to have carried out this process using every factory’s specific product matrix. For this reason, spike and recovery testing should be performed by your laboratory.
Missing this step can lead to false positive or false negative results. The former may trigger an unnecessary product recall, while the latter could result in a serious food safety incident. Despite its importance, spike and recovery testing is not a UKAS requirement and may therefore need to be specifically requested from your laboratory. If the laboratory has not requested an ingredient list, this may indicate that spike and recovery testing has not yet been considered.
Barbara explained that ideally, whenever a laboratory receives a new sample, it should review the ingredient list and consider whether it has analysed a similar matrix before. If it has, repeat spike and recovery testing may not be necessary. If it has not, the laboratory should spike the sample with a known amount of allergen, run it through the assay, and measure the recovery. The expectation is close to 100% recovery, within an acceptable level of uncertainty.
When carrying out a validation and swabbing equipment surfaces, can a composite swab be used?
Barbara explained that composite swabs are almost always a bad idea and a false economy. Although they may appear to save time or cost, for example asking your laboratory to combine five swabs into one sample, there are two key issues with this approach.
Firstly, combining swabs can dilute any contaminant to the point where the test may incorrectly indicate that no allergen is present. Secondly, if a combined sample does return a positive result, it is not possible to determine which of the original swab locations was responsible.
That brings us to the end of our webinar Q&A roundup.
We hope you found Barbara’s expert answers helpful and informative. If you would like to learn more about allergen testing and best practice, we recommend watching the webinar in full.
If you have any additional questions, you can submit them using the contact form below. Simply enter your details and a member of our in-house Technical Team will be in touch with a response.
If you would like to learn more about our range of Allergen Tests, share your details below.

WEBINAR: From Awareness to Action: How You Can Bring World Food Safety Day Alive
WEBINAR: From Awareness to Action: How You Can Bring World Food Safety Day Alive
Discover how food factories can use World Food Safety Day to drive genuine engagement and lasting improvement. This webinar explores practical ideas to bring food safety to life through interactive activities, team involvement, and meaningful communication. Learn how to turn the event into more than a one-day campaign by embedding positive food safety behaviours into everyday operations across your site.

World Food Safety Day Resource Pack
- World Food Safety Day Showdown Quiz
- Interactive workshop featuring a realistic food safety scenario
- World Food Safety Day Bingo Challenge
- Customisable pledge template for WFSD commitments
Webinar Speakers

Alex Carlyon
Specialism: Food Safety
and Compliance

Natalie Smith
Specialism: Employee Engagement
& Company Culture

Lauren Bere
Specialism: Leadership Support
& Communications
Key Webinar Areas

1. World Food Safety Day - The Bigger Picture

2. From Tick Box To Talking Point - Engagement That Really Lands

3. Ten Activities To Bring World Food Safety Day Alive At Your Site

4. Beyond The Day - Building A Culture That Sticks
5. Q&A Session With Our Panel Of Experts
If you have any questions for our team of experts, share your details below...

The 3 Software Packages Behind WatchmanOne Real-Time Wireless Monitoring
Discover which of the three WatchmanOne software packages is best suited to your site.
One of the strengths of the WatchmanOne Real-Time Wireless Monitoring System is its flexibility.
Rather than forcing every customer into a one size fits all approach, WatchmanOne offers three different software packages, allowing you to choose the level of access, reporting, and remote control that best fits your operation.
Whether you want a simple on-site monitoring solution or a fully featured, multi-site reporting package, there’s an option to match.
1. Base Station Package (Standard Option – Free of Charge)
The Base Station Package is the core software that comes as standard with every WatchmanOne system. It is a browser based, on site package designed for day to day monitoring and alarm management.
It allows users to connect sensors, set alarm limits, and manage user access. Because it operates on a local network (LAN), system changes can only be made while connected on site. However, alarms and notifications are still received remotely.
This package is ideal for single site operations that want secure, no subscription monitoring with minimal complexity.
2. Connect Direct (Remote Access – No Subscription)
Connect Direct builds on the Base Station Package by allowing remote access from anywhere, without introducing a subscription fee.
Functionally, it is the same interface as the Base Station, but accessed through the MyDataPortal login screen. This means users can make system changes, acknowledge alarms, and manage settings even when off site.
What it does not include is the advanced reporting, analysis tools, or visual features found in MyDataPortal. Connect Direct is best suited to customers who need remote control without the cost of a full cloud package.
3. My Data Portal (Advanced and Subscription-Based)
MyDataPortal (MDP) is the most powerful WatchmanOne package. It is designed for multi-site operations, advanced reporting, and future scalability.
MDP offers full access from anywhere in the world, advanced data analysis, automated reporting, virtual sites, site maps, and multi site dashboards. It also includes a mobile app for iOS and Android.
All new software development is focused on MDP, making it the most future proof option. It is available via an annual subscription, paid per base station.
WatchmanOne Software Packages – Comparison Table
| Feature | Base Station Platform | Connect Direct | MyDataPortal (MDP) |
|---|---|---|---|
| Cost | Free of charge | Free of charge | Annual subscription (per base station) |
| Access location | On-site network only | Anywhere | Anywhere |
| Remote alarm notifications | ✔ Yes | ✔ Yes | ✔ Yes |
| Make system changes remotely | ✘ No | ✔ Yes | ✔ Yes |
| Advanced reporting & analysis | ✘ No | ✘ No | ✔ Yes |
| Multi-site monitoring | ✘ No | ✘ No | ✔ Yes |
| Site maps & virtual sites | ✘ No | ✘ No | ✔ Yes |
| Mobile app | ✘ No | ✘ No | ✔ iOS & Android |
| Best suited for | Simple, single-site monitoring | Remote access without subscription | Multi-site, audit-driven operations |
Each WatchmanOne software package is designed to support different operational requirements, whether that’s straightforward on-site monitoring, remote system access, or more advanced reporting across multiple locations.
If you would like to learn more about the WatchmanOne System or its three different software options, contact our team on 01473 461 800 or email sales@klipspringer.com. Alternatively, fill out the form below.
If you would like to learn more about the WatchmanOne System or the different packages available, share your details below.

Mobile Work Stations for Food Factories: 5 Key Benefits for Efficiency and Compliance
This article explores five key benefits of mobile work stations in food production.
Mobile work stations provide a flexible way to improve control, organisation, and efficiency across food production environments.
If you are thinking about introducing them to your site, the following article outlines five key benefits for you to consider.


1. Improve Flexibility Across Production Areas

Mobile work stations allow equipment to be positioned exactly where it is needed, when it is needed. The braked castor wheels provide smooth and controlled movement between areas, making it easy to relocate the stations if production demands change, then fix them in place as required.
This flexibility will help to streamline operations and reduce unnecessary movement.
It will also help to minimise disruption during changeovers, allowing work areas to be quickly reset without slowing down production and compromising productivity.
2. Support Consistent Processes

The consistent monitoring of Critical Control Points (CCPs) is an essential part of maintaining food safety standards. This is also true of accurate record keeping and the use of clear processes that are easy to understand.
A dedicated mobile work station provides an organised space for storing equipment, clipboards, and important documents, ensuring everything required is kept in one place, instead of being spread out across your site.
This will help to improve the consistency and reliability of CCP checks, while also supporting greater control and visibility.
3. Make Life Easier for Your Hygiene Team

Poorly designed workstations have the potential to harbour harmful bacteria, undermining hygiene standards and increasing the risk of contamination.
Mobile work stations provide a durable, easy-to-clean solution, featuring stainless steel frames and food-safe, water-repellent surfaces that won’t peel over time.
Another benefit is flexibility during cleaning, as mobile workstations can be wheeled into designated washdown areas. They also allow for a full 360 clean, which is more difficult to achieve with stations that are fixed to the wall.
4. Organise Equipment and Reduce Costs

Time spent searching for missing tools and equipment can impact productivity and negatively affect morale.
With designated storage areas, optional shelving, and the ability to introduce a shadow board set up, mobile work stations ensure everything has a clear and accessible home.
This not only improves efficiency, but also helps to prevent equipment from being misplaced, damaged, or moved between areas unnecessarily. The angled writing surface will also stop essentials from falling to the floor, further reducing replacement costs.
5. Secure Audit Compliance

Version 9 of the BRCGS Global Food Safety Standard highlights the importance of equipment control and documented food safety procedures.
Mobile work stations can play a valuable role in strengthening audit performance by providing a clear and highly-visual approach to managing both equipment and records.
The visibility and organisation provided by these stations also supports traceability, making it easier to demonstrate procedures are being followed consistently across different shifts, teams, and areas of your site.
From increasing flexibility and supporting hygiene standards, to improving equipment control and strengthening compliance, mobile work stations bring greater visibility and control to key processes.
If you would like to learn more about this popular solution, contact our team on 01473 461 800 or email sales@klipspringer.com. Alternatively, fill out the form below.
If you would like to learn more about mobile work stations or our complete range of equipment storage, share your details below and we will be in touch.
About the Author
Libby Loughnan is a Content Executive specialising in food safety and compliance. She has written extensively on equipment management, hygiene best practice, and lean manufacturing.

Food Factory Guide to High Heat Cleaning and Production
Discover how high heat cleaning and production equipment can solve common challenges in food factory environments.
Without the right tools and procedures in place, high temperature areas can quickly become difficult to manage, leading to burnt-on residues, equipment damage, and increased risk to both your product and team.
This article explores the role of high heat equipment in food manufacturing and the risks associated with these environments. You’ll also find practical solutions for maintaining hygiene and efficiency.
What are the Key Challenges of High Heat Environments?

Burnt-On Residues
When food debris is exposed to high temperatures it can carbonise and adhere to surfaces. Standard cleaning tools often become ineffective under these conditions and may degrade from heat exposure.

Hygiene and Food Safety
If residues build up over time, this has the potential to impact food safety and audit compliance. Inconsistent cleaning can also affect heat transfer and equipment performance.

Equipment Damage
Tackling debris with unsuitable equipment, such as metal or wire brushes, can damage surfaces over time. This can lead to deep scratches with the potential to harbourage harmful bacteria.

Operator Safety
As you can imagine, cleaning at high temperatures presents a serious risk to operator safety. Without the right tools, workers may be forced to get too close to hot surfaces, increasing the likelihood of burns or injury.
High Heat Cleaning Equipment
Using equipment specifically designed for high temperature environments is key to maintaining both safety and hygiene.
High heat-resistant brushes made with PEEK bristles provide a durable and food-safe solution for cleaning hot surfaces. These bristles can withstand contact temperatures of up to 250°C, allowing effective cleaning without degrading or contaminating the area.
Compared to traditional wire brushes, they also reduce the risk of surface damage while remaining tough enough to remove stubborn residues.


For example:
- Long-handled utility brushes allow operatives to clean from a safer distance, reducing direct exposure to heat while maintaining control.
- Short machine brushes are well suited to detailed cleaning of smaller components and hard-to-reach areas.
- Griddle brushes with extra-stiff bristles are ideal for removing heavy, baked-on residues from flat cooking surfaces.
Selecting the correct brush for the application ensures effective cleaning while protecting both equipment and operators.
High Heat Production Equipment
Cleaning is only one part of working in high temperature areas. Production tools must also be capable of withstanding sustained heat.
High heat utensils manufactured from specialist polymers offer a reliable solution for direct contact with hot surfaces and products.


Hand spatulas designed for temperatures up to 250°C provide durability alongside improved grip and control, making them suitable for a wide range of production tasks.
For larger vessels or deeper cooking environments, high heat paddles offer both reach and strength. Paddles with longer stainless steel handles allow operators to work safely with hot contents, while shorter versions provide greater control in more confined spaces.
Features such as chamfered edges and integrated hooks further support ease of use and efficiency during production.
Visual Management in High Heat Areas
Visual management solutions can be used to promote safety and audit compliance throughout high temperature applications.
Clear, attention-grabbing signage reinforces correct procedure and key training points, helping teams to drive efficiency and reduce downtime.
Dedicated PPE boards also play an important role in communicating the required protective equipment for high heat applications, protecting team members from accident or injury.


From high heat-resistant brushes to durable production utensils, the right equipment plays a key role in ensuring safe and efficient operations.
For more information on high heat cleaning and production tools, contact us on 01473 461 800 or email sales@klipspringer.com. Alternatively, fill out the form below.
If you have any questions about high heat hygiene or production equipment, share your details below and we will be in touch.

Everything You Need to Know About AI in Food Production
The role of AI in food production, plus what it means for safety, efficiency, and risk.
Artificial intelligence (AI) is starting to play a bigger role in the food production industry. It is being used to support everyday tasks, inform key decisions, and improve standards of food safety.
The following article explores the current applications of AI in food production, along with the potential opportunities and risks that come with its adoption.
Emerging Uses of AI in Food Production

Supply Chain & Inventory Management
AI can help businesses better manage stock levels and predict demand. By analysing past trends and current data, it becomes easier to produce the right amount of product at the right time. This reduces waste, avoids overproduction, and helps ensure products are available when needed.

Food Safety and Quality Control
AI is being used to identify defects and inconsistencies in products. Automated systems can analyse images or data to spot issues that might be missed during manual checks. There is also the potential for AI to be used for product testing, combining different types of analysis into a single result.

Food Safety and Risk Prevention
By analysing large amounts of data, AI systems can identify patterns linked to contamination or foodborne illness. This allows businesses to act earlier, addressing potential issues before they become serious problems. It also improves traceability, making it easier to track where products and ingredients have come from.

AI, Compliance and Documentation
AI is helping to simplify compliance by improving how data and records are managed. Many systems can automatically organise documentation, track activity, and support audit preparation. Moving away from paper-based systems makes it easier to access information and keep records up to date.
“AI is transparent and auditable. It can monitor, predict, and record data to support future traceability exercises and reporting.”
Stuart Warren, Senior Food Safety Manager, Coca-Cola EuroPacific Partners
The Benefits of AI
Supporting Risk Management
By identifying risks earlier, AI allows businesses to take a more proactive approach to food safety. This reduces the likelihood of issues developing into larger problems.

Improving Efficiency
AI can automate routine tasks, reduce manual work, and improve consistency across production and quality control processes. It can also help teams plan more effectively, cutting down on waste and making better use of resources.
The Risks and Limitations
Data Quality and Reliability
AI systems depend on good-quality data. If the data is inaccurate or outdated, the results produced by AI may also be unreliable.
Over time, systems can also become less accurate if they are not regularly updated to reflect changes in products, environments, or processes.

Cybersecurity and Data Risks
As more systems become digital, the risk of data breaches and manipulation increases. This could include unauthorised access, internal misuse, or changes to important records.
For this reason, it’s important that AI systems are supported by strong verification processes and human oversight.
“We need to bring people on the AI journey. It’s about being transparent about how AI is going to support your food business going forward.”
Stuart Warren, Senior Food Safety Manager, Coca-Cola EuroPacific Partners
Key Considerations for Implementing AI

Governance and Oversight
AI systems need clear rules and controls to ensure they are used correctly. This includes managing data securely and maintaining accountability for decisions. Human involvement remains essential, particularly when making critical food safety decisions.
Skills and Training
As AI becomes more widely used, there is a growing need for training. Teams need to understand how to use these systems and how to interpret the results they produce.
Culture and Collaboration
AI works best when it is part of a wider food safety culture. It should support existing processes and encourage collaboration between teams, rather than operate in isolation.
AI is likely to play a central role in the future of food production, particularly when it comes to improving food safety, increasing transparency, and reducing inefficiencies.
However, regulation is still developing, and businesses will need to take responsibility for managing both the opportunities and the risks.
To learn more about this topic, check out our industry webinar on AI and real-time data. It features key insights from Stuart Warren, Senior Food Safety Manager at Coca-Cola EuroPacific Partners.
If you have any questions for the Klipspringer team, share your details below and we will be in touch.

What Does the Clean Label Trend Mean for Food Manufacturing?
What the clean label movement means for food manufacturing, plus how to engage with this emerging trend.
As clean label expectations grow, manufacturers are under increasing pressure to reduce additives without compromising safety, stability, or shelf life.
The following article takes a closer look at what the clean label movement is, its potential impact on the food production industry, and the five key solutions that will help sites succeed in this area.
What is Clean Label?

Most clean label products aim for:
- Shorter ingredient lists, with fewer and more recognisable components
- No artificial additives, such as colours, flavours, or preservatives
- Natural or minimally processed ingredients
- Greater transparency around sourcing and production methods
- “Kitchen cupboard” familiarity, using ingredients consumers feel they understand
The Impact of the Clean Label Movement

Consumer expectations around food have shifted significantly over the past decade, and clean label has become closely tied to how products are perceived.
It is often associated with health and wellbeing, even in cases where there is little nutritional difference. At the same time, clean labels can play an important role in building trust, giving consumers greater confidence in what they are buying and how it has been made.
The clean label movement also aligns with wider consumer concerns around sustainability, provenance, and processed foods.
Shelf Life, Safety & Consistency
Removing or reducing artificial additives presents a number of challenges for the food production industry, particularly in maintaining product stability and safety over time.
Preservatives help keep food safe by slowing spoilage and maintaining product quality. If a manufacturer decides to move away from them, they will need to rely on a combination of other methods to achieve the same results.

Working with more natural ingredients can also affect how ingredients behave during processing, making consistency at scale more difficult to achieve.
There is also a direct effect on sensory quality. Consumers still expect strong performance in taste, texture, and appearance, but removing additives can influence all three.
Solutions to Support Clean Label Production
You will already be familiar with many of the solutions below, as they play a central role in maintaining food safety, quality, and shelf life.
In a clean label context, however, their importance increases. With fewer traditional additives available, greater control must be achieved through the accurate measurement of key parameters.
1. Real-Time Wireless Monitoring

Real-time wireless monitoring provides continuous visibility of environmental conditions such as temperature and humidity.
By automatically collecting data, these systems reduce reliance on manual checks and identify deviations as they occur. This enables faster corrective action, helping prevent issues before they affect product safety or quality.
In a clean label context, this level of control is especially important. With fewer preservatives acting as a safety buffer, maintaining stable conditions is essential for protecting shelf life and ensuring product consistency.
2. pH and Electrochemical Equipment

Most spoilage organisms and pathogens cannot survive in highly acidic conditions, making pH a key tool for preserving products without the use of artificial preservatives.
pH meters help ensure products consistently reach and maintain target acidity levels, supporting both safety and shelf life.
This is particularly important in acidified products such as sauces, dressings, and pickles, as well as fermented foods like yoghurt and kimchi. In these applications, controlled pH reduction is essential for preservation, flavour development, and overall product stability.
3. Water Activity Meters

Water activity (aw) reflects how much of a product’s available water can support microbial activity, making it a critical control point for food safety and shelf life.
Water activity meters help ensure products remain within safe limits, reducing the risk of spoilage while maintaining product quality. This is particularly important in products like baked goods and powders, where small changes can affect texture, shelf life, and microbial stability.
In a clean label context, controlling water activity is an essential tool for maintaining consistency and reducing reliance on additives.
4. Food Industry Thermometers

Temperature is one of the most influential factors affecting shelf life, as it directly impacts microbial growth and enzymatic activity.
Food industry thermometers help ensure that correct temperatures are achieved and maintained throughout processing, storage, and distribution. This reduces the risk of pathogens such as Salmonella and Listeria monocytogenes.
By maintaining consistent temperature control across the production chain, manufacturers can support both safety and shelf life without increasing reliance on preservatives.
5. Gas Analysers

Gas analysers play a key role in controlled atmosphere techniques such as Modified Atmosphere Packaging. They verify that the correct gas mixture is within each pack – enhancing shelf life and product quality.
They also help to identify packaging issues. Even small defects can allow oxygen ingress or gas loss, which can quickly compromise shelf life. Early detection prevents these issues from escalating into wider batch failures.
In addition, gas analysers are used to monitor respiration in fresh produce and to limit oxidation in products such as coffee and dairy.
Clean label may not be the priority for every manufacturer, but it is a growing area of focus. For those choosing to engage with this trend, success depends on maintaining high standards of product safety, stability, and quality.
If you have any questions about the clean label movement or the solutions discussed in this article, contact us on 01473 461 800 or email sales@klipspringer.com. Alternatively, fill out the form below.
If you have any questions about the solutions mentioned throughout this article, share your details below and we will be in touch.

Water Ingress in Food Factories: Risks, Equipment Damage & Prevention Strategies
Water ingress in food factories has the potential to damage equipment, disrupt production, and compromise food safety.
What is Water Ingress in a Food Factory?
What are the Potential Consequences of Water Ingress?


Equipment Failure and Downtime
Food Safety and Hygiene
Compliance and Audit Readiness


Segregation & Preventing Water Ingress


SegriCovers
SegriScreens
SegriCurtains
If you have any questions about water ingress or the solutions referenced throughout this article, share your details below and we will be in touch.

Colour-Coding and Audit Compliance: Best Practices for Food Manufacturing
A practical look at BRCGS colour-coding requirements and how to ensure audit success across your food production site.
Audit Expectations for Colour-Coding
Colour-Coding and Foreign Body Control (Clause 4.9.4)

Colour-Coded Spill Kits
- Support colour-coding and segregation.
- Include essential cleaning equipment.
- Available in up to 11 colours: blue, red, yellow, green, white, black, orange, purple, grey, brown and pink.
Colour-Coding in Cleaning and Hygiene (Clause 4.11.6)

Shadow Board Storage Solutions
- Customised boards, delivered in 5-7 working days.
- Five hassle-free mounting methods.
- Supplied with fully certified food-grade equipment in up to 11 distinct colours.
PPE and Colour-Coding Requirements (Clauses 7.2.3 and 7.4.5)
Clause 7.2.3
Clause 7.4.5

Metal Detectable Plasters
- Highly visible and metal detectable to reduce the risk of a foreign body incident.
- Designed to meet the needs of the food manufacturing and processing sector.
- Assorted sizes to accommodate various wound types.
Colour-Coding to Support Segregation in High-Risk and High-Care Areas (Section 8.3)
Clause 8.3.1
Clause 8.3.3
Employee Engagement and Colour-Coding
Visual Management
Ongoing Training

Visual Management
- Manufactured using food-safe materials that won't peel.
- Four material options: flexible magnetic, flexible self-adhesive vinyl, rigid aluminium composite, and rigid magnetic composite.
- Four mounting options: fixed-to-wall, magnetic-to-wall, freestanding frame, and mobile frame.
What Auditors Are Looking For
If you have any questions about colour-coding solutions or would like support in improving compliance across your site, share your details below and we will be in touch.

Starting a New Role in Food Production: Practical Support from Klipspringer
Discover five key areas where Klipspringer can help you succeed in your new role.
1. Accessing Your Web Portal

2. Ensuring Instruments are Audit‑Ready
- A central location for the storage of documents and certificates
- Details of when each item is next due for calibration
- Details of whether off-site or on‑site calibration is used
- Information relating to which instruments require urgent attention ahead of audits

3. Understanding Your Colour-Coding Policy

4. Environmental Testing, Allergen Control, and Hygiene Best Practice


5. Ongoing Support and Expert Guidance
Starting a new role can be overwhelming, but Klipspringer is here to make it easier. With over two decades of experience across the food industry, we provide practical support in food safety, audit compliance, and everyday operations.

As a BRCGS partner organisation, we can help you stay inspection-ready, guiding you through compliance requirements so you can be confident from day one.
Our customer support and in-house technical teams are available to answer questions, explain equipment options, and help you implement the right solutions to save time, reduce costs, or meet any other pressing KPIs.
You can also visit our Knowledge Hub for training resources, (blogs, guides, and video tutorials). With everything in one place, you can quickly access advice exactly when you need it.
Understanding your site’s equipment, keeping instruments audit-ready, managing your colour-coding policy, selecting the right testing methods, and making the most of ongoing support will help you get up to speed in your new role.
Klipspringer is here to support you at every step. You can contact our team on 01473461800 or sales@klipspringer.com. Alternatively, you can fill out the form below.
We’re on hand to provide guidance, answer your questions, and help you find the right solutions for your site. Share your details below and we will be in touch…

Webinar Round Up: Leveraging Real-Time Monitoring for Meaningful Insights
Insights from an Industry Webinar on Leveraging Real-Time Monitoring for Meaningful Insights in Food Production.
In this article, we recap insights from an industry webinar exploring how real-time monitoring goes beyond compliance to support data-driven decision-making.
The session featured expert perspectives from:
- Alex Carlyon, Key Account Director at Klipspringer
- Radek Tameczka, Real-Time Monitoring Specialist at Klipspringer
- Stuart Warren, Senior Food Safety Manager at Coca-Cola Europacific Partners
If you are short on time, you will find a bulleted list of key takeaways at the end of each section.
Real-Time Monitoring – An Introduction
What Is Real-Time Wireless Monitoring?
Real-Time Wireless Monitoring vs. Passive Data Logging
Key Takeaways
BRCGS Requirements and Audit Compliance
Maintaining Conditions and Record Keeping
Continuous vs. Non-Continuous Monitoring Methods
Key Takeaways
The Business Case for Real-Time Monitoring
Real-Time Monitoring and Marginal Gains
Novak Djokovic & Marginal Gains
“What Gets Measured Gets Managed.”
Key Takeaways
The Current State of Food Safety & Why Change Is Happening
Why Is Change Happening?
The Growing Impact of AI
Key Takeaways
Understanding AI & Its Practical Role
What Do We Mean By AI?
Practical AI – What It Is & What It Isn’t
The Evolution of Food Safety Systems
Key Takeaways
Moving to Predictive Food Safety
From Supplier Audits to Supplier Intelligence
Turning Data into Action
The Future of Food Safety
Key Takeaways
WatchmanOne: Real-Time Monitoring

The next generation of Real-Time Wireless Monitoring, trusted by industry leaders across the UK and Ireland.
- Instant alarm notifications if parameters are breached.
- Automated reporting for easy analysis.
- Versatile system with up to 150 sensors.
- No surprise costs or ongoing fees.
- Data is fully secure and belongs to your business.
Webinar Q&A
Energy Efficiency & Building Trust
Vibration Monitoring & Accessibility
Key Takeaways
If you have any questions about Real-Time Wireless Monitoring, share your details below.

WEBINAR: Mastering Allergen Testing: Best Practice and the Role of Rapid Testing
WEBINAR: Mastering Allergen Testing: Best Practice and the Role of Rapid Testing
Despite significant investment, allergen recalls are still rising. So what’s going wrong? Testing plays a critical role in allergen management, but not all strategies are as effective as they seem. Misunderstandings around rapid tests, validation, and verification can create gaps that put both consumers and brands at risk.
Inspired by our recent industry forum on allergen management, this webinar will help you to:
- Build robust allergen testing protocols.
- Explore the role and limitations of rapid allergen tests.
- Avoid common mistakes that undermine your controls.
- Identify when alternative approaches, such as the A3 system and protein testing, may be more effective.


White Paper: Getting Allergen Testing Right - The Foundation
- Key principles for a robust allergen testing programme.
- Best practice guide for cleaning validation.
- Expert advice on choosing the right laboratory.
Barbara Hirst: Q&A
Keynote Speaker Barbara Hirst sat down with Klipspringer’s Engagement Manager Guy Bush to address the unanswered questions shared during the webinar’s Q&A.
Webinar Speakers
Alex Carlyon
Key Account Director,
Klipspringer

Radek Tameczka
Allergen Testing Specialist,
Klipspringer

Barbara Hirst
Senior Consultant, Food Safety
and Quality, RSSL

Masayoshi (Masa) Tomiki
Senior Manager, Morinaga BioScience, Inc
Keynote Speaker
Barbara Hirst
Barbara is a Senior Consultant in the Food Safety and Quality team at RSSL, specialising in allergen management. She works closely with food manufacturers to identify allergen control challenges and implement practical, effective solutions. In this webinar, Barbara covered the following areas:
- Key considerations for allergen sampling.
- Important factors to consider when using ELISA testing.
- How to work effectively with a laboratory.
- How to ensure reliable laboratory results.
- How to use rapid on-site testing to maximise efficiency.
Key Webinar Areas
1. How to get the best out of allergen testing.

2. Rapid Allergen Testing: What Works and When?
3. Choosing the Right Rapid Allergen Test For Your Site

4. What is the Right Tool for You? Alternatives to Rapid Tests?
5. Q&A Session With Our Panel of Experts
Allergen Testing Kits

A new standard in allergen detection, delivering high levels of accuracy and reliability.
- EASY Test Kits: suitable for rapid surface testing and rinse water verification.
- PRO Test Kits: suitable for for testing allergens within food samples, even highly-processed products.
- ELISA Test Kits: suitable for highly sensitive detection of allergens in raw materials and processed foods.
If you have any questions about allergen testing, share your details below...

Preparing for the UK-EU SPS Agreement: What Food Manufacturers Need to Know
The UK Government has confirmed that a Sanitary and Phytosanitary (SPS) agreement with the EU is in progress. Implementation is expected from mid-2027.
Particularly relevant to food manufacturers, processors, and suppliers, this development reflects a wider shift towards greater alignment with EU standards, bringing both new opportunities for trade and increased expectations around compliance.
In the following article, we will share a quick overview of the SPS agreement. We will also explore how your business can prepare for these changes and where Klipspringer can support you.
The SPS Agreement
Covering areas such as food safety, hygiene, labelling, additives, and pesticide regulation, the SPS agreement aims to reduce the complexity that many businesses have faced since Brexit.
For businesses currently trading with the EU, this could mean fewer delays, less paperwork, and more predictable supply chains. For those that stepped away from EU markets, it may present an opportunity to re-enter with greater confidence.

However, while trade barriers at the border are expected to decrease, expectations within production environments will increase.
To benefit from smoother access to EU markets, UK businesses will need to consistently meet EU aligned standards. This includes a stronger focus on hygiene practices, traceability, temperature control, and accurate documentation.
With the timeline set for 2027, businesses now have a clear window to review their processes, identify any gaps, and ensure they are ready to meet these evolving requirements.
How can your site prepare for this upcoming change in legislation?
Playing catch up is never a good idea, especially when it comes to matters of compliance. Instead, it is best to prepare for any upcoming changes to legislation before the relevant deadline arrives.
With this in mind, we have listed five solutions that will help you to get ready for 2027 and ensure your site is aligned with EU standards.
1. Make Hygiene a Priority
Regulation (EC) No 852/2004 is expected to fall within the scope of the new SPS agreement. This regulation covers all stages of food production and requires businesses to maintain high standards of cleanliness, train staff effectively, and implement systems such as HACCP to identify and control food safety risks.

Ensure cleaning schedules are consistently followed, staff are fully trained, and any hazard controls are up to date and well documented. This is also a good opportunity to standardise procedures across different production areas.
Klipspringer supports businesses in maintaining robust hygiene standards. From colour-coded cleaning systems to visual management tools, we can help you ensure that your site meets regulatory requirements and is audit ready. You can explore our hygiene solutions and guidance via the online portal or speak with our team for tailored advice.
2. Temperature Control and Monitoring

Temperature control is another fundamental part of food safety and is likely to come under increased scrutiny.
If you are looking to strengthen accuracy and compliance in this area, you could benefit from introducing in-process data loggers for continuous, real-time monitoring of products and processes.
A site-wide Real-time Wireless Monitoring System can also be used to track key parameters such as temperature, humidity, and door contact, sending automatic alerts if a breach occurs.
3. Assess your Food Contact Materials
Regulation (EC) No 1935/2004, is expected to fall within the scope of the new SPS agreement. This regulation requires that any materials or equipment intended to come into contact with food do not transfer substances that could endanger human health or compromise food safety. This includes items such as utensils, containers, and production equipment.

Review the materials currently in use across your site and confirm that they are suitable for their intended purpose and supported by appropriate documentation. This may also be a good opportunity to replace worn or non-compliant items and standardise equipment across different areas of production.
Klipspringer specialises in food-contact approved materials. If you have any questions about whether your current equipment meets the required standards, our team will be happy to help. You can also view certification details across our product range via the online portal.
4. Plan for Increased Production Demand

The SPS agreement is expected to increase trade with the EU, which could lead to higher product demand. This could place greater pressure on your storage, handling, processing systems, and hygiene controls.
Consider whether additional equipment, colour-coded storage, or temporary segregation solutions could help maintain efficiency and compliance during busier periods.
This is also a good opportunity to review staffing, workflows, and seasonal planning to ensure your team can meet demand without compromising food safety or compliance.
5. Traceability and Documentation

Clear and accurate records will be essential for demonstrating compliance under the new SPS agreement.
Review how ingredients, materials, and finished products are tracked through your site, ensuring that information is easy to access and consistently recorded. The more thorough your records are at this stage, the easier it will be to meet any new expectations.
Strong documentation will not only support compliance with EU aligned standards but also help your business respond quickly and effectively in the event of an audit or recall.
At Klipspringer, we are closely following developments around the new SPS agreement to ensure we can provide the right products, systems, and support to help your business stay compliant.
If you have any questions about the guidance in this article, or want to explore how our food safety solutions can support your site through these changes, our team is here to help.
You can contact us directly on 01473461800 or sales@klipspringer.com. Alternatively, you can fill out the contact form below and one of our friendly team members will be in touch.
If you would like further guidance relating to the solutions included in this article, the Klipspringer team would be happy to help. Share your details below and we will be in touch.

SenseAnywhere vs WatchmanOne: Key Features and Differences of Real-Time Monitoring Systems
Exploring the Key Features and Differences of the SenseAnywhere and WatchmanOne Real-Time Monitoring Systems


Key Differences
1. Connectivity & Infrastructure
| SenseAnywhere | WatchmanOne |
|---|---|
|
|
2. Sensors, Battery Life & Power
| SenseAnywhere | WatchmanOne |
|---|---|
|
|
3. Cost Summary
|
SenseAnywhere (6 sensors) |
WatchmanOne (6 sensors) |
WatchmanOne (8 sensors) |
|
|---|---|---|---|
| Includes |
|
|
|
| Costs |
|
|
Note: This option effectively gives two extra sensors at ~50% of the normal price |
Comparison Table – Overview
| Feature | SenseAnywhere (6 sensors) |
WatchmanOne (6 sensors) |
|---|---|---|
| Battery | Up to 10 years, non-replaceable | 3–5 years, replaceable |
| On-site Display | ❌ None | ✅ Base station screen |
| Audible Alarm | ❌ No | ✅ Yes (at base station) |
| Cloud Platform | ✅ Included (default) | ✅ Included (via My Data Portal) |
| Annual Cost | £147.18 (£24.53 per sensor) | £56.63 (per base station, typically one per site) |
| SMS Cost | £0.61 each | £0.10 each |
| Initial Cost (Comparable 6 sensors) | £1,895.56 | £2,137.70 |
| Key Features |
|
|
If you have any questions about the SenseAnywhere or WatchmanOne Real-time Monitoring Systems, share your details below and we will be in touch.

Audit Countdown: What to Prioritise One Month, One Week and One Day Before an Audit
Introducing our Official Audit Countdown Guide: Stay organised, reduce pressure, and approach inspections with confidence.
Equipment and Storage
Throughout the Year

One Month Before or Whenever Your Audit Is Announced
One Week Before
Preparing for an audit and need last-minute support?
Whether you're replacing equipment, organising documentation, or resolving final issues, our team can help you stay audit-ready with practical solutions and fast turnaround.
- Same-day despatch on a wide range of equipment
- UKAS calibration, service, and repair with fast turnaround
- Online portal to access certificates and order history


One Day Before
Internal Audits
Throughout the Year

One Month Before or Whenever Your Audit Is Announced
One Week Before


One Day Before
Employee Engagement and Training
Throughout the Year

One Month Before or Whenever Your Audit Is Announced
One Week Before

One Day Before
Calibration and Documentation
Throughout the Year

One Month Before or Whenever Your Audit Is Announced
One Week Before

One Day Before
Preparing for an audit? Share your details below and our team will help you get everything in place.

ATP Testing: Why a ‘Zero’ Result Doesn’t Always Mean Clean
Discover why ATP Zero Readings are often misleading, what auditors think about them, and how the A3 System addresses this issue.
| Standard ATP Test | The A3 System |
|---|---|
|
|
Can you rely on your ATP results?
If zero readings are accepted as a pass, there is a risk that contamination is being missed. The A3 System removes this uncertainty by ensuring every valid test produces a measurable result.
- Detects ATP, ADP, and AMP for more reliable results
- Reduces the risk of false negatives caused by cleaning chemicals
- Ensures zero readings clearly indicate a testing issue
2. ATP Degradation
| Standard ATP Test | The A3 System |
|---|---|
|
|
3. Faulty Swabs or Poor Sampling Technique
| Standard ATP Test | The A3 System |
|---|---|
|
|
“We recommend using the A3 System, which provides
increased confidence in your results and reduces the
risk of misleading false negatives.”
Ed Campion, Hygiene Transformation Project Manager, Weetabix
Why Is It Important to Investigate Zero Readings?

How Do You Investigate a Zero Reading Produced by the A3 System?

1. Repeat the test on the same area
2. Test an alternative area
3. Check the swab and reagent
4. Assess the instrument
NOTE: Even unused swabs that haven’t been exposed to a sample should show a value of 2-3 RLU.
By recognising the limitations of standard ATP testing, sites can reduce the risk of false negatives and make more informed decisions about hygiene verification.
The comparison table below highlights the key differences between standard ATP tests and the A3 System in relation to zero readings.
| Standard ATP Test | The A3 System |
|---|---|
|
✗ Enzyme reaction is inhibited by a wide range of cleaning chemicals ✗ Unable to identify degraded molecules such as ADP and AMP ✗ Zero readings could indicate a clean surface or an issue with the testing process |
✓ Reduced risk of chemical interference affecting results ✓ Detects ATP, ADP, and AMP ✓ Detects ADP and AMP after common processes like heating, cooking, and cleaning ✓ Detects ADP and AMP in food residues that contain little or no ATP ✓ When a surface is truly clean, produces low baseline readings (often 1–8 RLU) that sit comfortably below site benchmarks ✓ Zero results are ALWAYS wrong and clearly indicate the need for investigation |
If you have any questions about zero readings or the A3 System, you can contact our team on 01473461800 or sales@klipspringer.com. Alternatively, you can fill out the contact form below.
Want more reliable hygiene verification? Share your details below and we’ll show you how the A3 System can help.

WEBINAR: Beyond Compliance: Leveraging Real-Time Monitoring for Meaningful Insights
WEBINAR: Beyond Compliance - Leveraging Real-Time Monitoring for Meaningful Insights
Real-time monitoring improves traceability, reduces manual checks, and triggers alerts when something goes wrong. But if you’re only using it for compliance, you’re missing a lot of potential value. Many sites already collect data on key parameters like temperature, CO₂, door activity, and energy use. The question is whether that data is being used to improve operational performance. In this webinar, we explored how real-time monitoring can:
- Drive intelligent business decisions beyond audits
- Reduce costs and boost sustainability
- Maximise efficiency across your entire operation
Stuart Warren, Senior Food Safety Manager at Coca-Cola EuroPacific Partners, also shared how Coca-Cola was using AI and real-time data to stay ahead. Attendees learned why analysing every datapoint matters, where AI could add real value, and what food businesses need to do to stay competitive in the years ahead.

Webinar Speakers
Alex Carlyon
Key Account Director,
Klipspringer
Radek Tameczka
Real-Time Monitoring Specialist,
Klipspringer

Stuart Warren
Senior Food Safety Manager,
Coca-Cola EuroPacific Partners
Key Webinar Areas

1. Why Real-Time Monitoring Matters in Modern Food Safety

2. Meeting BRCGS Monitoring Requirements with Confidence

3. Turning Monitoring Data into Business Intelligence

4. Driving Business Impact with AI, Digital, and Emerging Technology

5. Q&A Session with our panel of experts
The WatchmanOne Real-Time Monitoring System
The next generation of Real-Time Wireless Monitoring, trusted by industry leaders across the UK and Ireland.
- Instant alarm notifications if parameters are breached.
- Automated reporting for easy analysis.
- Versatile system with up to 150 sensors.
- No surprise costs or ongoing fees.
- Data is fully secure and belongs to your business.
If you have a question about Real-Time Monitoring, share your details below...

Choosing the Right Allergen Tests for Your Food Factory Application
Discover the benefits, limitations, and industry applications of our Lateral Flow Immunoassays and ELISA Allergen Test Kits.
Effective allergen testing is an essential part of food manufacturing. It helps sites to prevent cross contamination, support cleaning validation, meet strict regulatory requirements, and ultimately protect consumers with food allergies.
With several different testing methods available, choosing the right option for your site and application can sometimes be challenging. So, in the following article, we’ll take a closer look at the three key types of allergen testing solutions supplied by Klipspringer:
Quick Comparison Table
Not sure which allergen test is right for your application?
Our range of allergen test kits is designed to support every stage of your allergen control programme.
- Allergen Test Kits EASY for rapid surface and rinse water verification
- Allergen Test Kits PRO for testing allergens in food products and complex matrices
- ELISA Allergen Test Kits for high-sensitivity quantitative laboratory analysis
Why choose an Allergen Test Kit EASY?
Best for: Detecting allergenic protein residues on surfaces and in rinse water samples.
Allergen Test Kits EASY are a popular choice when speed and simplicity matter.
They provide incredible accuracy, with performance that can be up to ten times more accurate than many other LFIs on the market.
Despite this enhanced sensitivity, they remain very simple to use. Time consuming preparation steps common with other lateral flow tests have been eliminated, delivering results in just two steps and a total testing time of 10 minutes.
Storage is simple too. The kits can be kept at temperatures between 2 and 30°C, so refrigeration is not required. Under these conditions, the tests have a shelf life of approx 6-12 months.
Key Features
- Simple, two-part swab and shake process with a 10-minute test time.
- Accurate detection rate of 0.5ppm for rinse water samples and 4/5ppm for surfaces.
- No refrigerator required for storage.
- In stock for same-day despatch.

Ideal Applications in the Food Industry
Allergen Test Kits EASY are frequently used by hygiene teams to confirm that allergenic protein residue has been removed or reduced to a safe level on surfaces or in rinse water samples. These checks typically take place before a production line is released to ensure the risk of cross contamination is minimised.
These LFIs are particularly valuable during cleaning validation and routine hygiene verification, giving teams rapid confirmation that allergen controls are working as intended. With results available in around 10 minutes, corrective action can be taken immediately if residue is detected, helping to prevent costly production delays or product holds.
The simplicity of the test also makes it well suited to busy manufacturing environments. Staff can carry out testing directly on the factory floor without complex preparation or specialist laboratory equipment, making it easier to build allergen verification into everyday hygiene procedures.
Popular Applications
- Verifying cleaning effectiveness after allergen changeovers.
- Confirming equipment and food contact surfaces are free from allergen residue before production starts.
- Testing rinse water following cleaning procedures.
- Supporting cleaning validation studies during process development or audits.
- Routine hygiene verification as part of allergen management programmes.
- Investigating potential cross contamination events.
- Verifying sanitation of utensils, tools, and equipment.
- Environmental swabbing in areas where allergen control is critical.
Available Test Kits

Key Considerations
While Allergen Test Kits EASY are ideal for rapid surface and rinse water testing, they may not be the best option for every application.
For example, they are not suitable for testing finished food products or complex food matrices. In these cases, methods designed specifically for food samples, such as PRO Test Kits, are more appropriate.
EASY tests also do not offer the level of sensitivity required for very low level allergen detection or quantitative analysis. For these applications, laboratory based methods such as ELISA tests are the preferred option.
Why choose an Allergen Test Kit PRO?
Best for: Detecting target allergens in food products, even highly processed food.
Allergen Test Kits PRO use highly specific antibodies to detect target allergens in food products. The novel extraction solution provided in each kit enhances the extraction recovery yield to ensure accurate results, even when testing highly processed food.
These LFIs provide qualitative positive or negative results, making it easy to interpret allergen presence without requiring specialist equipment or training.
- Accurate allergen detection, even in highly processed and heated foods.
- Easier to use and less expensive than ELISA tests.
- Includes ready-to-use Extraction Solution.
- Minimises risk of false negatives due to unique Extraction Solution.
- No additional Buffer Solution required for testing.
- Limit of Detection: 5ppm.

Ideal Applications in the Food Industry
Allergen Test Kits PRO are used by sites that need accurate and reliable detection of allergens in both unprocessed and highly processed foods.
They are particularly valuable for verifying raw materials, monitoring production lines, and confirming that cleaning and production controls are effective in preventing cross contamination.
With fast results and minimal preparation, PRO kits allow teams to take immediate action if allergen presence is detected, helping to maintain food safety and regulatory compliance.
The simplicity and reliability of these kits make them suitable for use across a wide range of food matrices, from bakery products and sauces to ready-to-eat meals and confectionery.
Popular Applications
- Verifying raw materials for allergen presence before use in production.
- Monitoring production lines to prevent cross contamination.
- Confirming the effectiveness of cleaning and sanitation procedures.
- Supporting changeover validation between allergen-containing products.
- Routine allergen checks as part of a food safety management programme.
- Testing complex or highly processed food matrices where extraction is required.
- Investigating potential allergen incidents or complaints.

Key Considerations
The kits within this range can also be used for surface and rinse water samples. However, for these applications, we recommend using EASY Rapid Allergen Test Kits, which are designed specifically for fast and simple environmental verification.
Similarly, for highly sensitive, quantitative analysis, laboratory based ELISA tests are the more appropriate choice.
Why choose an ELISA Allergen Test Kit?
Best for: Highly sensitive detection of allergens in raw materials and processed foods
- Detects allergen proteins in raw, highly processed, and heat-treated foods.
- High sensitivity with a limit of detection (LOD) of 0.31 ppm.
- Highly specific antibodies for accurate allergen identification.
- Innovative extraction solution enabling detection of both native and denatured proteins.
- Easy-to-use protocol suitable for diverse food matrices.
- Reliable, quantitative results across a wide range of applications.

Ideal Applications in the Food Industry
ELISA test kits are designed for laboratory use where accurate, quantitative allergen testing is required. They are commonly used to verify raw materials, support routine quality control, and monitor production environments for potential allergen contamination. By providing precise and reliable results, they help laboratories assess allergen levels and support compliance with regulatory labelling requirements.
ELISA testing is also widely used during annual process and product validations to demonstrate that allergen control measures remain effective. It plays an important role in cleaning validation and allergen verification, helping confirm that sanitation procedures have successfully removed allergen residues, particularly when quantitative evidence is required for audits or investigations.
In addition, ELISA tests are used during new product development, recipe changes, or process modifications to verify that allergen cross-contamination risks are controlled. They also support root-cause analysis when unexpected allergen contamination occurs, and can be used to verify supplier compliance by testing incoming ingredients to confirm declared allergen status.
- Quantitative determination of target allergens in raw and processed foods.
- Verification of raw materials before use in production.
- Routine quality control testing in laboratory environments.
- Monitoring production lines for allergen contamination through sample testing.
- Supporting allergen labelling compliance and regulatory documentation.
ELISA tests are commonly used as the reference standard when validating rapid allergen detection tests such as lateral flow tests (LFTs). During validation, ELISA testing is used to establish the quantitative baseline, including key performance parameters such as limits of detection (LOD) and limits of quantification (LOQ). Results from LFTs are then compared against the ELISA data to confirm that the rapid method is suitable for routine allergen screening.
ELISA can also be used for method verification. In these cases, facilities may carry out parallel testing using both LFTs and ELISA methods to demonstrate that the rapid test consistently detects allergen residues at the required level and performs reliably within their specific production environment.
Key Considerations
ELISA test kits provide high sensitivity and can detect both native and denatured proteins across a wide range of food matrices.
They are not intended for rapid surface or rinse water testing in production areas. For quick environmental checks, Allergen Test Kits EASY are a more suitable choice.
Similarly, Allergen Test Kits PRO are the preferred choice for the quick screening of food products that do not require such high sensitivity levels.
That brings us to the end of our guide to choosing the right allergen tests for your food factory application, covering Allergen Test Kits EASY, Allergen Test Kits PRO, and ELISA Allergen Test Kits.
If you have any questions about pH measurement, you can contact our team of technical experts on 01473 461 800 or sales@klipspringer.com. Alternatively, fill out the contact form below.
Share your details below to discuss the right allergen test kit for your application.

High-Level Cleaning in Food Factories: Challenges & Solutions
Explore the challenges of high-level cleaning in food factories, plus the high-reach tools that improve safety, control, and hygiene.
High-Level Cleaning in Food Factories:
Five Common Challenges

Condensation and Listeria Risk
Need help improving high-level cleaning in your factory?
We can help you reduce contamination risks, improve access to overhead areas, and recommend practical tools for safer, more effective cleaning.
- Guidance on high-reach cleaning tools
- Advice on condensation and contamination risk
- Support aligned with hygiene and audit expectations
High-Reach Cleaning Solutions
From flexible brushes that bend around pipes to squeegee systems that control moisture collection, the right tools will make high-level cleaning safer, faster, and more effective.
Telescopic Equipment Handles
Telescopic handles allow hygiene teams to reach ceilings, pipework, and other overhead surfaces without unnecessary strain. Extending reach improves control at height and helps ensure all areas are thoroughly cleaned.

Klipspringer Telescopic Handles
Klipspringer telescopic handles offer the following features:
- A wide range of lengths, from two-stage to nine-stage models, reaching up to 9.5 m
- Aluminium options for strength or fibreglass for lightweight handling
- Twist-and-lock mechanisms to keep handle sections securely in place
- Water-fed variants with quick-coupling connections for rinsing overhead surfaces
- Colour-coded designs (up to 10 distinct colours) to support segregation and prevent incorrect use across different zones and applications
High-Reach Brushes
Flexible high-reach brushes bend to match the contours of surfaces, making them ideal for wrapping around pipework and reaching awkward or hidden areas.

Klipspringer High-Reach Brushes
Klipspringer high-reach brushes offer the following features:
- Colour-coded options to support segregation and prevent cross-contamination
- Manufactured using food contact approved materials, suitable for food production environments
- A variety of sizes to suit small or large pipes and surfaces
- Compatible with the complete range of Klipspringer handles
- High temperature tolerance, up to 134 °C
T-Bars and Dusters
High-level dusting and T-bar tools make cleaning overhead surfaces faster and easier. Their long reach gives hygiene teams effortless access to high-reach areas, and their flat design provides broad coverage, efficiently removing dust and debris without spreading it.
Klipspringer High-Reach Dusters & T-Bars
Klipspringer high-reach cleaning tools offer:
- Flat or bendable designs for thorough cleaning of narrow gaps, pipes, and ledges
- Replacement sleeves for improved hygiene and cost-effective ongoing use
- Compatible with Klipspringer telescopic handles for integrated high-level cleaning
High-Reach Condensation Squeegees
Condensation squeegees remove water from walls and ceilings, collecting moisture on the supple rubber blade so it can be removed safely, rather than dripping onto production surfaces below. This helps hygiene teams reduce contamination risks and maintain a consistently clean environment.

Klipspringer High-Reach Condensation Squeegees
Klipspringer high-reach condensation squeegees offer the following benefits:
- One-piece design for increased hygiene and easy cleaning
- Supple rubber blade that removes and contains moisture effectively
- Crevice-free interior to prevent dirt or bacteria buildup
- Compatible with water-fed handles, reaching up to 9.5 m for elevated or hard-to-reach surfaces
- Available in 10 distinct colours to support segregation and prevent cross-contamination
High-Reach Cleaning Verification
High-reach cleaning verification enables hygiene teams to confirm that overhead surfaces have been cleaned effectively. By extending verification to ceilings, tanks, and pipework, sites can maintain higher standards of hygiene control and reduce the risk of undetected contamination.

The A3 System and Swab Holder
When combined with a high-reach swab holder, the A3 System offers the following advantages:
- Detects all forms of organic residue for comprehensive hygiene verification
- Eliminates the need for ladders, improving health and safety
- Reduces the need for multiple access tools, supporting cost efficiency
- Compatible with all Klipspringer threaded handles for seamless integration
By combining effective procedures with purpose-built equipment, sites can reduce contamination risks and maintain stronger control over high-level hygiene.
If you have any questions about the products or solutions mentioned throughout this article, you can contact us on 01473461800 or sales@klipspringer.com. Alternatively, you can fill out the contact form below and we will be in touch.
Not sure if your current high-level cleaning process is compliant or effective? We can review your setup and recommend the right tools for your site.

Future Trends of The Food Production Industry
The industry is entering a period of rapid change, driven by new technologies, emerging ingredients, and evolving risks.
The Role of Artificial Intelligence
Customers and auditing bodies may begin to move away from periodic inspections towards more continuous forms of oversight. Rather than assessing a site once or twice a year, smart systems could maintain a constant digital view of activity across the factory floor, highlighting trends and risks in real time.
AI may not just be used to generate data. Its real value could lie in translating complex information into clear, practical guidance. Instead of technical alerts or lengthy reports, future systems could automatically recommend actionable next steps, helping teams respond quickly and confidently.

Cameras and image-recognition tools have the potential to play a much larger role in future factories, scanning production lines to flag unsafe practices or subtle issues that are easy to miss in a fast-moving environment. Small sensors could also monitor key parameters, identifying unusual patterns before they escalate into compliance failures.
Food production sites may experiment with systems that respond automatically when risks are detected, making minor adjustments before problems have the chance to escalate. Digital twins (virtual versions of real production lines) could also be used to test process changes or explore “what if?” scenarios without disrupting day-to-day operations.
The Popularity of New Protein Sources
Insects and other novel proteins are rising in popularity as alternative sources of nutrition. However, allergen data remains limited in some areas. To account for this, factories will need to review existing allergen management systems, adapt risk assessment tools, and closely monitor regulatory developments.
Emerging protein sources could require a revised approach to supplier approval, particularly if raw materials are sourced from unfamiliar regions or new partners. This may also apply where new farming methods and production processes introduce additional risk factors to the supply chain.

Alternative proteins may behave differently to traditional animal or plant-based ingredients during processes such as mixing, heating, or extrusion. As a result, sites may need to refine equipment settings and processing parameters to maintain product quality and consistency.
When it comes to building trust in alternative proteins, communication with consumers will become increasingly important. Manufacturers are likely to face evolving expectations around ingredient origin, sustainability claims, and nutritional information.
Social Media and Food-Related Apps
A single social media post can reach a wide audience within seconds. While this can strengthen brand visibility, it can also amplify complaints or misinformation. As new platforms continue to emerge, manufacturers will need robust crisis response strategies to manage reputational risk effectively.
A growing number of apps allow consumers to scan products for nutritional information and ingredient details, supporting healthier choices and allergen awareness. Increased visibility of product data may strengthen transparency, but it could also intensify scrutiny of recipes, ingredient lists, and labelling accuracy.

As social media plays a greater role in shaping consumer understanding, the risk of misinformation around food safety and nutrition is likely to grow. Short-form recipe videos and product reviews often prioritise visual impact over clear guidance, sometimes overlooking fundamental food safety practices.
Digital platforms provide new opportunities to engage consumers on topics such as food safety, sustainability, and allergen awareness. Forward-thinking manufacturers may allocate resources to developing and monitoring content that supports brand reputation while aligning with regulatory expectations.
Increased Risk to Supply Chains
In the UK, theft and fraud costs in supply chains rose from £68 million in 2023 to £111 million in 2024, driven by organised crime and insider threats. If this trend continues, sites will need to strengthen internal controls, verification procedures, and monitoring systems to minimise the risk of financial loss.
Animal disease remains a persistent threat to supply chain stability. In the future, AI and other emerging technologies could enhance resilience through predictive forecasting, improved traceability, and earlier intervention. Faster detection and response times may help to limit recalls and reputational damage.

The UK’s National Cyber Security Centre has underscored the growing threat posed by state-sponsored cyberattacks and increasingly sophisticated criminal activity. As food factories become more reliant on technology, cybersecurity will need to sit alongside food safety as a core operational priority.
Rising concerns over allergen contamination of raw ingredients demand more rigorous testing, enhanced data transparency, and stricter supply chain audits. As consumer expectations increase and regulation evolves, predictive AI tools could help sites to identify emerging risks and take preventative action.
As the industry’s trusted partner in food safety compliance, we are committed to helping you navigate emerging challenges, strengthen compliance, and ensure resilience across your operation.
To discuss how our products and solutions can support your site, whether in preparation for upcoming audits or future developments, call 01473 461 800 or email sales@klipspringer.com. You can also share your details via the contact form below and a member of our team will be in touch.
If you would like to discuss the future planning of your food factory, please share your contact information below.

EU Listeria Rules: New Shelf-Life Requirements for Ready-to-Eat Foods
Listeria monocytogenes is facing increased scrutiny as new EU rules reshape how
ready-to-eat foods are assessed for safety.
The European Commission has published Regulation (EU) 2024/2895, introducing tougher controls for ready-to-eat foods.
From July 2026, businesses will need robust scientific evidence to prove their products remain safe throughout their entire shelf life, marking a significant shift in compliance expectations.

Why is Listeria Under Increased Scrutiny?
Listeria differs from many other foodborne bacteria.
- It survives in aerobic & anaerobic conditions.
- It can grow at refrigeration temperatures.
The second point is particularly significant, as it means that where a product supports growth, listeria levels can increase during chilled storage. This could be in a depot, retail environment, or a consumer’s home.
A Change in EU Regulations
For ready-to-eat foods that support the growth of Listeria monocytogenes, businesses typically demonstrate “absence in 25g” at the point of production. After this stage, many rely on the ≤ 100 cfu/g limit to remain compliant during shelf life. Historical data and finished product testing are often used to support this approach.
From July 2026, “absence in 25g” will become the default requirement for the entire shelf life of products that support growth. The 100 cfu/g limit will only be permitted where a business can scientifically demonstrate that this level will not be exceeded at any point before the end date.
If growth cannot be ruled out through robust evidence, “absence in 25g” will need to be maintained throughout shelf life.
What Does This Mean for the UK?
Great Britain
Following Brexit, new EU rules do not automatically apply in England, Scotland, or Wales. If you only supply the domestic GB market, you are not currently legally bound by the July 2026 update.
The Food Standards Agency has not confirmed that these changes will be formally adopted into GB law. However, the UK often aligns with EU food safety standards, so it is wise to stay informed and plan ahead.
Exporting to the EU
If your site exports ready-to-eat foods to the EU or Northern Ireland, you must comply with the EU regulations. This is because authorities will assess your products against EU law, regardless of where they were made.
For many UK manufacturers, this makes preparation unavoidable. Even if your primary market is Great Britain, planning now will reduce risk and ensure compliance if your products cross borders.
Northern Ireland
Northern Ireland operates under the Windsor Framework, which keeps certain EU food safety laws in place. The new Listeria rules will apply from 1 July 2026.
Which Products Will This Change Affect?
The stricter requirements primarily focus on chilled ready-to-eat foods that can support the growth of Listeria monocytogenes. These include:
- Cooked sliced meats and pâtés
- Cold-smoked fish
- Soft cheeses
- Prepared salads
- Sandwiches and other chilled foods with multiple components
If a product is eaten without further cooking and does not have strong intrinsic barriers, such as low pH or low water activity, it is likely to fall into this category. Where growth cannot be confidently ruled out, regulators will assume it can occur. This means the default expectation will be “absence in 25g” throughout the shelf life.

Practical Steps to Consider
If you produce chilled ready-to-eat foods, practical next steps include:
- Assess whether your shelf-life evidence is strong enough
- Strengthen environmental monitoring in higher-risk areas
- Clarify responsibilities across the supply chain
- Train teams and ensure all actions are fully documented
A proactive, science-based approach will help protect consumers, maintain compliance, and demonstrate safety right through to the end of shelf life.
A Note on Environmental Monitoring

Even though demonstrating absence at the point of production is no longer enough on its own, listeria control during production is still a critical step in reducing contamination risk and maintaining good hygiene practices.
Klipspringer Listeria Isolation Swabs can help with this. They have been developed to support applications such as checking food contact surfaces, validating cleaning procedures, and identifying potential contamination points.
Quick and easy to use, these tests support a proactive hygiene strategy and help teams act swiftly if Listeria is detected.
Listeria control is no longer just about passing the right tests at the point of production. For UK businesses supplying Northern Ireland or exporting to the EU, you need to demonstrate safety throughout shelf life.
To find out more about upcoming regulatory changes or our Listeria Environmental Monitoring Tests, contact us on 01473 461800 or sales@klipspringer.com. Alternatively, use the form below to share your details.
If you would like further information relating to compliance in this area, the Klipspringer team would be happy to help. Share your details below.

HSE Bakery Inspections Underway Across the UK
Since January 2026, the Health and Safety Executive (HSE) has carried out a series of inspections at large bakeries across the UK.
HSE Inspectors are checking that employers are effectively protecting workers from exposure to dusty ingredients, including flour, bread improver enzymes, and other powdered materials.
The inspections focus on whether bakeries are following the guidance outlined in the Control of Substances Hazardous to Health (COSHH) regulations. This means assessing if workplaces are:
- Eliminating dusty processes where possible
- Substituting lower-dust alternatives
- Using engineering controls, such as local exhaust ventilation
- Relying on respiratory protective equipment only as a last resort
HSE inspectors are also reviewing health surveillance programmes to ensure that employees exposed to dusty ingredients are being monitored appropriately.
“I urge employers to carefully consider dusty processes, eliminating risk and substituting to prevent exposure.”
— Mike Calcutt, Deputy Director, HSE’s Engagement and Policy Division
The Health Risks of Dust Exposure
Dusty ingredients in bakeries pose a serious health risk to workers. Flour dust, in particular, is a common cause of occupational asthma in the UK, while other powdered ingredients can also trigger respiratory sensitisation.
Repeated exposure to dust can make the airways hypersensitive. Once a worker becomes sensitised, even small amounts of dust can provoke symptoms such as coughing, wheezing, chest tightness, and shortness of breath. In many cases, these conditions are irreversible.
High-risk tasks include:
- Dusting flour during dough handling
- Tipping, dispensing, or weighing dry ingredients
- Cleaning up flour or powdered ingredient spills
Unchecked dust can linger in the air, increasing the likelihood of long-term respiratory issues. Protecting your workforce requires a combination of process controls, effective cleaning, and ongoing health surveillance.

Solutions for Managing Dust in Bakeries
Industrial Vacuums: Safe, Efficient Dust Control
Effectively controlling dust not only protects your workforce but also improves cleanliness, productivity, and compliance with HSE regulations. While a combination of measures is important, one of the most practical and effective solutions is the use of specialist industrial vacuums.
A number of the Industrial Vacuums within the Klipspringer range have been specifically designed for dry, powdered ingredients like flour, spices, and bread improver enzymes.

There are also ATEX options certified for Zones 21 and 22. They provide a safe, reliable solution for managing dust in ATEX areas. Key features include:
- Brushless motor for long service life. Turbine motors are also available.
- Filtered air system for motor cooling and exhaust – different filtering systems to supress dust contamination.
- AISI 304 stainless steel construction for filter chamber, tank, and cover.
- Star filter available in multiple media options e.g. HEPA filters and M Class (as standard).
- Most models feature a tangential inlet and integrated manual filter cleaning. However, some ATEX options feature a central inlet.
- Available in multiple power options: 400 V three-phase, 240v, or 110v.
- Different collection options available for the secure containment of dust, including the Longopac options.
This vacuum effectively removes dust without stirring it into the air. It is compatible with a wide range of ATEX-approved attachments that ensure every cleaning task, from factory floors to hard-to-reach areas, can be handled safely.

Supporting Measures for Dust Control
While Industrial Vacuums form the cornerstone of dust management, we recommend complementing them with other control measures:

Effective Cleaning
Regularly remove dust using appropriate tools, avoiding methods that stir particles into the air.
Extra-soft brush bristles or hygienic double-blade squeegees could help you to maintain a safe environment, but only if they align with your site’s existing policies.

Personal Protective Equipment (PPE)
Ensure operatives understand the risks of dust exposure and wear correctly fitted protective equipment, such as masks and glasses, when necessary.
PPE should be used to supplement other control measures, not as the sole means of protection.

Training and Visual Management
Reinforce key safety messages with clear visual signage that highlights essential actions.
This includes using the right equipment, cleaning up spills immediately, maintaining a ‘clean-as-you-go’ approach, and wearing appropriate PPE.
NOTE: It is important that you weigh up the introduction of any new equipment against your site’s existing policies. You should also consider the expectations of your customers and relevant auditing body.
For a deeper dive into these measures, you can explore the following help guides:
Klipspringer can help you to protect your workforce and meet HSE expectations with an effective dust control strategy.
For more information or to discuss your site’s requirements, contact us on
01473 461800 or sales@klipspringer.com. Alternatively, use the form below to share your details.
If you would like further information relating to compliance in this area, the Klipspringer team would be happy to help. Share your details below.

Shadow Boards and Food Safety Audits: What Do Auditors Really Expect?
Explore the relationship between shadow board storage and audit compliance.
What Do Food Safety Standards Expect?
- Equipment and utensils are stored in a hygienic manner
- Cleaning tools are easily identifiable and colour-coded where required
- Cross-contamination risks are controlled during both use and storage
- Equipment is segregated by zone and application
- Cleaning and sanitation procedures are clearly defined and consistently followed
- Utensils are fit for purpose and replaced at the end of their lifespan

“Equipment that is not used or is taken out of service shall be cleaned and stored in a manner that does not pose a risk to the product.”
— BRCGS Global Food Safety Standard, Issue 9, Clause 4.6.5
How Do Shadow Boards Strengthen Audit Readiness?
Shadow boards offer a practical, highly visual way to demonstrate that audit expectations are being met. When implemented effectively, they enhance audit readiness across several key areas:
1. Clearly Designated Storage Locations
Auditors expect equipment to have a defined home and to be stored in a way that does not pose a risk to food safety.
Shadow boards meet this expectation by providing a fixed, clearly marked location for each item. Benefits include:
- Reducing the likelihood of tools being lost
- Making it immediately obvious when equipment is missing
- Supporting hygienic storage by keeping items off floors and work surfaces
- Establishing a best-practice standard that can be rolled out across the site

2. Colour-Coding and Segregation
Shadow boards strengthen colour-coding policies by clearly showing which tools belong in each area and highlighting their intended applications.
By visually linking equipment to defined zones, processes, or risk levels, they make best practice intuitive. This reduces misuse and promotes accountability.
The result is not just better organisation, but stronger risk management. For auditors, a well-designed shadow board provides immediate evidence that colour-coding rules are understood and are being applied consistently.

3. Hygienic Design
Food safety standards emphasise the importance of hygienic design.
Made from food-safe, water-resistant, and
easy-to-clean materials, shadow boards support this requirements by:
- Resisting moisture and washdown chemicals
- Eliminating potential harbourage points for bacteria or debris
- Reducing the risk of degradation over time
This aligns directly with the broader requirement that equipment storage systems must not introduce contamination risks.

4. Visual Management and Accountability
One of the greatest audit advantages of shadow boards is that they bring equipment into plain view. Rather than leaving tools out of sight, where they might go unnoticed until an auditor identifies a non-conformity, shadow boards make it immediately obvious if:
- A tool is missing
- An item is in the wrong location
- Equipment is damaged
- A utensil has been returned unclean
This supports internal audits and ongoing supervision, while also providing auditors with evidence that the correct controls are in place.

Do Shadow Boards Increase the Risk of Audit Non-Conformance?
Shadow boards bring equipment into plain view, making it immediately obvious if an item is missing, damaged, dirty, or stored incorrectly. While this visibility strengthens day-to-day control, some hygiene managers worry that it could expose them during an audit.
In practice, a missing tool is not automatically a non-conformance. The risk only arises where there is a lack of control. For example:
- A tool is missing with no clear explanation
- Equipment is not being stored in its designated place
- There is poor discipline around storage
- There is a risk of contamination or cross-contamination

If you can prove that a tool is temporarily absent because it is in use, being cleaned, or undergoing maintenance, auditors are likely to view this as part of a controlled system.
Remember, the requirement is control, visibility, and hygienic management. It’s not that every shadow on your board must be filled at every moment of the day.
In fact, bringing equipment into the open is a positive move for audit compliance. It demonstrates transparency, confidence in your processes, and a willingness to make controls visible rather than hidden. As for audit preparation, this level of visual management also makes equipment checks faster and more straightforward.
“Equipment stored in internal production and storage areas shall be kept clean.”
— BRCGS Global Food Safety Standard, Issue 9, Clause 4.6.5
Shadow Boards and Audit Compliance
Installing shadow boards is a strong first step toward improving organisation, hygiene control, and audit readiness. However, to unlock the full potential of this solution, your shadow boards should be thoughtfully integrated into your wider systems. For best results, ensure they are:
- Fully aligned with your colour-coding policy
- Referenced within Cleaning Instruction Cards
- Supported by ongoing cleaning procedures
- Included in internal audit checks
- Covered in staff training and onboarding
- Routinely inspected and well maintained

“Food contact equipment that has been stored but is not in daily use shall be cleaned and, where necessary, disinfected prior to use.”
— BRCGS Global Food Safety Standard, Issue 9, Clause 4.6.5
How to Assess Your Audit Readiness
If you are considering shadow boards as part of your compliance strategy, taking a structured approach will help to ensure they genuinely strengthen your audit position.
1. Review Your Audit Standard
Start by revisiting the specific clauses that relate to:
- Equipment storage
- Cleaning tools
- Segregation and cross-contamination control
- Hygienic design
Focus on understanding the intended outcome of these requirements. Auditors are typically looking for evidence of control, consistency, and risk reduction.

2. Conduct a Gap Analysis
Assess your current practices:
- Are tools ever left on work surfaces?
- Do utensils move between zones without clear control?
- Are items occasionally missing or unaccounted for?
- Is storage visually organised and easy to verify at a glance?
If gaps or inconsistencies exist, implementing a structured visual storage system is a great way to deliver a clear, measurable improvement.

3. Integrate Storage into Your Compliance System
To deliver real value, storage solutions should be embedded within your wider compliance framework. This means they are:
- Clearly documented within procedures
- Included in internal audit checks
- Routinely inspected and maintained
- Supported by appropriate staff training
When approached in this way, shadow boards become part of a controlled, auditable system that supports consistent performance.

Shadow boards and other named storage solutions may not be explicitly mentioned in major food safety standards, but the principles they support are.
Hygienic storage, equipment segregation, and cross-contamination controls are all mandatory requirements, and when properly implemented, shadow boards make these practices easy to demonstrate.
If you have any questions about shadow board storage solutions, you can contact us on 01473461800 or sales@klipspringer.com. Alternatively, you can fill out the contact form below.
To learn more about shadow board storage and audit compliance, share your details below.

Introducing the Hygienic Double Blade Squeegee: Practical Benefits for Food Factories
A first look at the Hygienic Double Blade Squeegee, plus the practical benefits it brings to on-site hygiene and efficiency.
Limited-time special introductory price – purchase online now
1. Ultra-Hygienic Design
Hygiene was a key focus in the development of the Hygienic Double Blade Squeegee. Its extra-smooth, moulded design features minimal crevices, which makes it easier to clean than traditional double blade models.
By reducing areas where residues and moisture can collect, the squeegee helps hygiene teams work more efficiently and maintain overall equipment cleanliness.

“All the team prefer it over other squeegees we’ve used.”
— Site Hygiene Manager, High Care Food Manufacturer
2. Push and Pull Functionality
The double blade design delivers reliable performance even on uneven surfaces, ensuring the Hygienic Double Blade Squeegee is suited to a variety of cleaning tasks.
It is designed for both push and pull operation, so liquids can be moved efficiently in either direction. This helps reduce cleaning time and supports more efficient workflows in busy food production environments.


3. Replaceable Cartridge
The replaceable cartridge system allows worn components to be swapped out easily while staying secure during operation, extending the squeegee’s lifespan and eliminating the cost of unnecessary replacements.
By replacing only the blade rather than the entire squeegee, sites can significantly reduce plastic use and lower their CO₂ footprint. Inventory management is also simplified, as storing slim replacement blades instead of full squeegees takes up much less space.

4. Durable Design
The Hygienic Double Blade Squeegee is designed to withstand the demands of food production environments, providing reliable, long-lasting performance.
Its robust design has been proven in trials with hygiene teams across the UK and Ireland, ensuring durability that’s truly tried and tested.

5. Colour-Coded for Segregation
The Hygienic Double Blade Squeegee is available in up to 11 colours, ready to support your site’s colour-coding and segregation policies.
Clear colour differentiation helps to prevent squeegees from being used in the wrong areas, reducing the risk of cross-contamination and ensuring compliance with audit requirements.

Comparison Table
| Single Blade Hygiene Squeegee |
Traditional Double Blade Squeegee |
Hygienic Double Blade Squeegee |
|
|---|---|---|---|
| Food contact approved | Yes | No | Yes |
| Hygienic design | 5/5 | 1/5 | 4/5 |
| Ease of cleaning | 5/5 | 0/5 | 4/5 |
| Bacteria harbourage resistance | 5/5 | 0/5 | 4/5 |
| Push | 1/5 | 5/5 | 5/5 |
| Pull | 5/5 | 5/5 | 5/5 |
| Number of components (excl. handle) | 1 | 3 | 2 |
| Performance (moving water) | 4/5 | 5/5 | 5/5 |
| Ease of movement | 4/5 | 5/5 | 5/5 |
| Speed of movement/efficiency | 3/5 | 4/5 | 5/5 |
| Replaceable cartridge | No | Yes | Yes |
| Size options | 300, 400, 500, 600, 700mm | 400, 600mm | 400, 600mm |
| Colour coding | 11 colours, fully colour coded | 8 colours, partially colour coded | 11 colours, fully colour coded |
| Sustainability | 1/5 | 3/5 | 4/5 |
| Scraper nose | Yes | No | No |
| Performance on smooth floor surfaces | 5/5 | 5/5 | 5/5 |
| Performance on uneven floor surfaces | 2/5 | 4/5 | 3/5 |
| Performance on anti-slip floor surfaces | 4/5 | 4/5 | 5/5 |


We hope this article has provided a helpful overview of the Hygienic Double Blade Squeegee, highlighting its design features and practical benefits for food production environments.
If you have any questions about this innovative squeegee design, you can contact us on 01473461800 or sales@klipspringer.com.
Alternatively, you can fill out the contact form below to arrange a trial.
To arrange a trial of the Hygienic Double Blade Squeegee, share your details below.

On-Site Histamine Checks: Food Safety & Compliance
On-site histamine checks are a critical first line of defence for food production sites.
1. Protecting Consumers from Histamine Poisoning
Histamine can trigger rapid and potentially severe reactions, including flushing, headaches, rashes, vomiting, and breathing difficulties. It is one of the most common causes of seafood-related food poisoning worldwide.
Histamine checks provide a quick and effective way to verify that histamine levels are not approaching dangerous thresholds. By identifying elevated levels early, sites can prevent unsafe products from entering the food chain, reducing the risk of consumer illness and product recalls.

2. Ensuring Compliance with Legal Limits
Many foods, particularly tuna, mackerel, anchovies, sardines, and other pelagic fish, are subject to strict histamine limits under UK and EU legislation. Histamine can also form in cheeses and fermented foods such as wine and sauerkraut.
Routine histamine testing supports compliance by providing documented evidence of control during audits and inspections. Rapid screening methods allow sites to demonstrate due diligence without delaying production.

3. Identifying Temperature Spoilage
Histamine forms when certain food products are exposed to incorrect temperatures. Elevated or borderline results can act as an early warning sign of:
- Breakdowns in the cold chain
- Increased microbial activity
- Poor handling practices or delayed chilling
Identifying these issues early enables food production sites to investigate root causes, take corrective action, and prevent repeated failures.

4. Rapid On-Site Screening
By reducing reliance on external laboratory testing for initial screening, sites can act fast to prevent potential incidents. Rapid, on-site histamine screening allows teams to identify batches that may require more precise quantitative testing before they move further through the production process.
This approach supports a wide range of quality assurance activities, including:
- Intake checks on incoming raw materials
- In-process quality control during production
- Verification of supplier performance
- Informed batch release decisions
By enabling faster decision-making without disrupting operations, on-site screening helps to maintain both food safety and operational efficiency.

Histamine Check Swabs – A Practical Screening Tool
Histamine Check Swabs provide a simple, rapid method for screening histamine in food samples using a colourimetric reaction.
The test is based on an enzyme-specific assay in which histamine dehydrogenase reacts with histamine to produce a purple formazan dye.
The intensity of the colour change is compared against a colour chart to give an approximate indication of histamine content.

Intended for on-site use, Histamine Check Swabs support quick decision-making where immediate screening is required. While the method is not intended for precise quantification or as an official analytical test, it offers a practical way to identify samples that require laboratory analysis.
Key Features and Benefits
Colour change indicating histamine content
Visual indication of a histamine reaction without instrumentation.
Enzyme-specific reaction
Designed to react specifically with histamine.
Fast results (approximately 5 minutes)
Rapid indication supports timely quality and safety decisions.
No instrumentation required
Can be carried out on site without analytical equipment.
Simple, easy-to-use method
Suitable for routine screening with minimal training.
Colour chart comparison
Provides an approximate understanding of histamine concentration.
Regulatory Requirements
In the UK, statutory histamine limits only apply to fish and certain fishery products. These limits are set out in Retained Regulation 2073/2005, which outlines both the criteria and the sampling schemes. Products that exceed these limits can be withdrawn or recalled, and local authorities may take enforcement action.
Testing must be conducted using validated laboratory methods. On-site rapid tests can serve as a screening tool but cannot replace accredited laboratory testing for compliance purposes.
Even when products meet the legal limits, businesses must remain vigilant. Histamine is heat-stable and is not destroyed by cooking, so controlling time and temperature at every stage is critical. Key measures include rapid chilling immediately after catch, maintaining cold chain integrity, and adhering to strict hygiene standards during handling and processing.
The table below summarises the histamine limits and sampling criteria set out in UK legislation for certain fish and fishery products. This information has been provided for general guidance only. Food businesses should always refer to the relevant legislation and seek appropriate technical advice to confirm their own compliance obligations.
| Product | Mean limit | Max limit | Sampling plan |
|---|---|---|---|
| Fish species naturally high in histidine, e.g. tuna, mackerel, sardines, anchovies, herring | ≤ 100 mg/kg | ≤ 200 mg/kg | n = 9 samples per batch |
| Fishery products that have undergone enzyme maturation in brine (where histamine may increase during processing) | ≤ 200 mg/kg | ≤ 400 mg/kg | n = 9 samples per batch |
| Fermented fish sauces | N/A | ≤ 400 mg/kg | n = 1 sample |
For other foods, UK regulations do not define explicit histamine limits. However, businesses are still responsible for managing the risk of histamine formation through robust food safety systems.
On-site histamine screening plays a vital role in protecting consumers, supporting regulatory compliance, and accelerating informed decision-making, making it a reliable safeguard wherever histamine risk is a concern.
For more information about Klipspringer Histamine Check Swabs, contact our technical team on 01473 461800 or email sales@klipspringer.com. You can also complete the contact form below and we’ll get back to you right away.
If you would like to learn more about Histamine Checks or Klipspringer Histamine Check Swabs, share your details below and we’ll get back to you right away.


 Shadow Boards & Equipment Storage
 Visual Management
 Hygiene & Production Equipment
 Food Handling & Storage Containers
 Instrumentation and Monitoring
 Calibration & Service
 Segregation & Washdown Covers
 Detectable Equipment
 Specialist PPE
 Stainless Steel Equipment
 Hygiene Squeegees
 Vacuum Cleaners
 Food Manufacturing
 Food Storage, Distribution & Retail
 Auditors & Food Safety Inspectors
 Food Service & Hospitality